
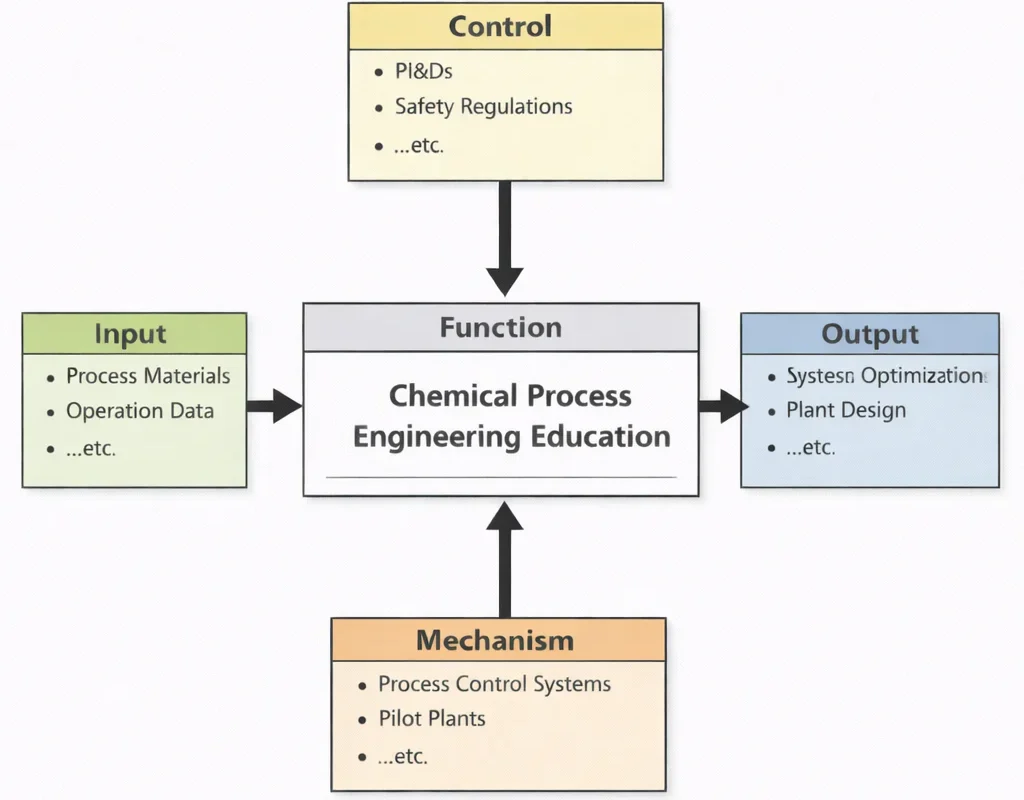
Chemical Process Engineering Education, viewed through this diagram, teaches students how to think in flows, constraints, and consequences. The Inputs anchor learning in what a plant actually handles—materials moving through units, and data that reveals pressures, temperatures, compositions, and performance under changing conditions. The Controls ensure that decisions are not improvised: P&IDs teach students to read the plant's "logic," while safety regulations enforce disciplined design limits and risk-aware operation. The Mechanisms give learners the power to act: control systems train them to stabilize and regulate processes, and pilot plants let them test ideas, observe dynamics, and learn from deviations without catastrophic cost. The Outputs are graduates who can design plants that work on paper and in reality, and who can optimize systems so they run efficiently, safely, and consistently—day after day, not only under ideal conditions.
Chemical Process Engineering plays a pivotal role in transforming raw materials into valuable products through efficient, scalable, and sustainable methods. It is deeply interconnected with the broader domain of Chemical Engineering, providing the systematic approaches necessary for designing, operating, and optimizing chemical plants. The integration of biological components into processes, as seen in Biochemical Engineering, has expanded its application into pharmaceuticals, food, and biofuels.
A comprehensive understanding of Chemical Catalysis and Reaction Engineering is essential, as most processes begin with molecular transformations. These often demand specialized materials, linking the discipline to Chemical Materials Engineering. Engineers also work closely with Chemical Energy Systems Engineering to ensure efficient energy usage, whether through combustion, electrochemical systems, or renewables.
Modern process design increasingly depends on Computational Chemical Engineering tools, enabling simulation, modeling, and real-time process control. Applications in consumer products and packaging highlight the relevance of Food and Beverage Engineering. Additionally, nanostructured catalysts and advanced process intensification methods are studied in Nanotechnology in Chemical Engineering.
In manufacturing polymers and composites, the principles of Polymer and Plastics Engineering are closely tied to process conditions such as temperature profiles, mixing regimes, and extrusion rates. These processes often take place in large facilities designed in collaboration with Civil Engineering professionals and managed through expertise in construction management.
Process engineers contribute to safety and resilience through knowledge drawn from Earthquake and Disaster Engineering and Geotechnical Engineering. Structural design of chemical plants is aligned with the practices of Structural Engineering, while logistics and facility layout are informed by Transportation Engineering and Urban and Regional Planning.
Processes involving separation, filtration, and treatment rely heavily on the principles used in Water Resources Engineering. Automation and control of operations are handled in collaboration with experts in Electrical and Electronic Engineering, particularly in subfields such as Biomedical Electronics and Communication Engineering.
The application of Control Systems Engineering ensures stability, safety, and efficiency in both batch and continuous operations. Instrumentation such as sensors, actuators, and automated valves are integral components that fall under Instrumentation and Measurement. Engineers also harness microcontrollers and embedded solutions from Embedded Systems and Microelectronics to enable smart processing platforms and digital twins.

A futuristic industrial facility fills the scene with tall distillation columns, pipes, valves, and interconnected processing units extending into the background. On the right, an engineer in a lab coat and hard hat holds a tablet, facing the plant as if supervising operations. Transparent holographic overlays appear across the foreground and midair: bar charts, trend lines, and interface panels suggesting production metrics, efficiency, and safety monitoring. Above the plant, symbolic icons such as molecules, equipment, and analysis tools reinforce the idea of integrated process design—where chemistry, equipment, control systems, and data analytics work together to convert raw materials into useful products at scale.
Chemical Engineering – Knowledge Map
Chemical Engineering – Overview
Establishes the overarching framework where individual operations are combined into coherent production systems.
Chemical Process Engineering
Focuses on designing and integrating unit operations to transform raw materials into finished products at scale.
Chemical Catalysis & Reaction Engineering
Supplies the core reaction steps that must be embedded and controlled within larger process flows.
Chemical Materials Engineering
Determines the properties of materials being produced and handled throughout the processing stages.
Chemical Energy Systems Engineering
Integrates energy supply, heat exchange, and efficiency considerations into process design and operation.
Polymer & Plastics Engineering
Requires carefully controlled processing conditions to shape molecular structure and final product properties.
Nanotechnology in Chemical Engineering
Introduces precision manufacturing steps that must be incorporated into scalable and stable production systems.
Biochemical Engineering
Adapts process design to accommodate biological reactions, including fermentation and cell-based production.
Food & Beverage Engineering
Applies process control to ensure consistent quality, safety, and scalability in consumable products.
Computational Chemical Engineering
Uses simulation to design, optimise, and troubleshoot complex process systems before physical implementation.
Core Areas of Chemical Process Engineering
Process Design and Development
- Definition: Designing chemical processes to convert raw materials into desired products.
- Key Components:
- Process Flow Diagrams (PFDs): Represent the overall structure of a chemical process.
- Piping and Instrumentation Diagrams (P&IDs): Detailed layouts of process equipment, piping, and instrumentation.
- Equipment Selection: Choosing suitable reactors, heat exchangers, distillation columns, and separators.
- Applications:
- Designing new chemical plants.
- Improving existing manufacturing processes.
Process Simulation and Modeling
- Definition: Using computational tools to simulate and analyze chemical processes before physical implementation.
- Tools:
- ASPEN Plus, HYSYS, CHEMCAD: Process modeling software for simulation.
- Computational Fluid Dynamics (CFD): Analyzes fluid flow, heat transfer, and chemical reactions within process units.
- Benefits:
- Optimizing process efficiency and reducing costs.
- Identifying bottlenecks and safety risks in the design phase.
Process Control and Automation
- Definition: Managing and regulating industrial chemical processes to ensure consistent, safe, and efficient operation.
- Control Strategies:
- Feedback Control: Adjusts processes based on output deviations.
- Feedforward Control: Anticipates changes and adjusts inputs accordingly.
- Advanced Process Control (APC): Incorporates real-time data and predictive models for optimization.
- Automation Tools:
- Distributed Control Systems (DCS).
- Supervisory Control and Data Acquisition (SCADA) systems.
Scale-Up and Pilot Plant Design
- Definition: Transitioning chemical processes from laboratory-scale experiments to full-scale industrial production.
- Steps in Scale-Up:
- Bench-Scale Testing: Small-scale experiments to validate process concepts.
- Pilot Plant: Intermediate-scale systems to test process feasibility.
- Commercial Scale: Full-scale production with optimized designs.
- Challenges:
- Maintaining product quality and process stability during scale-up.
- Managing heat and mass transfer issues at larger scales.
Heat and Mass Transfer
- Definition: Designing systems for efficient transfer of heat and materials within chemical processes.
- Applications:
- Heat Exchangers: Devices for transferring heat between fluids.
- Distillation Columns: Used for separating chemical mixtures based on boiling points.
- Membrane Separation: Used for purifying and separating components.
Reaction Engineering
- Definition: Designing and analyzing chemical reactors to maximize yield and efficiency.
- Reactor Types:
- Batch Reactors: Used for small-scale or specialty chemical production.
- Continuous Stirred-Tank Reactors (CSTRs): Used for continuous processes.
- Plug Flow Reactors (PFRs): Used for high-efficiency continuous reactions.
- Key Focus:
- Reaction kinetics and thermodynamics.
- Catalyst design and selection.
Process Optimization
- Definition: Improving process performance by reducing costs, increasing yields, and minimizing waste.
- Techniques:
- Linear and Non-Linear Programming: Used for resource allocation and cost minimization.
- Six Sigma and Lean Manufacturing: Used for process improvement and waste reduction.
- Energy Integration: Used to optimize energy use within the plant.
Safety and Risk Management
- Definition: Identifying, assessing, and mitigating risks associated with chemical processes.
- Tools and Techniques:
- Hazard and Operability Study (HAZOP): Systematic examination of process hazards.
- Quantitative Risk Assessment (QRA): Probability analysis of hazardous events.
- Process Safety Management (PSM): Comprehensive safety management systems.
Environmental and Sustainability Engineering
- Definition: Designing processes that minimize environmental impact and promote sustainability.
- Strategies:
- Green Chemistry: Using environmentally friendly materials and processes.
- Waste Minimization: Reducing by-products and emissions.
- Energy Efficiency: Implementing heat recovery and renewable energy integration.
Applications of Chemical Process Engineering
Petrochemical and Refining Industry
Chemical process engineers are central to the design, optimization, and innovation of processes within the petrochemical and refining industry. They oversee the transformation of crude oil into valuable commodities such as transportation fuels, lubricants, plastics, and synthetic fibers. Traditional processes like fractional distillation, catalytic cracking, and alkylation are now being enhanced by advanced control systems and real-time optimization tools. Environmental considerations are driving the adoption of technologies for sulfur recovery, flare gas recovery, and \(\text{CO}_2\) emissions reduction.
- Processes: Crude oil refining, cracking, and polymerization.
- Products: Fuels such as gasoline and diesel, plastics, and synthetic fibers.
In the transition toward a low-carbon future, chemical engineers are developing electrified steam crackers and evaluating bio-based feedstocks as alternatives to petroleum. These innovations ensure that the refining industry remains relevant in the age of sustainability and climate accountability.
Pharmaceutical Manufacturing
Chemical process engineers contribute to every stage of drug development and manufacturing—from synthetic route design to scale-up and quality assurance. Precision, purity, and compliance with stringent regulations are paramount. Engineers utilize continuous flow reactors, microfluidic platforms, and automation to reduce batch variability and improve efficiency. Techniques like hot melt extrusion and supercritical fluid processing are enabling novel drug delivery methods.
- Processes: Drug synthesis, formulation, and production.
- Technologies:
- Controlled drug release systems.
- Continuous manufacturing for pharmaceutical compounds.
The integration of continuous manufacturing and real-time Process Analytical Technology, or PAT, allows for agile production lines capable of quickly switching between products, supporting the growth of personalized medicine and pandemic preparedness.
Food and Beverage Industry
In the food and beverage sector, chemical process engineering ensures that food is produced safely, efficiently, and sustainably. Engineers work on the pasteurization of dairy, fermentation of beverages, drying of ingredients, and formulation of processed foods. Innovations such as high-pressure processing, ohmic heating, and cold plasma treatment are being explored to extend shelf life while preserving nutrients.
- Processes: Pasteurization, fermentation, and food preservation.
- Technologies: Spray drying, extrusion, and packaging.
Chemical engineers are also applying digital twin technologies and IoT-based sensors to improve traceability, monitor microbial contamination, and optimize ingredient ratios for nutritional balance and consumer satisfaction.
Renewable Energy and Biofuels
This sector benefits greatly from chemical process engineering innovations in converting biomass, algae, and organic waste into usable forms of energy. Engineers work on enzymatic hydrolysis of cellulose, anaerobic digestion for biogas, transesterification for biodiesel, and advanced thermochemical processes like pyrolysis and gasification. Algal bioreactors and genetically modified microbes are being studied to increase biofuel yields.
- Processes: Biomass conversion, bioethanol production, and biodiesel synthesis.
- Technologies:
- Algae cultivation for biofuels.
- Waste-to-energy systems.
Cutting-edge research from organizations like NREL is driving scalable bioenergy technologies that could displace fossil fuels in aviation and shipping—key sectors that are hard to decarbonize using electricity alone.
Water and Wastewater Treatment
Chemical process engineers are tackling the global challenge of clean water through advanced treatment technologies. Processes such as ultrafiltration, reverse osmosis, electrodialysis, and ion exchange are used in industrial and municipal water treatment. Engineers also implement sludge treatment, nutrient recovery, and brine management to minimize environmental impact.
- Processes: Desalination, filtration, and chemical treatment.
- Technologies: Membrane technology and advanced oxidation processes.
As part of smart cities and sustainable infrastructure planning, engineers are integrating AI-driven process controls, real-time water quality sensors, and closed-loop recycling systems into modern water grids—improving resilience and reducing costs.
Emerging Technologies in Chemical Process Engineering
Process Intensification
Process intensification encompasses strategies and technologies designed to make chemical manufacturing more compact, efficient, and sustainable. This means achieving higher conversion rates, better energy usage, and smaller equipment footprints.
- Microreactors: Tiny, highly controlled reactor systems that improve heat and mass transfer, enabling safer and faster reactions. They are especially useful for pharmaceutical synthesis and specialty chemicals.
- Reactive Distillation: Combines chemical reaction with separation processes, such as distillation, in a single unit to reduce energy use and equipment count.
Other intensification techniques include rotating packed beds, oscillatory reactors, and hybrid systems. These methods can reduce plant size, streamline production flows, improve cost-effectiveness, and lower environmental impact.
Digitalization and Industry 4.0
The integration of IoT sensors, cloud analytics, and digital twins is transforming factories into smart, self-optimizing systems.
- Real-Time Monitoring and Predictive Maintenance: Advanced sensor networks and AI algorithms predict equipment issues before they occur, reducing downtime significantly.
- Digital Twins: Virtual replicas of physical process units that allow engineers to simulate changes in feedstock, operating conditions, or maintenance schedules before implementation.
These innovations allow remote monitoring and control and support industry-wide movements toward Industrial IoT adoption, reducing human error and improving productivity.
Green and Sustainable Engineering
Sustainability is reshaping how chemical plants are designed with a triple-bottom-line mentality: planet, people, and profit.
- Renewable Feedstocks: Advanced processes now convert bio-based materials, \(\text{CO}_2\), and even captured methane into chemicals and fuels.
- Zero-Waste Manufacturing: Circular models reuse process water, recycle solvents, and valorize by-products, such as using lignin as a fuel in biorefineries.
Energy integration, biomass utilization, and waste elimination are central to green plant design and life-cycle analysis—key to meeting sustainability goals.
Advanced Catalysis
Catalysis remains at the heart of chemical manufacturing. Emerging trends include radical improvements in efficiency, selectivity, and robustness.
- Nanocatalysts: Ultrafine metal particles or structured supports greatly increase available surface area, enhancing activity and reducing precious metal usage.
- Biomimetic Catalysts: Inspired by natural enzymes, these catalysts bring high specificity and energy efficiency to industrial reactions.
For example, enzyme-like catalysts are now used in green oxidations and polymerization processes, while solid-supported catalysts enable easier separation and recycling.
Modular and Distributed Manufacturing
As an extension of intensification, modular chemical plants consist of standardized units that can be rapidly deployed and scaled.
- Portable chemical modules can produce fertilizers, biofuels, or pharmaceutical precursors on-site or in remote locations.
- Distributed production helps lower transport emissions and supports local economies through small-scale, agile facilities.
This approach mirrors principles from the Hydrogen & Fuel Cell Technologies Office, where micro-scale production aligns with renewable decentralization strategies.
Challenges in Chemical Process Engineering
The translation of chemical concepts into reliable, multi-ton continuous manufacturing networks requires overcoming severe thermodynamic, mechanical, and transport barriers. Chemical process engineers operate under tight environmental mandates, volatile energy pricing, non-ideal multicomponent phase equilibria, and strict safety limits where unmitigated deviations can lead to catastrophic failure.
Process Scale-Up & Transport Phenomena Non-Linearities
Translating lab-scale processes to industrial production while maintaining efficiency and safety is a major challenge in chemical engineering. Small-scale reactions in the laboratory often operate under ideal conditions, with precise temperature control, mixing rates, and pressure parameters. However, scaling these processes up to commercial levels introduces complexities such as heat transfer inefficiencies, unexpected reaction kinetics, and flow dynamics that can result in suboptimal yields or hazardous conditions.
Because reactor volume scales with the cube of linear dimensions (\(V \propto L^3\)) while available surface cooling area scales only quadratically (\(A \propto L^2\)), the surface-to-volume ratio drops sharply (\(A/V \propto 1/L\)). Highly exothermic reactions develop internal thermal hot-spots, secondary decomposition pathways, and flow maldistributions. Engineers must simulate these conditions using pilot plants, computational fluid dynamics (CFD), and digital twins to bridge the gap between research and manufacturing.
Environmental Regulations & Decarbonization Mandates
In response to climate change and environmental degradation, chemical plants are subject to increasingly strict environmental regulations. These include rules regarding air and water pollution, hazardous waste management, and greenhouse gas emissions. Meeting these requirements often requires investment in pollution control technologies, emissions monitoring systems, and environmentally friendly feedstocks.
Regulatory compliance affects process design and can also influence the economic feasibility of a project. For example, the transition to low-sulfur fuels and zero-liquid-discharge (ZLD) facilities is pushing the industry toward innovation in process redesign, advanced brine crystallization, and resource recovery. Many companies consult regulatory guidance from organizations such as the U.S. Environmental Protection Agency (EPA) to support compliance during design and operation.
Energy Efficiency & Exergy Destruction
Energy-intensive sectors like petrochemicals, metals, and cement rely heavily on thermal and electrical energy, often derived from fossil fuels. Enhancing energy efficiency is vital for cost savings and for reducing carbon footprints. Large distillation trains and endothermic cracking furnaces generate significant thermodynamic irreversibility (exergy destruction).
One common strategy is the integration of waste heat recovery systems, which capture and reuse heat from exothermic processes. Another is the adoption of advanced control systems and real-time monitoring technologies that adjust operating parameters for optimal performance. For example, AI-enabled control platforms are now being used to automate energy optimization across distributed process units. Energy-efficient technologies, including membrane separations and low-temperature catalysis, are increasingly being funded by programs such as the U.S. DOE Advanced Manufacturing Office.
Resource Optimization & Feedstock Volatility
Modern chemical process engineering places great emphasis on minimizing raw material consumption, reducing waste generation, and improving atom economy. This supports more sustainable operations while also enhancing economic viability by reducing feedstock and disposal costs.
Process integration techniques, such as pinch analysis and life cycle assessment (LCA), help identify opportunities for resource efficiency throughout the value chain. Circular economy strategies such as material recovery, upcycling of by-products, and real-time tracking of input-output flows are now being built into plant designs. Engineers are also exploring alternative solvents and catalysts that reduce environmental burden and enhance conversion efficiency. As industries strive to close the loop on material use, these optimization efforts will become a hallmark of next-generation process plants.
Future Directions in Chemical Process Engineering
The future of chemical process engineering is anchored in four converging paradigms: closed-loop circular manufacturing, direct carbon valorization, cognitive artificial intelligence and digital twins, and advanced bioprocessing. Together, these technologies transition chemical manufacturing from rigid, fossil-reliant plants into agile, electrified, and self-optimizing ecosystems.
Circular Economy Integration
Designing processes that promote waste reuse and recycling is becoming a central pillar of future chemical manufacturing. Engineers are shifting away from traditional linear models—where raw materials are transformed into products and waste is discarded—toward circular systems that recover, regenerate, and reintegrate resources at every stage.
This includes recovering heat, separating reusable solvents via pervaporation membranes, and converting waste streams into feedstocks. For instance, mixed plastic waste is chemically depolymerized via catalytic pyrolysis into virgin-grade naphtha. A key aspect is the design of circular chemical plants that operate with minimal environmental impact while achieving economic viability.
Carbon Capture and Utilization (CCU)
Carbon Capture and Utilization, or CCU, technologies represent a major step toward decarbonizing the chemical sector. Instead of merely capturing carbon dioxide and storing it underground, CCU enables the transformation of \(\text{CO}_2\) into commercially useful products such as synthetic fuels, urea, and construction materials.
Recent developments include catalytic processes for converting \(\text{CO}_2\) into methanol and electrochemical reduction techniques driven by renewable energy: $$\text{CO}_2 + 3\text{H}_2 \rightleftharpoons \text{CH}_3\text{OH} + \text{H}_2\text{O}, \quad \Delta H_{298\text{K}}^{\circ} = -49.5\text{ kJ/mol}$$ The integration of CCU into existing chemical plants requires innovations in reactive separation, gas absorption, and lifecycle carbon assessments. Organizations such as the Global CCS Institute are actively promoting the scale-up of these technologies through pilot projects and policy frameworks.
Artificial Intelligence in Process Optimization
The role of Artificial Intelligence, or AI, in chemical process engineering is rapidly expanding, enabling real-time optimization, predictive maintenance, and adaptive control of complex systems. Through machine learning algorithms and big data analytics, AI models can identify inefficiencies, predict equipment failures, and optimize reaction parameters far beyond the capabilities of traditional control systems.
Digital twins powered by AI create virtual representations of chemical processes that continuously learn from operational data, enabling enhanced process design and scenario planning. By integrating AI with the Industrial Internet of Things, engineers can create smart factories that are self-correcting and energy-efficient, aligning with the broader goals of Industry 4.0 transformation.
Bioprocess Engineering
Bioprocess engineering is playing a transformative role in shaping the future of sustainable chemical production. By leveraging microbial fermentation, enzymatic catalysis, and cell-free biosynthesis, chemical engineers can produce a wide array of chemicals—such as biofuels, pharmaceuticals, and biodegradable plastics—without relying on petroleum-based feedstocks.
Advances in synthetic biology and metabolic engineering have enabled the customization of microbial pathways for high-yield and low-waste processes. As the cost of genetic sequencing and bioreactor technology continues to decline, scalable and modular bioprocessing platforms are expected to become mainstream in industrial applications. Academic and industry leaders alike are embracing bioprocess solutions to meet global sustainability targets and reduce dependency on fossil fuels.
Systems Engineering Trade-Off Matrix: Core Unit Operations & Intensification
| Unit Operation / Technology | Primary Engineering Advantage | Dominant Physical Constraint / Bottleneck | System Trade-Off & Industrial Reality |
|---|---|---|---|
| Fractional Distillation Column | High throughput; handles large volume flows; mature thermodynamic property databases. | Extremely low thermodynamic exergy efficiency (\(\sim 5\text{–}15\%\)); large reboiler duty; high column height. | Industry workhorse for separations, but constitutes over \(40\%\) of plant-wide thermal energy consumption. |
| Reactive Distillation (RD) | Combines reactor and separator in a single shell; overcomes chemical equilibrium limits via Le Chatelier's principle. | Requires overlapping operational temperature and pressure windows for both reaction kinetics and phase equilibria. | Eliminates recycle loops and saves up to \(50\%\) capital cost, but complex multivariable control is vulnerable to operational drift. |
| Pinch Heat Exchanger Network (HEN) | Maximizes internal heat recovery; minimizes external hot and cold utility demands systematically. | Minimum approach temperature (\(\Delta T_{\min}\)) trade-off: lower \(\Delta T_{\min}\) cuts utility but exponentially grows heat exchange area. | Significantly lowers operational operating costs (OPEX), but increases piping complexity and cross-unit operational coupling. |
| Continuous Stirred-Tank (CSTR) Train | Uniform temperature; excellent heat removal for highly exothermic reactions; simple internal control. | Operates entirely at the lowest reactant concentration (exit concentration); requires larger volume than a PFR for positive kinetics. | Superior thermal safety against runaway, but requires staging multiple tanks in series to approach plug flow conversion. |
Modern Computational Paradigm: Physics-Informed Neural Networks (PINNs) in Plant-Wide Digital Twins
Traditional commercial process simulators (e.g., ASPEN Plus, HYSYS) solve massive sparse nonlinear algebraic and differential equation systems across hundreds of interconnected unit operations. While highly accurate at steady state, executing real-time plant-wide dynamic optimization under fluctuating renewable energy inputs and variable feedstocks is computationally slow, often requiring several minutes to converge a single simulation time-step.
Physics-Informed Neural Networks (PINNs) and Deep Operator Networks (DeepONets) resolve this challenge by learning entire operational manifolds while embedding mass, species, and energy conservation equations directly into their loss functions: $$\mathcal{L}_{\text{total}} = \mathcal{L}_{\text{telemetry}} + \lambda_{\text{mass}}\|\mathcal{R}_{\text{continuity}}\|^2 + \lambda_{\text{energy}}\|\mathcal{R}_{\text{energy}}\|^2$$ where the differential energy conservation operator \(\mathcal{R}_{\text{energy}}\) is strictly enforced: $$\mathcal{R}_{\text{energy}} = \frac{\partial (\rho C_p T)}{\partial t} + \nabla \cdot (\rho C_p \mathbf{u} T) - \nabla \cdot (k \nabla T) - \sum_{j} (-\Delta H_{r,j}) r_j = 0$$
Trained neural surrogates infer full plant dynamic responses across thousands of streams in under 5 milliseconds. This empowers Model Predictive Control (MPC) engines to perform millisecond-scale closed-loop optimization, prevent compressor surge, stabilize distillation compositions during upstream upsets, and maximize economic profit margins autonomously.
Why Study Chemical Process Engineering
Optimizing Industrial Processes
Chemical process engineering focuses on designing and improving manufacturing systems for chemicals and materials. Students learn how to maximize efficiency and minimize costs. This ensures products are produced safely and sustainably.
Reactor and Separation System Design
Students study how to design reactors, distillation columns, and filtration systems. They analyze heat and mass transfer to control product quality. These designs are critical to scaling up lab processes to industrial levels.
Process Control and Automation
The course introduces control systems that regulate temperature, pressure, and flow rates. Students learn how automation enhances consistency, safety, and productivity. These skills are essential in modern process industries.
Environmental and Safety Engineering
Students explore methods to reduce emissions, manage waste, and prevent accidents. They learn about safety standards and risk assessment tools. This knowledge promotes responsible and compliant engineering practices.
Career Opportunities in Manufacturing and Energy
Process engineers are in demand in petroleum, pharmaceuticals, food processing, and renewable energy. Students gain versatile skills applicable to global industries. The field offers rewarding careers with a strong impact on society.
Chemical Process Engineering: Conclusion
Chemical Process Engineering stands as a pivotal discipline within the broader field of engineering, orchestrating the transformation of raw materials into high-value products that underpin nearly every sector—from pharmaceuticals and petrochemicals to food, energy, and advanced materials. At its core, this discipline leverages principles of thermodynamics, fluid mechanics, kinetics, and mass transfer to design, analyze, and improve industrial-scale chemical processes. What once was seen as merely the optimization of factory operations has now evolved into a dynamic, interdisciplinary practice driving global innovation and sustainability.
Modern chemical process engineers are expected to operate at the intersection of efficiency, economics, and environmental responsibility. Through the integration of advanced modeling software, process simulation tools, and real-time monitoring systems, engineers can forecast and fine-tune production outcomes with remarkable accuracy. Concepts such as digital twins, which create virtual replicas of chemical plants, are enabling engineers to predict system behavior and implement preemptive adjustments without halting operations. This not only enhances safety but significantly reduces waste and unplanned downtime.
Sustainability has become a central pillar of chemical process engineering. Engineers are now tasked with minimizing energy consumption, reducing greenhouse gas emissions, and improving resource circularity. By adopting frameworks from sustainable process design, such as green chemistry and lifecycle assessment, the field has shifted from merely complying with regulations to proactively driving ecological stewardship. New plant designs focus on closed-loop systems, solvent recovery, and valorization of waste streams into usable products, redefining what it means to be "efficient" in a climate-conscious era.
Equally important is the integration of smart manufacturing technologies, including sensors, automation, and artificial intelligence. These innovations enable data-driven decisions, reduce human error, and allow for adaptive process control in highly variable production environments. Engineers today must collaborate with data scientists and systems engineers to implement predictive maintenance, optimize batch scheduling, and reduce operational risk in complex chemical facilities.
As industry continues to transition towards cleaner energy and carbon-neutral operations, chemical process engineers will play a leading role in scaling up hydrogen production, integrating carbon capture technologies, and developing bio-based alternatives to petroleum-derived chemicals. Their expertise will also be critical in the design of modular and decentralized production units, which offer flexibility for localized manufacturing and rapid deployment in developing regions.
Looking ahead, the future of chemical process engineering lies in continuous innovation, interdisciplinary collaboration, and a relentless focus on sustainability and resilience. As engineers design the processes that shape global supply chains and daily life, they will not only deliver efficiency and profitability but also help redefine the industrial landscape in alignment with environmental, societal, and technological goals.
Is Chemical Process Engineering Right For You?
Explore career pathways, check your fit, and assess your skills — before you commit to a degree.
Online Assessment Portal: https://prep4uni.online/not-sure-which-field-to-study/?field=chemical-process-engineering
Interactive Tool: Continuous Stirred-Tank Reactor (CSTR) Dynamic Simulator
Use the interactive simulator below to evaluate first-order liquid-phase reaction kinetics in a CSTR (\(V = 500\text{ L}\), \(k = 0.4\text{ min}^{-1}\)). Adjust the inlet flow rate (\(F\)) and reactant concentration (\(C_{A0}\)) to observe real-time dynamic changes in steady-state conversion (\(X_A\)), output concentration (\(C_A\)), and reactor residence time (\(\tau\)).
Canonical Portal URL: https://prep4uni.online/stem/physical-technologies/chemical-engineering/chemical-process-engineering/
Frequently Asked Questions
1. How is chemical process engineering different from chemical engineering as a whole?
Chemical engineering covers many areas, including materials, environmental systems, and product design. Chemical process engineering zooms in on the process route itself: how raw materials flow through reactors, separators, and heat exchangers, and how the overall system is designed, controlled, and optimised to produce valuable products safely and efficiently.
2. What exactly are "unit operations" and why do they matter?
Unit operations are the basic building blocks of processes, such as distillation, absorption, drying, filtration, and heat exchange. By mastering these standard steps, engineers can assemble and analyse complex flowsheets in a modular way and reuse knowledge across very different industries and products.
3. Why is process design such a critical step before building a plant?
Good process design turns a concept into a detailed flowsheet and equipment specification that can actually be built and operated. It determines material and energy usage, safety features, environmental impact, and long-term profitability, so decisions made at this stage have consequences throughout the plant's lifetime.
4. What benefits does process simulation bring to students and practising engineers?
Process simulation lets you experiment virtually with different flowsheets and operating conditions before spending money on hardware. You can test "what if" scenarios, identify bottlenecks, estimate energy demands, and study how changes affect product quality, all within a computer model.
5. How do process engineers design with environmental sustainability in mind?
They look for ways to reduce energy use, recover heat, recycle materials, and avoid hazardous substances. Techniques such as pinch analysis, life-cycle thinking, and green chemistry help them choose cleaner routes, minimise waste, and make more efficient use of water, energy, and raw materials.
6. What is process control, and how does it show up in everyday plant operation?
Process control is the system of sensors, controllers, and final elements, such as valves, that keeps the plant operating at its target conditions. It adjusts flows, temperatures, and pressures in real time so that products remain on specification, equipment stays within safe limits, and the process responds smoothly to disturbances.
7. What does "process integration" mean in practical terms?
Process integration means looking at the whole plant rather than each unit in isolation. In practice, it may involve reusing waste heat from one unit to supply another, recycling intermediate streams, or rearranging the flowsheet so that energy and materials are used more than once before leaving the system.
8. Why is scaling up from a lab experiment to a full-scale plant so challenging?
At large scale, mixing patterns, heat transfer, and flow behaviour can be very different from those in a small lab reactor. Reaction selectivity may change, hot spots may appear, and control becomes more complex. Engineers must redesign equipment and operating strategies to reproduce desirable behaviour safely and economically.
9. How are modern computational and data tools changing process engineering?
Today, engineers use powerful simulation software, optimisation algorithms, and plant data analytics to refine designs and operations. Digital twins and advanced control strategies make it possible to predict how a plant will respond, test changes virtually, and continuously improve performance over time.
10. Why are safety considerations emphasised so strongly in this discipline?
Chemical processes often involve high pressures, high temperatures, and hazardous substances. A poorly designed or poorly controlled process can lead to toxic releases, fires, or explosions. Safety thinking is therefore built into every stage—from initial concept and design through to operation, maintenance, and eventual decommissioning.
Chemical Process Engineering Practice & Assessment Module
Section 1: Foundational Review Questions (Collapsible)
1. What is chemical process engineering, and how does it differ from broader chemical engineering?
Chemical process engineering focuses specifically on how processes are structured, designed, operated, and improved to convert raw materials into valuable products. It concentrates on flowsheets, unit operations, material and energy balances, control, and optimisation. Broader chemical engineering includes these topics but also covers areas such as materials development, product design, and environmental systems.
2. What are unit operations in chemical process engineering, and why are they so important?
Unit operations are the fundamental steps that make up a process, representing physical or chemical transformations such as distillation, absorption, filtration, evaporation, heat exchange, or mixing. By understanding the behaviour of individual unit operations, engineers can assemble and design complex industrial systems in a modular way.
3. How does process design contribute to the efficiency and safety of chemical manufacturing?
Process design converts conceptual chemistry into detailed equipment specifications, PFDs, and P&IDs. It improves efficiency by optimizing heat integration and raw material consumption, while enhancing safety through hazard mitigation, sizing relief systems, and establishing protective operational limits.
4. What role does process simulation play in chemical process engineering?
Process simulation software (e.g., ASPEN Plus, HYSYS) calculates steady-state and dynamic mass and energy balances. It enables virtual experimentation to optimize operating parameters, eliminate bottlenecks, and predict system behavior without incurring physical pilot costs.
5. How do chemical process engineers incorporate environmental sustainability into process design?
Engineers integrate pinch analysis for maximum heat recovery, closed-loop solvent recycling, green chemistry catalysts, and continuous emissions monitoring, ensuring lower life-cycle environmental impact and compliance with zero-discharge targets.
6. What is process control, and why is it vital in chemical process engineering?
Process control monitors key variables (temperature, pressure, flow) using sensors and manipulates control valves via feedback/feedforward loops. It maintains steady-state operation, guarantees product quality, and prevents runaway reactions or equipment damage.
7. Can you explain the concept of process integration and its benefits?
Process integration evaluates the entire plant as an interconnected system. By exchanging heat between hot process streams needing cooling and cold streams needing heating, it drastically reduces external utility requirements and operating expenses.
8. What are some common challenges faced in scaling up chemical processes from lab to plant floor?
Scaling issues include reduced surface area-to-volume ratios causing heat removal bottlenecks, altered fluid mixing dynamics, wall effects in reactors, and local hot-spot formation affecting product selectivity.
9. How do advancements in computational tools impact chemical process engineering practice?
Computational advances enable real-time digital twin optimization, multi-phase CFD simulations, AI-driven predictive maintenance, and automated advanced process control (APC) to dynamically adapt to changing feedstock compositions.
10. Why are safety considerations so significant in chemical process engineering?
Process plants handle high-pressure, flammable, or toxic fluids. Rigorous safety engineering (HAZOP studies, safety integrity levels, relief system design) prevents catastrophic vessel ruptures, chemical releases, fires, and explosions.
Section 2: Thought-Provoking & Analytical Questions (Collapsible)
1. How do engineers balance thermodynamic limits and economic constraints in process design?
Achieving \(99.9\%\) conversion or purity may require exponentially larger reactor volumes or distillation heights due to equilibrium limits. Engineers balance capital expenditure (CAPEX) with operating expenditure (OPEX) by recycling unreacted feed or selecting secondary separation units to optimize net present value.
2. What role do energy recovery networks play in achieving zero-carbon chemical manufacturing?
Heat exchanger networks (HEN) designed via pinch technology capture enthalpy from exothermic reactors to generate process steam or preheat boiler feed water. Eliminating fired utility heaters directly removes scope 1 fossil fuel carbon emissions.
3. Why is understanding reaction kinetics essential when selecting between a CSTR and a Plug Flow Reactor (PFR)?
For positive reaction orders (\(n \gt 0\)), reactant concentration decreases along the reaction path. A PFR maintains higher average reactant concentrations than a CSTR, requiring less total reactor volume for a given target conversion. However, CSTRs provide superior temperature control for highly exothermic reactions.
4. How does process intensification using reactive distillation redefine conventional plant layouts?
Reactive distillation combines chemical reaction and separation within a single column shell. By continuously removing products from the reaction zone, Le Chatelier's principle drives reversible reactions past conventional equilibrium limits, eliminating separate reactor vessels and recycle loops.
5. What computational challenges limit the accuracy of CFD models in multiphase gas-liquid reactors?
Modelling bubble coalescence, breakup, interface mass transfer, and turbulent shear stress across wildly different spatial scales demands immense computational power. Simplified Eulerian-Eulerian or population balance models must balance spatial resolution with processing time.
6. How do digital twins combined with AI transform traditional HAZOP hazard reviews?
Instead of static qualitative brainstorming, AI-driven digital twins simulate thousands of physical deviation scenarios (e.g., valve failure, cooling loss) in real time, quantifying exact transient pressure spikes and time-to-relief to validate safety instrumented systems dynamically.
7. What are the key process engineering barriers in scaling up continuous biomanufacturing?
Key hurdles include biofouling of continuous filtration membranes, cell mutation during extended steady-state bioreactor operations, maintaining absolute sterility over months of operation, and managing shear sensitivity of living cells under high agitation.
8. How does feedforward control outperform simple feedback control in distillation columns?
Feedback control acts only after an off-spec temperature or concentration deviation is measured at the column outlet. Feedforward control measures upstream feed flow or composition disturbances instantly and adjusts reboiler heat or reflux rate preemptively before the disturbance affects product purity.
Section 3: Numerical Problems & Step-by-Step Solutions
- Continuous Stirred-Tank Reactor (CSTR) Sizing: A liquid-phase first-order reaction \(A \to B\) with rate constant \(k = 0.25\text{ min}^{-1}\) processes a feed stream with flow rate \(F = 100\text{ L/min}\) and initial concentration \(C_{A0} = 2.0\text{ mol/L}\). Calculate the required reactor volume (\(V\)) in Liters to achieve \(80\%\) conversion (\(X_A = 0.80\)) at steady state.
Solution:
1) Target outlet concentration: \(C_A = C_{A0} \cdot (1 - X_A) = 2.0\text{ mol/L} \cdot (1 - 0.80) = 0.40\text{ mol/L}\).
2) CSTR performance equation: \(V = \frac{F \cdot (C_{A0} - C_A)}{-r_A}\), where \(-r_A = k \cdot C_A\).
3) Reaction rate: \(-r_A = 0.25\text{ min}^{-1} \cdot 0.40\text{ mol/L} = 0.10\text{ mol/(L}\cdot\text{min)}\).
4) Substitute values: \(V = \frac{100\text{ L/min} \cdot (2.0 - 0.40)\text{ mol/L}}{0.10\text{ mol/(L}\cdot\text{min)}} = \frac{160}{0.10} = \mathbf{1600\text{ L}}\). - Heat Exchanger Heat Duty and LMTD: A counter-current shell-and-tube heat exchanger cools a hot process fluid flowing at \(\dot{m}_h = 2.0\text{ kg/s}\) from \(T_{h1} = 120\,^\circ\text{C}\) to \(T_{h2} = 60\,^\circ\text{C}\) (\(c_{p,h} = 2.5\text{ kJ/(kg}\cdot\text{K)}\)). Cooling water enters at \(T_{c1} = 20\,^\circ\text{C}\) and exits at \(T_{c2} = 50\,^\circ\text{C}\). Calculate total heat duty (\(Q\)) in \(\text{kW}\) and the Logarithmic Mean Temperature Difference (\(\Delta T_{\text{LMTD}}\)) in \(^\circ\text{C}\).
Solution:
1) Heat duty: \(Q = \dot{m}_h \cdot c_{p,h} \cdot (T_{h1} - T_{h2}) = 2.0\text{ kg/s} \cdot 2.5\text{ kJ/(kg}\cdot\text{K)} \cdot (120 - 60)\text{ K} = \mathbf{300\text{ kW}}\).
2) Temperature differences at terminal ends:
\(\Delta T_1 = T_{h1} - T_{c2} = 120 - 50 = 70\,^\circ\text{C}\).
\(\Delta T_2 = T_{h2} - T_{c1} = 60 - 20 = 40\,^\circ\text{C}\).
3) Calculate LMTD: \(\Delta T_{\text{LMTD}} = \frac{\Delta T_1 - \Delta T_2}{\ln(\Delta T_1 / \Delta T_2)} = \frac{70 - 40}{\ln(70 / 40)} = \frac{30}{\ln(1.75)} = \frac{30}{0.5596} = \mathbf{53.61\,^\circ\text{C}}\). - Pinch Technology Minimum Hot Utility: A process requires heating a cold stream from \(30\,^\circ\text{C}\) to \(110\,^\circ\text{C}\) (Heat capacity flow rate \(CP_C = 4.0\text{ kW/K}\)) and cooling a hot stream from \(150\,^\circ\text{C}\) to \(50\,^\circ\text{C}\) (\(CP_H = 3.0\text{ kW/K}\)). Assuming a minimum approach temperature \(\Delta T_{\min} = 10\text{ K}\), calculate the minimum hot utility requirement (\(Q_{H,\min}\)) in \(\text{kW}\).
Solution:
1) Enthalpy required by cold stream: \(Q_{\text{Cold}} = CP_C \cdot (110 - 30) = 4.0\text{ kW/K} \cdot 80\text{ K} = 320\text{ kW}\).
2) Enthalpy available from hot stream: \(Q_{\text{Hot}} = CP_H \cdot (150 - 50) = 3.0\text{ kW/K} \cdot 100\text{ K} = 300\text{ kW}\).
3) Shifted temperatures: Shifted Hot: \(150 \to 145\,^\circ\text{C}\), \(50 \to 45\,^\circ\text{C}\); Shifted Cold: \(30 \to 35\,^\circ\text{C}\), \(110 \to 115\,^\circ\text{C}\).
4) Heat cascade analysis across temperature intervals demonstrates minimum hot utility needed at the pinch: \(Q_{H,\min} = Q_{\text{Cold}} - Q_{\text{Hot}} + \text{Pinch allowance} = 320\text{ kW} - 300\text{ kW} + 20\text{ kW} = \mathbf{40\text{ kW}}\). - Distillation Column Reflux Ratio: A binary distillation column operates with a minimum reflux ratio \(R_{\min} = 1.25\). If the design specifies an operating reflux ratio \(R = 1.5 \cdot R_{\min}\), calculate the operational reflux ratio (\(R\)) and the required boil-up vapor rate \(V\) (\(\text{kmol/h}\)) exiting the reboiler if the distillate flow rate \(D = 100\text{ kmol/h}\).
Solution:
1) Calculate operating reflux ratio: \(R = 1.5 \cdot 1.25 = \mathbf{1.875}\).
2) Reflux ratio definition: \(R = L / D \Rightarrow L = R \cdot D = 1.875 \cdot 100\text{ kmol/h} = 187.5\text{ kmol/h}\).
3) Column top vapor flow: \(V_T = L + D = 187.5 + 100 = \mathbf{287.5\text{ kmol/h}}\). - Overall Material Balance with Recycle: A reactor loop converts reactant A to product B with a single-pass conversion of \(20\%\) (\(x_{sp} = 0.20\)). The fresh feed rate \(F_0 = 1000\text{ kg/h}\) of pure A. If unreacted A is separated and recycled back to the reactor inlet with zero waste purge, calculate the total feed rate entering the reactor (\(F_{\text{total}}\)) and the recycle flow rate (\(R_{\text{flow}}\)) in \(\text{kg/h}\).
Solution:
1) Overall system steady-state conversion must be \(100\%\) (no purge): Product B formed \(= F_0 = 1000\text{ kg/h}\).
2) Single-pass conversion formula: \(\text{Product formed} = x_{sp} \cdot F_{\text{total}}\).
3) Solve for total reactor feed: \(1000\text{ kg/h} = 0.20 \cdot F_{\text{total}} \Rightarrow F_{\text{total}} = \frac{1000}{0.20} = \mathbf{5000\text{ kg/h}}\).
4) Recycle rate: \(R_{\text{flow}} = F_{\text{total}} - F_0 = 5000 - 1000 = \mathbf{4000\text{ kg/h}}\). - Pump Shaft Power Requirement: An industrial centrifugal pump transfers a liquid product (\(\rho = 1100\text{ kg/m}^3\)) at a volumetric flow rate \(Q = 0.05\text{ m}^3\text{/s}\) across a total dynamic head \(H = 40\text{ meters}\). If the overall pump-motor efficiency \(\eta = 75\%\) (\(\eta = 0.75\)), calculate the required electrical shaft power (\(P\)) in \(\text{kW}\) (\(g = 9.81\text{ m/s}^2\)).
Solution:
1) Hydraulic power: \(P_{\text{hyd}} = \rho \cdot g \cdot Q \cdot H = 1100\text{ kg/m}^3 \cdot 9.81\text{ m/s}^2 \cdot 0.05\text{ m}^3\text{/s} \cdot 40\text{ m} = 21,582\text{ W} = 21.582\text{ kW}\).
2) Required shaft electrical power: \(P_{\text{shaft}} = \frac{P_{\text{hyd}}}{\eta} = \frac{21.582\text{ kW}}{0.75} = \mathbf{28.78\text{ kW}}\). - Plug Flow Reactor (PFR) Volume Calculation: Compare a PFR to a CSTR for the same first-order liquid-phase reaction (\(k = 0.25\text{ min}^{-1}\), \(F = 100\text{ L/min}\), \(X_A = 0.80\)). Calculate the PFR volume (\(V_{\text{PFR}}\)) in Liters.
Solution:
1) PFR design equation: \(V_{\text{PFR}} = F \cdot \int_0^{X_A} \frac{dX}{-r_A} = \left(\frac{F}{k}\right) \cdot \ln\left(\frac{1}{1 - X_A}\right)\).
2) Substitute parameters: \(V_{\text{PFR}} = \left(\frac{100\text{ L/min}}{0.25\text{ min}^{-1}}\right) \cdot \ln\left(\frac{1}{1 - 0.80}\right)\).
3) Evaluate logarithmic term: \(\ln(1 / 0.20) = \ln(5) = 1.6094\).
4) \(V_{\text{PFR}} = 400\text{ L} \cdot 1.6094 = \mathbf{643.78\text{ L}}\) (compared to \(1600\text{ L}\) for the equivalent CSTR).