
Energy and Resource Efficiency in Manufacturing education is, at its core, an education in attention. It trains the eye to notice where energy quietly leaks away, where material becomes scrap without anyone calling it a “decision,” and where a process that looks productive is actually expensive in hidden ways. This diagram shows how that discipline is built. The inputs bring both the formal knowledge (curricular resources) and the lived reality (industry practices), so students learn the language of efficiency without losing touch with shop-floor constraints. The controls—guidelines and evaluation criteria—act like a measuring tape: they keep the learning honest, comparable, and tied to outcomes rather than slogans. Inside the central function, learners practice turning questions into numbers: How much energy does a step consume? Where is the largest loss? What changes reduce waste without harming quality or throughput? The mechanisms—simulation models and material analysis tools—make these questions answerable, letting students test alternatives, explore trade-offs, and see consequences before resources are spent. The outputs are therefore more than “awareness”: they are practical insights and capable students who can walk into a manufacturing setting and speak the language of improvement with evidence, not guesswork.
- Thermodynamic Conservation & Exergy Destruction: Application of the First and Second Laws of Thermodynamics to industrial mass and energy balances, quantifying Specific Energy Consumption (\(\text{SEC}\)) and recuperative heat exchange.
- Affinity Scaling & Electromechanical Optimization: Governing cubic relationships in turbomachinery power consumption (\(P \propto N^3\)) and automated variable-load stabilization using Variable Frequency Drives (VFDs).
- AI-Driven & Digital Twin Systems: Transitioning classical supervisory control toward Physics-Informed Neural Networks (PINNs), Neural Operators, and real-time edge Model Predictive Control (MPC) for dynamic decarbonization.
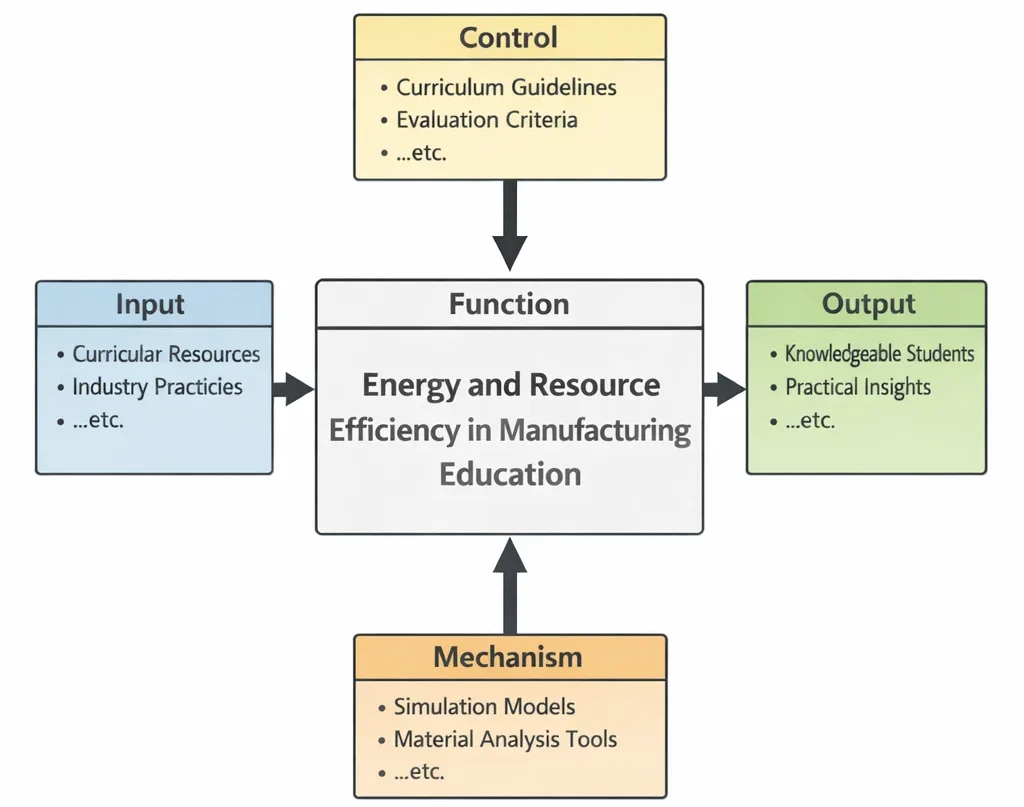
This IDEF0 (Input–Control–Output–Mechanism) diagram presents Energy and Resource Efficiency in Manufacturing Education as a clear educational workflow. Inputs on the left—curricular resources and industry practices—provide the foundational knowledge and real-world context. Controls from the top—curriculum guidelines and evaluation criteria—define what learners must cover and how competence is assessed. In the center, the function (Energy and Resource Efficiency in Manufacturing Education) organizes these elements into structured learning and applied understanding. Outputs on the right—knowledgeable students and practical insights—represent the learning results that can be carried into factories, projects, and decision-making. Mechanisms at the bottom—simulation models and material analysis tools—make the topic measurable and testable, enabling learners to explore trade-offs, quantify improvements, and connect theory to manufacturing realities.
Energy and resource efficiency in manufacturing has become an essential pillar of sustainable industrial development. With the dual pressures of environmental responsibility and economic competitiveness, today’s manufacturing systems are evolving rapidly to reduce waste, optimize inputs, and minimize emissions. This shift is tightly connected with broader advances in Industrial and Manufacturing Technologies, where integration of digital tools, lean practices, and system redesign is transforming both production and resource use.
The implementation of Sustainable Manufacturing strategies is central to this transformation, aiming for high performance with minimal environmental impact. Technologies such as Smart Manufacturing and Industry 4.0 and Digital Twin Technology allow factories to simulate operations, monitor real-time data, and make energy-aware decisions dynamically. These capabilities are enhanced when combined with Computer-Integrated Manufacturing (CIM) platforms that synchronize energy management with production scheduling.
Improvements in material utilization are being driven by innovations in Additive Manufacturing (3D Printing) and Advanced Materials and Manufacturing Technologies. These methods support localized production, complex part optimization, and material recovery—all of which contribute to energy savings across the supply chain. Their effectiveness is further enhanced by robust Manufacturing Quality Control and Assurance processes that reduce defects and prevent resource loss.
Efficient energy use is also enabled through intelligent automation. Integration with Industrial Automation and Robotics and careful attention to Human Factors and Ergonomics in Manufacturing ensure that energy is spent effectively in both human and machine activity. By adopting Lean Manufacturing principles, operations are further streamlined to eliminate inefficiencies that drain energy or consume excess resources.
Systems-level efficiency is also shaped by strategic Supply Chain Management. From sourcing to logistics, each decision can impact total energy consumption. Digital coordination across the production network leads to better-informed procurement and transportation choices that support sustainable goals. These logistics are tightly coupled with disciplines such as Manufacturing and Production Engineering and Mechanical Design and CAD, which define the geometry and material flows of production.
Energy efficiency efforts must be grounded in sound physical science. Knowledge from Thermodynamics and Heat Transfer, Fluid Mechanics and Hydraulics, and Solid Mechanics underpins the thermal and mechanical systems being optimized. The intelligent application of these principles is seen in sectors like Automotive Engineering and Biomechanical Engineering, where efficiency is key to performance and sustainability.
A holistic energy strategy must also consider systems control, as taught in Control Systems in Mech Engineering. These systems maintain process balance and avoid unnecessary energy expenditure. Likewise, nanotechnology innovations—explored in Nanotechnology and Advanced Materials in Mech Eng—enable advanced coatings and materials that improve thermal regulation and energy retention in equipment.
Finally, these strategies are brought to life by people and technologies working together. In the context of Robotics and Automation in Mech Eng and systems-wide digital design integration, engineers are empowered to transform vision into scalable, efficient reality. The field continues to evolve with every development in Mechanical Engineering, bridging tradition and transformation in pursuit of a more sustainable industrial future.

Efficiency Engineering: Optimising Energy Use and Material Resources
Navigate through the core topics of Industrial & Manufacturing Technologies to see how energy and resource efficiency interacts across different manufacturing domains:
Industrial & Manufacturing Overview
Positions resource efficiency within broader industrial system performance and baseline operational metrics.
Energy & Resource Efficiency (Current)
Optimises energy consumption and material usage to improve sustainability, eliminate waste, and reduce operating costs.
Sustainable Manufacturing
Aligns efficiency strategies directly with long-term environmental objectives and circular economy practices.
Process Design
Develops efficient plant workflows that minimize raw material scrap and optimize thermal/electrical loads.
Lean Manufacturing
Reduces non-value-adding operational waste and improves physical resource utilization on the factory floor.
Smart Manufacturing
Uses real-time data analytics and IoT sensor networks to monitor and optimize energy draw dynamically.
Digital Twin
Simulates virtual energy consumption models and material throughput flows for pre-implementation optimization.
Automation
Enhances overall system efficiency through precise, highly repeatable, and energy-aware robotic operations.
CIM
Integrates enterprise energy performance metrics across centralized production planning software environments.
Additive Manufacturing
Minimizes raw material waste through precise layer-by-layer fabrication compared to subtractive techniques.
Advanced Materials
Supports efficient production by employing high-performance alloys and composites engineered for lower mass.
Supply Chain
Optimises resource flow and transportation fuel efficiency across international distribution networks.
Quality Control
Ensures resource efficiency changes do not compromise component structural integrity or tolerances.
Human Factors
Enhances worker physical performance and motion safety to support sustainable workstation workflows.
Core Concepts in Energy and Resource Efficiency
Energy Efficiency
Definition: Using less energy to achieve the same output, thereby reducing energy waste. This principle involves optimizing systems, technologies, and behaviors to minimize energy input without compromising productivity.
Goals:
- Lowering energy costs by decreasing consumption across industrial processes, lighting, HVAC systems, and machinery.
- Reducing greenhouse gas (GHG) emissions, which directly contributes to climate change mitigation and compliance with global climate agreements.
- Enhancing operational efficiency by streamlining processes, minimizing idle energy use, and incorporating smart energy management systems that adjust to load and demand.
Examples:
- Upgrading to energy-efficient motors and lighting systems like LED bulbs and high-efficiency HVAC units, as well as retrofitting older buildings with energy-smart insulation and control systems.
- Deploying variable frequency drives (VFDs) in motor operations to reduce unnecessary energy use during low-load periods.
- Implementing real-time energy monitoring platforms to identify inefficiencies and optimize energy use dynamically.
Resource Efficiency
Definition: Maximizing the value extracted from raw materials while minimizing waste and losses. It encourages designing systems where each material is used for its full potential before being discarded or repurposed.
Goals:
- Extending the lifecycle of materials by promoting reuse, refurbishment, and remanufacturing practices.
- Reducing reliance on virgin resources through the use of secondary raw materials and closed-loop systems.
- Enhancing recyclability of components and packaging by selecting materials that can be easily separated, sorted, and repurposed at end-of-life.
Examples:
- Using lightweight materials in automotive manufacturing to reduce resource consumption while improving fuel efficiency and lowering emissions.
- Designing modular products that facilitate repair and component replacement rather than full disposal.
- Adopting water-efficient production processes and recovering waste heat in thermal systems.
Sustainable Manufacturing Practices
Definition: Production methods that minimize environmental impacts and ensure sustainable resource use, aligning with long-term ecological balance and economic viability.
Goals:
- Reduce pollution and waste through cleaner production techniques, closed-loop systems, and real-time environmental monitoring.
- Promote circular economy principles such as product lifecycle extension, reuse of industrial byproducts, and regenerative design.
- Adopt renewable energy and green technologies that reduce fossil fuel dependency and harmful emissions. For example, as detailed by the U.S. Department of Energy’s Advanced Manufacturing Office, clean energy initiatives are transforming industrial sectors through innovation.
Circular Economy Integration
Definition: Designing processes and products to minimize waste and enable reuse, recycling, and regeneration of resources. This strategy challenges the traditional linear model of "take-make-dispose."
Applications:
- Using recycled plastics to manufacture new consumer goods while reducing environmental burdens from virgin plastic production.
- Designing products for disassembly and material recovery, allowing manufacturers to retrieve high-value components at end-of-life and reduce dependency on new material inputs.
- Creating reverse logistics systems to collect used goods for reintegration into the production cycle.
Renewable Energy Integration
Definition: Incorporating renewable energy sources like solar, wind, and biomass into manufacturing operations to decarbonize production and improve energy security.
Benefits:
- Reduces dependence on fossil fuels and exposure to volatile energy markets.
- Cuts operational carbon emissions significantly, supporting sustainability goals and corporate social responsibility targets.
Examples:
- Solar panels powering manufacturing facilities and supplementing grid electricity, especially during peak demand hours.
- Biomass boilers providing heat for industrial processes using organic waste as a fuel source, creating closed-loop systems and reducing landfill use.
- Wind turbines deployed on industrial campuses to support direct consumption of clean electricity and feed surplus energy into the grid.
Advanced Computational Paradigms in Industrial Decarbonization
Modern resource and energy optimization has progressed beyond static empirical balance equations to real-time, high-fidelity computational modeling. Advanced computational mechanics and machine learning allow engineers to predict thermodynamic bottlenecks, prevent exergy destruction, and synchronize multi-carrier energy microgrids without taking production machinery offline.
Physics-Informed Neural Networks (PINNs) & Neural Operators in Thermal Systems
Classical computational fluid dynamics (CFD) and finite element analysis (FEA) for waste heat boilers and recuperative heat exchangers are computationally prohibitive for real-time edge control. Contemporary implementations integrate Physics-Informed Neural Networks (PINNs), embedding the governing Navier-Stokes and energy conservation equations directly into the neural network loss function:
$$\mathcal{L}_{\text{total}} = \mathcal{L}_{\text{data}} + \lambda_{\text{NS}} \|\rho (\mathbf{u} \cdot \nabla)\mathbf{u} + \nabla p - \mu \nabla^2 \mathbf{u}\|^2 + \lambda_{\text{energy}} \|\rho c_p (\mathbf{u} \cdot \nabla T) - k \nabla^2 T - \dot{q}_v\|^2$$
Where \(\mathbf{u}\) denotes the velocity vector, \(p\) is fluid pressure, \(T\) is local temperature, \(k\) is thermal conductivity, and \(\dot{q}_v\) represents volumetric heat generation. Furthermore, Fourier Neural Operators (FNOs) learn mesh-independent mappings between continuous parameter spaces, enabling instantaneous zero-shot resolution transfer for varying flue gas velocities across recuperators during abrupt factory shift transitions.
Edge Digital Twins & Dynamic Model Predictive Control (MPC)
Industrial load balancing leverages edge microcontrollers and FPGA-accelerated digital twins executing real-time Model Predictive Control (MPC). By monitoring electrical utility pricing signals (\(\$/\text{kWh}\)) and machine tool states via high-throughput OPC-UA protocols, MPC solves a constrained receding horizon optimization problem:
$$\min_{\{u_k\}} \sum_{k=0}^{N-1} \left[ C_k \cdot P_{\text{grid}}(x_k, u_k) \Delta t + \alpha \|x_k - x_{\text{target}}\|^2 + \beta \|\Delta u_k\|^2 \right] \quad \text{subject to} \quad T_{\text{die}} \le T_{\text{crit}}, \quad \dot{m}_{\text{part}} \ge \dot{m}_{\text{quota}}$$
This formulation enforces physical constraints (such as die-casting solidification thresholds and hourly delivery quotas) while dynamically shifting high-power motor ramps and thermal batch cycles to off-peak grid periods, achieving automated demand-side response without compromising mechanical tolerances.
Systems Engineering Trade-Off Matrix: Industrial Efficiency Interventions
Implementing efficiency interventions requires rigorous multi-variable trade-off analysis. The structured matrix below outlines core capital, operational, and thermodynamic compromises inherent to plant-scale retrofits:
| Intervention Strategy | Primary Efficiency Mechanism | Engineering Limitations & Risks | System Compromise & Mitigation |
|---|---|---|---|
| VFD Retrofits on Turbomachinery | Modulates motor shaft RPM via inverter frequency; eliminates valve throttling losses (\(P \propto N^3\)). | Harmonic distortion on plant bus; high-frequency voltage reflections (\(dV/dt\)) causing motor bearing pitting. | Requires active harmonic filters and shaft grounding rings; increases electrical enclosure footprint. |
| Recuperative Flue Gas Heat Exchangers | Preheats combustion air or feedwater using exhaust sensible heat, directly reducing fuel consumption. | Acid dew-point corrosion if exhaust cools below sulfur condensation limits (\(T_{\text{flue}} \lt 130^\circ\text{C}\)); backpressure on blowers. | Requires high-nickel alloys or borosilicate tubes; must maintain minimum exhaust threshold to preserve stack buoyancy. |
| Subtractive to Additive (DMLS) Transition | Reduces Buy-to-Fly ratio from \(\gt 10:1\) down to \(\sim 1.2:1\); eliminates billet milling scrap. | High specific electrical energy per kilogram sintered; powder oxidation degradation; slow batch throughput. | Economically and energetically justifiable primarily for complex, high-value alloys (Inconel, Ti-6Al-4V) rather than bulk mild steel. |
| Closed-Loop Process Water Recycling | Recovers up to 90–95% of industrial rinse effluent using membrane filtration and reverse osmosis (RO). | Biofouling and scaling on membranes; high electrical pumping power required for high-osmotic pressure reject brine. | Requires chemical anti-scalant dosing and scheduled clean-in-place (CIP) regimens; generates concentrated brine disposal stream. |
Applications of Energy and Resource Efficiency in Manufacturing
About This Interactive Simulator:
This real-time Energy & Resource Efficiency Simulator models an industrial production cell. Adjust line throughput speed and waste heat recovery efficiency to evaluate total electrical power demand, heat losses, and overall specific energy intensity in real time.
- Solid Cyan Line: Baseline electrical power consumption (\(\text{kW}\)) across a 24-hour manufacturing shift.
- Dashed Amber Line: Optimized net energy demand (\(\text{kW}\)) incorporating active waste heat recovery and variable-speed modulation.
- Interactive Sliders: Dynamically alter throughput (50–200 Units/Hr) and recovery efficiency (0–80%).
Industrial Energy Demand & Waste Heat Recovery Simulator
Energy Management Systems (EnMS)
Frameworks for systematically improving energy efficiency in manufacturing, such as ISO 50001, encourage a structured approach to identifying inefficiencies, setting performance goals, and measuring progress toward those objectives on a continual basis.
Key Components:
- Energy Audits: Identify areas of energy waste by analyzing equipment, building insulation, and utility bills to pinpoint underperforming systems.
- Performance Monitoring: Use IoT sensors to track energy usage in real-time, providing a data-rich environment for better decision-making.
- Target Setting: Establish goals for energy reduction based on benchmarking and predictive modeling techniques that align with corporate sustainability strategies.
Example: A factory reducing energy consumption by optimizing HVAC systems and production schedules, resulting in decreased utility costs and improved air quality control.
Process Optimization
Refining manufacturing processes to minimize resource and energy use while maximizing productivity involves analyzing workflows, identifying inefficiencies, and applying corrective strategies.
Techniques:
- Implementing Lean Manufacturing principles to reduce waste by eliminating non-value-adding activities.
- Using advanced control systems and real-time analytics to ensure process precision and reduce variability.
Example: A chemical plant optimizing reaction temperatures and pressures to save energy while improving reaction yields and product consistency.
Waste Heat Recovery
Capturing and reusing heat generated during industrial processes reduces overall energy demand and enhances process efficiency.
Applications:
- Preheating raw materials using exhaust heat from combustion systems, which reduces fuel consumption.
- Generating electricity from waste heat in power plants using Organic Rankine Cycle systems or thermoelectric converters.
Example: A steel mill using waste heat recovery systems to power auxiliary equipment like cranes and conveyors, contributing to reduced operating costs and emissions.
Material Efficiency
Reducing material waste by improving design, production, and recycling practices allows manufacturers to achieve more with fewer inputs.
Techniques:
- Using high-precision cutting tools and CNC machining to minimize scrap and improve dimensional accuracy.
- Designing products with fewer components or modular parts to reduce material complexity and facilitate disassembly and recycling.
Example: Lightweighting in automotive manufacturing to reduce metal consumption, improve fuel efficiency, and lower emissions during the vehicle’s lifecycle.
Water Conservation and Recycling
Reducing water usage and recycling wastewater in manufacturing processes preserves freshwater resources and cuts utility costs.
Techniques:
- Installing closed-loop water systems to reuse cooling water, especially in heat-intensive industries such as steel and chemicals.
- Treating and reusing greywater for non-potable purposes such as floor washing, landscaping, or toilet flushing.
Example: A semiconductor plant reusing treated wastewater for cleaning operations, reducing the demand for freshwater intake and improving environmental compliance. For additional insights into sustainable water management, the EPA’s Sustainable Management of Water page offers practical strategies for industries.
Renewable Energy Adoption
Powering manufacturing operations with renewable energy sources such as solar, wind, geothermal, or biomass reduces dependence on fossil fuels and supports carbon neutrality goals.
Applications:
- Installing rooftop solar panels for energy-intensive facilities to offset daytime energy usage with clean electricity.
- Using wind energy to power heavy machinery or storage systems during periods of high demand.
Example: A textile factory running on solar and wind energy to reduce its carbon footprint and earn sustainability certifications that boost brand reputation.
Digital Twin Technology
Creating virtual replicas of physical systems to simulate and optimize energy and resource use allows for proactive decision-making and performance forecasting.
Applications:
- Predicting energy savings from process changes by running simulations of modified production setups.
- Simulating resource flows, temperature control, and equipment lifecycles to identify inefficiencies and potential improvements.
Example: A factory using digital twins to test energy-efficient production schedules, adjust runtime variables, and align maintenance windows with energy-saving opportunities.
Automation and Robotics
Automating repetitive tasks enhances precision and reduces resource waste, thereby increasing consistency, safety, and scalability in manufacturing operations.
Applications:
- Robots in assembly lines to minimize material errors, improve repeatability, and eliminate human fatigue-related defects.
- Automated quality control systems using vision sensors and AI algorithms to identify flawed components and reduce defective product rates.
Example: A robotic arm ensuring precise application of adhesives, reducing waste and improving product reliability across multiple shifts with minimal supervision.
Technologies Supporting Energy and Resource Efficiency
IoT and Smart Sensors
Role: Provide real-time data on energy consumption and resource usage, offering granular visibility into manufacturing systems and utilities.
Applications: Monitoring machine performance to identify inefficiencies such as overuse of energy, leaks, or suboptimal operating conditions, enabling proactive adjustments.
Example: IoT sensors tracking electricity usage in industrial machines to flag anomalies, schedule maintenance, and shut down idle equipment automatically during non-peak hours.
Artificial Intelligence (AI)
Role: Analyze large datasets to identify patterns and optimize energy use, often through machine learning algorithms that adapt over time.
Applications: Predictive analytics for energy demand forecasting, enabling companies to align consumption with supply in real time and participate in smart grid systems.
Example: AI systems adjusting equipment operation during low energy demand periods to take advantage of lower utility rates and reduce overall energy bills, while still meeting production schedules efficiently.
Additive Manufacturing
Role: Reduces material waste by building products layer by layer, unlike subtractive manufacturing methods which generate excess scrap material.
Applications: Producing lightweight components for aerospace applications that improve fuel efficiency, reduce emissions, and minimize lifecycle environmental impact.
Example: 3D printing prototypes to avoid waste from traditional machining, which often involves cutting away large amounts of material, particularly from high-value metals like titanium or aluminum.
Blockchain Technology
Role: Enhances traceability and accountability in resource use by creating secure, tamper-proof records across supply chains and production processes.
Applications: Verifying the sustainability of raw materials, documenting ethical sourcing, and ensuring compliance with environmental standards throughout procurement and production.
Example: Blockchain tracking the origin of recycled materials to validate claims of eco-friendly product composition, support certifications, and build consumer trust. A related initiative can be explored through IBM’s blockchain supply chain solutions, which provide detailed frameworks for traceable and efficient resource management.
Renewable Energy Systems
Role: Powering operations with clean, renewable energy, helping businesses reduce reliance on fossil fuels, meet decarbonization goals, and enhance energy resilience.
Examples: Solar farms providing decentralized power for remote facilities, wind turbines driving mechanical or electrical systems in real-time, and geothermal energy systems offering consistent heating and cooling solutions with low emissions and high reliability.
Applications Across Industrial Sectors
Automotive Manufacturing
Energy Reduction: Using lightweight materials to improve fuel efficiency in vehicles while also reducing the energy required during manufacturing due to simpler handling and reduced processing demands.
Renewable Energy Integration: Solar-powered manufacturing plants with rooftop panels, energy storage systems, and real-time energy management dashboards to ensure optimal energy usage throughout production cycles.
Example: BMW's energy-efficient paint shops using renewable energy and robotic systems to minimize water, electricity, and chemical usage during surface treatments, contributing to their corporate sustainability goals.
Food and Beverage Industry
Water Conservation: Reusing water from cleaning processes through filtration, sterilization, and closed-loop systems to drastically lower total water withdrawal and discharge volumes.
Energy Efficiency: Waste heat recovery in brewing and baking by capturing exhaust energy from ovens and boilers to preheat incoming water or air, reducing fuel consumption and operating costs.
Example: Breweries capturing CO₂ emissions for reuse in carbonation, refrigeration, or as an input for fertilizer production, demonstrating circularity in emissions and resource usage.
Electronics Manufacturing
Resource Optimization: Reducing rare earth material usage in components by redesigning products to utilize fewer critical minerals or integrating substitute materials with similar functionality but lower environmental impact.
Waste Management: Recycling defective products and e-waste through disassembly, precious metal recovery, and circuit board reclamation to reduce landfill disposal and resource depletion.
Example: Apple using recycled aluminum in device casings, sourcing material from its own product take-back programs, thereby reducing carbon emissions and mining dependencies.
Cement and Steel Industries
Energy Efficiency: Using alternative fuels and waste heat recovery to lower the carbon footprint and energy demands of high-temperature processing operations like clinker and steel production.
Material Recycling: Incorporating industrial byproducts like fly ash, slag, and construction debris to reduce reliance on virgin raw materials and enhance product performance in concrete and steel blends.
Example: Steel plants using electric arc furnaces powered by renewable energy to melt scrap metal, achieving significant emission reductions compared to traditional blast furnaces and promoting circularity in materials.
Textile Industry
Water Recycling: Treating wastewater from dyeing processes for reuse using advanced filtration, ozone oxidation, and membrane bioreactors to meet environmental discharge standards and conserve water.
Renewable Energy: Solar and wind energy powering textile mills, including spinning, weaving, and finishing operations, often integrated with smart grid systems to ensure energy reliability and cost savings.
Example: Factories using waterless dyeing technologies, such as supercritical CO₂ dyeing, to eliminate the need for water altogether while improving colorfastness and reducing chemical loads in production.
Benefits of Energy and Resource Efficiency
- Cost Savings: Reducing energy consumption and waste lowers operational costs significantly. By optimizing systems, automating energy-intensive operations, and reducing dependency on non-renewable resources, companies can achieve long-term financial gains. These savings not only contribute to a healthier bottom line but also free up capital for investment in innovation and sustainability initiatives.
- Enhanced Productivity: Streamlined processes improve output and efficiency by minimizing delays, energy losses, and material handling errors. When manufacturing lines are optimized for energy use and resource flow, it leads to quicker cycle times, fewer defects, and smoother transitions between production phases, which collectively elevate overall productivity and competitiveness.
- Environmental Sustainability: Reduces carbon emissions and conserves natural resources through smarter consumption and improved process management. Energy-efficient operations produce fewer greenhouse gases, while resource-efficient practices minimize landfill contributions and depletion of critical materials. These strategies support broader environmental goals and help align industrial activities with international climate agreements such as the Paris Accord.
- Regulatory Compliance: Meets environmental standards and avoids penalties by proactively adhering to energy and resource efficiency benchmarks. Implementing best practices reduces the likelihood of violations, helps secure permits faster, and ensures smooth audits. In some regions, efficiency standards are tied to incentives, so compliant businesses can also benefit from tax relief or preferential procurement status.
- Improved Brand Reputation: Demonstrates commitment to sustainability, appealing to eco-conscious consumers, investors, and partners. Transparent reporting on resource use and sustainability metrics enhances trust and positions companies as responsible and forward-thinking. Brands that integrate green practices into their identity often see increased loyalty, stronger media attention, and better long-term market performance.
Challenges & Physical Constraints in Implementation
- High Initial Capital & Thermodynamic Payback Limits: Substantial upfront capital expenditure required for high-efficiency infrastructure—such as Organic Rankine Cycle (ORC) turbogenerators, recuperative burners, and multi-megawatt VFD installations—poses severe financial hurdles. Beyond capital costs, thermodynamic laws impose diminishing returns: as heat exchangers approach pinched temperature differences (\(\Delta T_{\text{pinch}} \lt 10\,\text{K}\)), surface area requirements scale asymptotically (\(A \propto 1/\Delta T_{\text{lm}}\)), leading to exponential equipment cost escalations for marginal exergy capture.
- Legacy Integration & Power Quality Distortion: Retrofitting modern power electronics into legacy factory infrastructures introduces severe electrical compatibility issues. High-frequency pulse-width modulated (PWM) switching from inverters injects total harmonic distortion (THD) into plant distribution grids, causing parasitic eddy-current heating in legacy transformers and dangerous common-mode voltages that cause electrical discharge machining (EDM) pitting inside motor bearings.
- Telemetry Infrastructure, Big Data Silos & Latency: High-frequency time-series telematics across thousands of sub-metered pneumatic, hydraulic, and electrical nodes frequently overwhelm industrial IT/OT architectures. Unsynchronized sampling rates between SCADA and cloud historians degrade machine learning accuracy, while network jitter prevents closed-loop edge Model Predictive Control from executing safety-critical power load shedding within deterministic millisecond windows.
- Workforce Competency & Cross-Disciplinary Silos: Optimizing resource efficiency requires bridging mechanical thermal engineering, electrical power electronics, chemical water treatment, and data science. Plant operators accustomed strictly to mechanical maintenance often lack training in configuring variable-frequency drive parameters, tuning PLC PID loops for variable flow, or interpreting multivariate anomaly flags, resulting in manual overrides that bypass energy-saving modes.
- Supply Chain Friction, Material Drift & Secondary Feedstock Limits: Transitioning to circular economy models introduces severe feedstock metallurgical and polymer variations. Secondary scrap aluminum alloys contain tramp iron and silicon contaminants that alter melt fluidity, elevate porosity, and degrade tensile ductility during die-casting. Enforcing traceability across Tier-2 and Tier-3 suppliers requires rigorous chemical spectroscopy, increasing incoming quality control inspection lead times.
Future Trends in Energy and Resource Efficiency
- Net-Zero Manufacturing & Electrified Process Heat: Achieving carbon neutrality requires industrial electrification, replacing natural gas-fired boilers with high-temperature industrial heat pumps and plasma torches capable of delivering process temperatures above \(200^\circ\text{C}\). Facilities are integrating multi-carrier thermal microgrids coupled with on-site hydrogen production to eliminate combustion-based Scope 1 direct emissions entirely.
- Autonomous Circularity & AI-Driven Disassembly: Robotic workcells equipped with multi-spectral computer vision and tactile feedback are automating the non-destructive disassembly of end-of-life battery packs and electric vehicle drivetrains. Direct closed-loop recycling processes sort, decontaminate, and remelt high-entropy alloys with near-zero yield loss, minimizing virgin mineral extraction dependencies.
- AI-Driven Energy Orchestration & Grid-Interactive Manufacturing: Factories are shifting from passive energy consumers to dynamic, grid-interactive flexible loads. Machine learning algorithms analyze dynamic day-ahead and real-time spot electricity pricing, automatically modulating energy-intensive batch sintering, cryogenic air separation, and water pumping schedules to provide synthetic inertia and frequency regulation services back to regional power grids.
- Standardized Digital Product Passports (DPP): International regulatory mandates (such as the EU Ecodesign Directive) are accelerating the adoption of blockchain-verified Digital Product Passports. These cryptographic ledgers track the embodied carbon footprint, recycled material fraction, and chemical hazardous substance declarations from raw extraction through final assembly, ensuring auditability across supply chains.
- Microgrids, Thermal Energy Storage & Exergy Cascading: Next-generation manufacturing campuses deploy on-site microgrids integrating solid-state batteries, molten salt or phase-change thermal storage (TES), and rooftop solar photovoltaics. Industrial parks apply exergy cascading—routing high-temperature exhaust from metallurgy furnaces through medium-pressure steam turbines, followed by low-grade district heating for administrative facilities—approaching thermodynamic Second Law limits.
Why Study Energy and Resource Efficiency in Manufacturing
Reducing Environmental Footprints
Energy and resource efficiency aims to minimize waste, emissions, and resource use. Students learn how to measure and reduce the environmental impacts of production. This supports global goals for climate action and sustainability.
Process Optimization and Cleaner Production
Students explore methods like lean manufacturing, process integration, and energy audits. These tools identify inefficiencies and opportunities for savings. This improves both environmental and economic performance.
Designing for Sustainability
Sustainable manufacturing starts at the design stage. Students learn how to select materials and processes that require less energy and create less waste. This supports life-cycle thinking and green innovation.
Measuring Efficiency and Performance
The course introduces key metrics such as energy intensity, yield ratios, and carbon footprint. Students use data to track improvements and guide decisions. These insights drive accountability and continuous improvement.
Policy, Standards, and Global Impact
Students study regulations, certifications, and sustainability reporting standards. They learn how to align industrial practices with international frameworks. This prepares them for leadership roles in sustainable manufacturing.
Energy and Resource Efficiency: Conclusion
Energy and resource efficiency in manufacturing is critical for fostering sustainability, reducing costs, and meeting global environmental challenges. As industries confront rising energy prices, resource scarcity, and increasingly stringent environmental regulations, efficiency becomes more than a best practice—it becomes a necessity. By adopting advanced technologies such as AI-driven analytics, digital twins, and IoT-based monitoring, companies can transform data into actionable insights that drive continuous improvement and smarter resource management.
Integrating renewable energy sources like solar, wind, and biomass helps decarbonize operations and contributes to climate targets, while innovations in water recycling, material optimization, and waste heat recovery enhance operational resilience. Promoting sustainable practices not only benefits the environment but also improves brand reputation and customer trust, especially as consumers increasingly favor eco-friendly companies.
Furthermore, global initiatives and policies such as the European Green Deal and the UN’s Sustainable Development Goals are accelerating the transition toward greener industrial models. Resources such as the International Energy Agency's Energy Efficiency hub provide valuable guidance and benchmarking tools for organizations looking to scale up their efforts.
As global priorities shift toward sustainability and circular economy principles, energy and resource efficiency will remain a key driver of innovation, competitiveness, and long-term resilience in manufacturing and other industrial processes. Embracing this transformation positions industries to thrive in a future that values not only economic performance but also environmental stewardship and social responsibility.
Energy and Resource Efficiency in Manufacturing: Frequently Asked Questions
This FAQ summarises how factories can use less energy and fewer resources while still meeting production and quality targets.
1. What is energy efficiency in manufacturing?
2. How is resource efficiency different from energy efficiency?
3. What are common strategies to improve energy efficiency in factories?
4. How does resource efficiency support sustainable manufacturing?
5. What is an Energy Management System (EMS)?
6. Which technologies drive energy and resource efficiency today?
7. How can lean manufacturing and efficiency initiatives work together?
8. What challenges arise when improving energy and resource efficiency?
9. How do digitalization and automation support efficiency?
10. Why are employee training and engagement so important?
Practice Modules & End-of-Page Exercises
Module 1: Fundamental Concept Review Questions
1. What is energy efficiency in the context of manufacturing, and why is it important?
2. How does resource efficiency differ from energy efficiency in manufacturing?
3. What are the primary technical strategies for improving energy efficiency in factories?
4. How does resource efficiency contribute directly to sustainable manufacturing?
5. What role do Energy Management Systems (EMS) play in plant operations?
6. What modern technologies are driving industrial energy and resource efficiency?
7. How can lean manufacturing tools be combined with resource efficiency goals?
8. What common organizational and financial barriers impede efficiency projects?
9. How do digitalization and smart automation enhance plant energy performance?
10. Why is workforce engagement vital for sustaining energy reduction targets?
11. What is the purpose of an industrial energy audit?
12. How does waste heat recovery improve total boiler or furnace efficiency?
Module 2: Analytical & Scenario-Based Inquiry
1. How does energy and resource efficiency in manufacturing contribute to overall business sustainability and long-term economic resilience?
2. What are the most effective technological interventions for waste heat recovery in thermal processing plants?
3. How can manufacturers measure and benchmark energy performance using standard metrics?
4. What are the primary environmental consequences of unmitigated industrial energy and resource waste?
5. How can Lean tools like 5S and Total Productive Maintenance (TPM) be applied to eliminate electrical and compressed air leaks?
6. What strategic solutions can overcome the high initial capital investment required for facility-wide energy retrofits?
7. How do Digital Twin simulation platforms enable dynamic load balancing across smart manufacturing facilities?
8. How can organizations cultivate an active shop-floor culture focused on energy and material conservation?
9. How does ISO 50001 implementation establish a structured framework for continuous energy improvement?
10. How can industrial facilities implement closed-loop process water recycling without risking chemical contamination?
11. How does circular economy integration transform conventional linear manufacturing waste into valuable production inputs?
12. How do collapsible assessment modules reinforce student understanding of quantitative efficiency metrics?
Interactive Review 1: What is the primary operational advantage of installing Variable Frequency Drives (VFDs) on centrifugal pumps?
Interactive Review 2: How does a recuperative heat exchanger improve natural gas furnace efficiency?
Interactive Review 3: Why is Specific Energy Consumption (SEC) preferred over absolute total energy consumption for plant benchmarking?
Module 3: Quantitative & Applied Engineering Calculations
Work through these step-by-step mathematical calculations evaluating motor power demand, waste heat recovery efficiency, compressed air leak costs, and Specific Energy Consumption (\(\text{SEC}\)).
Problem 1: Specific Energy Consumption (SEC) and Production Efficiency Calculation
Problem Statement: An aluminum die-casting plant processes raw ingot into automotive engine blocks. Over a 30-day operational month, the facility consumed \(450{,}000\,\text{kWh}\) of electricity and \(2{,}100{,}000\,\text{MJ}\) of natural gas while producing \(12{,}500\) finished engine blocks. Convert all energy consumption into Gigajoules (\(\text{GJ}\)) and calculate the Specific Energy Consumption (\(\text{SEC}\)) in \(\text{GJ/unit}\).
Step 1: Electrical Energy Conversion
Using the conversion factor \(1\,\text{kWh} = 0.0036\,\text{GJ}\):
$$E_{\text{elec}} = 450{,}000\,\text{kWh} \times 0.0036\,\frac{\text{GJ}}{\text{kWh}} = \mathbf{1{,}620\,\text{GJ}}$$
Step 2: Natural Gas Thermal Energy Conversion
Using the conversion factor \(1\,\text{GJ} = 1{,}000\,\text{MJ}\):
$$E_{\text{gas}} = \frac{2{,}100{,}000\,\text{MJ}}{1{,}000\,\text{MJ/GJ}} = \mathbf{2{,}100\,\text{GJ}}$$
Step 3: Total Primary Energy Aggregation
$$E_{\text{total}} = E_{\text{elec}} + E_{\text{gas}} = 1{,}620\,\text{GJ} + 2{,}100\,\text{GJ} = \mathbf{3{,}720\,\text{GJ}}$$
Step 4: Specific Energy Consumption (SEC) Evaluation
$$\text{SEC} = \frac{E_{\text{total}}}{N_{\text{units}}} = \frac{3{,}720\,\text{GJ}}{12{,}500\,\text{units}} = \mathbf{0.2976\,\text{GJ/Unit}} \quad (297.6\,\text{MJ/Unit})$$
Engineering Interpretation: The plant operates with a thermal-dominated energy split (\(56.5\%\) gas vs. \(43.5\%\) electric). This establishes an official baseline \(\text{EnB}\) under ISO 50001; thermal insulation retrofits on holding furnaces will yield the highest primary energy abatement.
Problem 2: Waste Heat Recovery Economizer Heat Transfer Calculation
Problem Statement: An industrial boiler exhausts \(4.5\,\text{kg/s}\) of flue gas at \(T_{g,1} = 280^\circ\text{C}\). An economizer captures waste sensible heat to preheat incoming boiler feedwater from \(T_{w,1} = 20^\circ\text{C}\) to \(T_{w,2} = 85^\circ\text{C}\). Given \(c_{p,w} = 4.18\,\text{kJ/(kg}\cdot\text{K)}\), water flow \(\dot{m}_w = 2.0\,\text{kg/s}\), and flue gas specific heat \(c_{p,g} = 1.05\,\text{kJ/(kg}\cdot\text{K)}\), calculate the heat recovery rate \(\dot{Q}\) in \(\text{kW}\) and the flue gas exit temperature \(T_{g,2}\), assuming zero shell losses.
Step 1: Water Stream Heat Absorption
$$\Delta T_w = 85 - 20 = 65\,\text{K}$$
$$\dot{Q} = \dot{m}_w \cdot c_{p,w} \cdot \Delta T_w = 2.0\,\frac{\text{kg}}{\text{s}} \times 4.18\,\frac{\text{kJ}}{\text{kg}\cdot\text{K}} \times 65\,\text{K} = \mathbf{543.4\,\text{kW}}$$
Step 2: Flue Gas Energy Balance
By First Law energy conservation (\(\dot{Q}_{\text{absorbed}} = \dot{Q}_{\text{released}}\)):
$$\dot{Q} = \dot{m}_g \cdot c_{p,g} \cdot (T_{g,1} - T_{g,2})$$
$$543.4\,\text{kW} = 4.5\,\frac{\text{kg}}{\text{s}} \times 1.05\,\frac{\text{kJ}}{\text{kg}\cdot\text{K}} \times (280 - T_{g,2}) = 4.725 \cdot (280 - T_{g,2})$$
Step 3: Flue Gas Exhaust Temperature Isolation
$$280 - T_{g,2} = \frac{543.4}{4.725} \approx 115.00^\circ\text{C}$$
$$T_{g,2} = 280 - 115.00 = \mathbf{165.00^\circ\text{C}}$$
Engineering Interpretation: The exit temperature of \(165^\circ\text{C}\) safely exceeds the typical acid dew point for natural gas/light fuel oil flue gases (\(\approx 120\text{--}130^\circ\text{C}\)), avoiding sulfuric acid condensation corrosion while recovering \(543.4\,\text{kW}\) of high-grade process heat.
Problem 3: Variable Frequency Drive (VFD) Energy Savings Calculation
Problem Statement: A \(75\,\text{kW}\) nameplate electric motor driving an industrial cooling water pump runs \(6{,}000\,\text{hours/year}\) at full speed, drawing \(P_1 = 70.0\,\text{kW}\). Installing a VFD allows average pump speed to be modulated down to \(80\%\) (\(N_2/N_1 = 0.80\)). Applying Affinity Laws (\(P \propto N^3\)), determine the operating power \(P_2\), annual electrical energy reduction in \(\text{kWh}\), and financial savings at \(\$0.12/\text{kWh}\).
Step 1: Affinity Scaling Power Evaluation
$$P_2 = P_1 \left(\frac{N_2}{N_1}\right)^3 = 70.0\,\text{kW} \times (0.80)^3 = 70.0 \times 0.512 = \mathbf{35.84\,\text{kW}}$$
Step 2: Instantaneous Power Delta
$$\Delta P = P_1 - P_2 = 70.0\,\text{kW} - 35.84\,\text{kW} = \mathbf{34.16\,\text{kW}}$$
Step 3: Annualized Energy Reduction
$$E_{\text{saved}} = \Delta P \times t_{\text{annual}} = 34.16\,\text{kW} \times 6{,}000\,\text{h} = \mathbf{204{,}960\,\text{kWh/year}}$$
Step 4: Utility Cost Savings Calculation
$$\text{Savings} = 204{,}960\,\text{kWh} \times \$0.12/\text{kWh} = \mathbf{\$24{,}595.20/\text{year}}$$
Engineering Interpretation: A \(20\%\) reduction in speed yields a \(48.8\%\) drop in electrical demand. Given that a standard \(75\,\text{kW}\) industrial inverter retrofit costs approximately \(\$8{,}000\text{--}\$12{,}000\) installed, the simple payback period is under 6 months.
Problem 4: Compressed Air Leakage Energy & Cost Analysis
Problem Statement: An ultrasonic leak audit of a plant pneumatic network at \(7.0\,\text{bar}\) reveals \(15\) equivalent \(1.5\,\text{mm}\) orifice leaks. A single \(1.5\,\text{mm}\) leak at \(7\,\text{bar}\) loses \(0.20\,\text{m}^3/\text{min}\) of free air. The plant rotary screw compressor consumes \(6.0\,\text{kW}\) of electrical power per \(1.0\,\text{m}^3/\text{min}\) delivered. Operating on \(8{,}000\,\text{hours/year}\) at \(\$0.10/\text{kWh}\), determine the total volumetric loss rate, electrical power wasted, annual energy loss, and monetary cost.
Step 1: Total Volumetric Air Leakage Rate
$$\dot{V}_{\text{waste}} = 15 \times 0.20\,\frac{\text{m}^3}{\text{min}} = \mathbf{3.0\,\text{m}^3/\text{min}}$$
Step 2: Continuous Compressor Power Penalty
$$P_{\text{waste}} = 3.0\,\frac{\text{m}^3}{\text{min}} \times 6.0\,\frac{\text{kW}}{\text{m}^3/\text{min}} = \mathbf{18.0\,\text{kW}}$$
Step 3: Annualized Electrical Consumption Penalty
$$E_{\text{waste}} = 18.0\,\text{kW} \times 8{,}000\,\text{h} = \mathbf{144{,}000\,\text{kWh/year}}$$
Step 4: Financial Loss Calculation
$$\text{Cost} = 144{,}000\,\text{kWh} \times \$0.10/\text{kWh} = \mathbf{\$14{,}400.00/\text{year}}$$
Engineering Interpretation: Compressed air is one of the most expensive factory utilities, operating at an overall mechanical-to-pneumatic efficiency of only \(\sim 10\text{--}15\%\). Sealing leaks via routine TPM represents an immediate zero-capital operational savings intervention.
Problem 5: Closed-Loop Process Water Recycling & Make-Up Volume Savings
Problem Statement: An electroplating rinse line draws \(50.0\,\text{m}^3/\text{h}\) of municipal water on a once-through open drain. The facility retrofits a multi-stage membrane filtration and RO recycling loop achieving a \(90\%\) water recovery efficiency. Fresh water supply costs \(\$2.50/\text{m}^3\), while industrial sewer discharge fees are \(\$1.80/\text{m}^3\). For an operational schedule of \(4{,}000\,\text{hours/year}\), calculate the make-up water demand, hourly savings, and annual utility cost reduction.
Step 1: Volumetric Balance & Make-Up Demand
$$\dot{V}_{\text{recycled}} = 50.0\,\frac{\text{m}^3}{\text{h}} \times 0.90 = 45.0\,\text{m}^3/\text{h}$$
$$\dot{V}_{\text{makeup}} = 50.0 - 45.0 = \mathbf{5.0\,\text{m}^3/\text{h}}$$
Step 2: Combined Water Volumetric Tariff
$$C_{\text{tariff}} = \$2.50 + \$1.80 = \$4.30/\text{m}^3$$
Step 3: Hourly Expenditure Comparison
$$\text{Cost}_{\text{baseline}} = 50.0\,\frac{\text{m}^3}{\text{h}} \times \$4.30 = \$215.00/\text{h}$$
$$\text{Cost}_{\text{retrofit}} = 5.0\,\frac{\text{m}^3}{\text{h}} \times \$4.30 = \$21.50/\text{h}$$
$$\Delta \text{Cost}_{\text{hourly}} = \$215.00 - \$21.50 = \mathbf{\$193.50/\text{h}}$$
Step 4: Annual Economic Savings
$$\text{Savings}_{\text{annual}} = \$193.50/\text{h} \times 4{,}000\,\text{h} = \mathbf{\$774{,}000.00/\text{year}}$$
Engineering Interpretation: In addition to saving \(180{,}000\,\text{m}^3\) of municipal freshwater annually, the reduction in discharge volume significantly mitigates compliance liability associated with local environmental effluent discharge limits.
Problem 6: Solar Photovoltaic (PV) Industrial Rooftop Decarbonization Assessment
Problem Statement: A textile manufacturing campus installs a \(500\,\text{kWp}\) monocrystalline rooftop solar PV system. The site receives an average of \(4.5\) peak sun hours per day. The regional grid emission intensity factor is \(0.65\,\text{kg CO}_2/\text{kWh}\). Determine total annual electricity yield in \(\text{kWh}\) and the net annual greenhouse gas abatement in metric tons of carbon dioxide (\(\text{tCO}_2/\text{year}\)).
Step 1: Daily Electrical Energy Yield
$$E_{\text{daily}} = 500\,\text{kWp} \times 4.5\,\frac{\text{h}}{\text{day}} = \mathbf{2{,}250\,\text{kWh/day}}$$
Step 2: Annualized Generation (365-Day Cycle)
$$E_{\text{annual}} = 2{,}250\,\frac{\text{kWh}}{\text{day}} \times 365\,\text{days} = \mathbf{821{,}250\,\text{kWh/year}}$$
Step 3: Greenhouse Gas Emissions Abatement
$$\text{Mass}_{\text{CO}_2} = 821{,}250\,\text{kWh} \times 0.65\,\frac{\text{kg CO}_2}{\text{kWh}} = 533{,}812.5\,\text{kg CO}_2$$
$$\text{Abatement} = \frac{533{,}812.5\,\text{kg}}{1{,}000\,\text{kg/ton}} = \mathbf{533.81\,\text{tCO}_2/\text{year}}$$
Engineering Interpretation: The system offsets over \(530\,\text{metric tons}\) of Scope 2 indirect emissions annually while hedging against peak diurnal electricity spot pricing tariffs.
Problem 7: Material Scrap Reduction & Additive Manufacturing Yield Optimization
Problem Statement: An aerospace structural bracket is evaluated for CNC subtractive milling versus Direct Metal Laser Sintering (DMLS) 3D printing. CNC milling machines a \(12.0\,\text{kg}\) titanium (Ti-6Al-4V) billet down to a \(1.5\,\text{kg}\) finished geometry (swarf scrap credit recovered at \(20\%\) of initial purchase price). DMLS uses \(1.8\,\text{kg}\) of spherical powder to produce the identical \(1.5\,\text{kg}\) part (unmelted powder sieved and reused). Raw billet costs \(\$80.00/\text{kg}\), CNC scrap credit is \(\$10.00/\text{kg}\), and gas-atomized powder costs \(\$120.00/\text{kg}\). Compute the net material cost per part for both routes and the net savings per bracket.
Step 1: Subtractive CNC Milling Net Material Expenditure
$$\text{Cost}_{\text{billet}} = 12.0\,\text{kg} \times \$80.00/\text{kg} = \$960.00$$
$$M_{\text{scrap}} = 12.0 - 1.5 = 10.5\,\text{kg}$$
$$\text{Credit}_{\text{scrap}} = 10.5\,\text{kg} \times \$10.00/\text{kg} = \$105.00$$
$$\text{Net CNC Cost} = \$960.00 - \$105.00 = \mathbf{\$855.00/\text{part}}$$
Step 2: Additive Manufacturing (DMLS) Material Expenditure
$$\text{Net DMLS Cost} = 1.8\,\text{kg} \times \$120.00/\text{kg} = \mathbf{\$216.00/\text{part}}$$
Step 3: Differential Material Cost Savings
$$\Delta \text{Cost} = \$855.00 - \$216.00 = \mathbf{\$639.00/\text{bracket}}$$
$$\text{Reduction Percentage} = \frac{\$639.00}{\$855.00} \times 100\% = \mathbf{74.74\%}$$
Engineering Interpretation: Additive manufacturing shifts the Buy-to-Fly ratio from \(8:1\) to \(1.2:1\). For high-cost, energy-intensive reactive metals like titanium, near-net-shape additive manufacturing saves substantial raw material and upstream extraction energy.