
Ergonomics is often mistaken for “comfort,” but its real subject is dignity: designing work and technology so people are not quietly punished by the tools they must use every day. This diagram captures how that sensibility is taught. The inputs—research literature and workplace case studies—bring both the science and the lived stories: what injuries repeat, what errors recur, what designs fail people in predictable ways. The controls—standards and evaluation criteria—keep the learning grounded, so students do not rely on taste or intuition alone, but learn to justify decisions with measurable reasoning. Within the central function, learners practice seeing the invisible: workload, attention, posture, reach, fatigue, signage clarity, interface friction—small mismatches that accumulate into risk. The mechanisms—ergonomic tools and simulation exercises—turn observation into action, giving students a way to measure, model, and redesign instead of merely “noticing.” And the outputs are practical: trained students who can translate human needs into design requirements, and workplaces that are safer, clearer, and more humane—where efficiency and well-being stop competing and begin cooperating.
- Biomechanical Static Equilibrium & Spine Kinetics: Rigorous modeling of \(L_5/S_1\) lumbar compression forces using moment balances, evaluating spinal load limits against the NIOSH \(3{,}400\,\text{N}\) action threshold.
- Quantitative Lifting Index Formulations: Multi-variable multiplicative derivation of Recommended Weight Limits (\(\text{RWL}\)) incorporating horizontal reach, vertical displacement, asymmetry, and frequency multipliers.
- Industry 5.0 & Human-in-the-Loop AI: Integrating Digital Human Modeling (DHM), wearable IMU-based kinematic state estimation, and cobot admittance control to dynamically mitigate musculoskeletal fatigue.
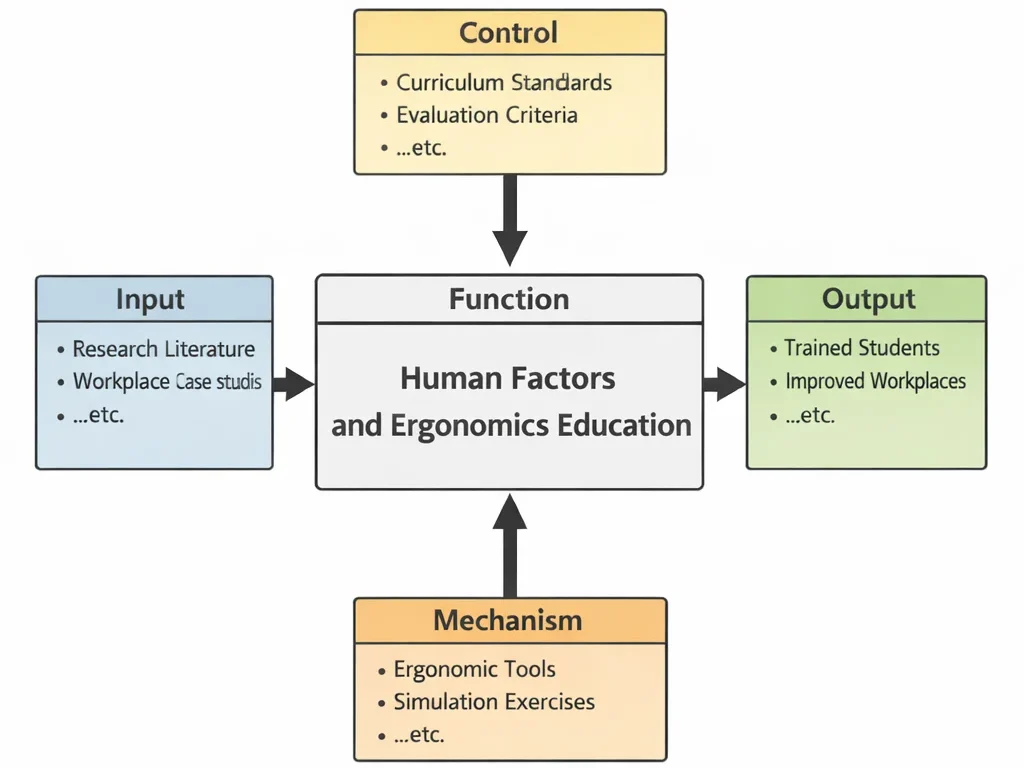
This IDEF0 (Input–Control–Output–Mechanism) diagram summarizes Human Factors and Ergonomics Education as a structured process. Inputs on the left—research literature and workplace case studies—provide the evidence base and practical context. Controls at the top—curriculum standards and evaluation criteria—set the learning scope and define how competence is assessed. In the center, the function (Human Factors and Ergonomics Education) transforms evidence and standards into teachable methods for analyzing human capabilities, limitations, and work-system design. Outputs on the right—trained students and improved workplaces—represent the intended educational results, including safer, more efficient, and more user-friendly environments. Mechanisms at the bottom—ergonomic tools and simulation exercises—support hands-on practice, allowing learners to test designs, evaluate risks, and refine solutions in realistic scenarios.
In the age of automation and advanced manufacturing systems, understanding human factors and ergonomics in manufacturing has never been more critical. This field focuses on optimizing the interaction between humans and machines to improve safety, productivity, and overall well-being in industrial settings. Rooted in the broader scope of Industrial and Manufacturing Technologies, ergonomic design and analysis enhance both workforce performance and technological efficiency.
Modern factories that embrace Smart Manufacturing and Industry 4.0 rely on data-driven insights to tailor machine interfaces and workflows to human capabilities. Coupled with Computer-Integrated Manufacturing (CIM) systems, these ergonomic enhancements reduce fatigue, errors, and accidents, making production processes more resilient and adaptive. The incorporation of Digital Twin Technology enables engineers to simulate human-machine interactions before implementation, identifying ergonomic risks and improving workplace design.
Ergonomics also plays a key role in Lean Manufacturing by streamlining operations through user-centered task design. As manufacturing shifts toward Additive Manufacturing (3D Printing) and Advanced Materials and Manufacturing Technologies, new ergonomic considerations emerge related to workstation layout, repetitive movement, and user interface design. A focus on Manufacturing Quality Control and Assurance is closely linked, as ergonomic failures can lead to inconsistencies and safety incidents.
Incorporating human factors principles into Industrial Automation and Robotics improves usability and collaboration between humans and robotic systems. Wearable technology, sensor feedback, and intuitive control systems bridge the gap between traditional labor and machine intelligence. The drive for Energy and Resource Efficiency in Manufacturing further underscores the need to reduce unnecessary physical strain and motion, minimizing both worker fatigue and wasted effort.
At the systems level, ergonomic thinking influences strategic decisions in Supply Chain Management and Sustainable Manufacturing. From packaging ergonomics to transport logistics, human-centered design supports efficient movement of goods while reducing injury risks. These considerations are aligned with the physical and organizational infrastructure developed in fields like Mechanical Engineering and its applications in Manufacturing and Production Engineering.
Ergonomics research draws upon multiple physical sciences. Concepts from Thermodynamics and Heat Transfer, Fluid Mechanics and Hydraulics, and Solid Mechanics support the design of thermal environments, tools, and posture-supporting devices. Innovations in Nanotechnology and Advanced Materials in Mech Eng are also contributing to ergonomic progress, offering lighter, more adaptive equipment and materials.
Whether applied in Automotive Engineering, Biomechanical Engineering, or Robotics and Automation in Mech Eng, the central aim remains the same: harmonizing the strengths of human operators with the capabilities of machines. Through effective Control Systems in Mech Engineering and thoughtful design using Mechanical Design and CAD, engineers can ensure that humans remain at the core of innovation and manufacturing excellence.

Human-Centred Manufacturing: Ergonomics, Safety, and Workforce Performance
Navigate through the core topics of Industrial & Manufacturing Technologies to see how human factors and ergonomics interacts across different manufacturing domains:
Industrial & Manufacturing Overview
Connects human interaction with technological systems across industrial environments, establishing the macro foundational context for human factors integration.
Human Factors & Ergonomics (Current)
Designs systems that enhance worker safety, comfort, and workforce productivity directly within modern manufacturing environments.
Automation & Robotics
Balances physical human–machine interaction and safety protocols in hybrid automated production cells and cobot workcells.
Smart Manufacturing
Integrates human decision-making roles into highly intelligent, sensor-driven, and connected Industry 4.0 production networks.
Process Design
Engineers operational sequences and physical layouts directly aligned with human physical capabilities and cognitive limits.
Quality Control
Reduces human inspection errors and strain-induced oversight to optimize quality inspection reliability.
Lean Manufacturing
Eliminates physical waste and unnecessary motion to streamline overall process flow while cutting fatigue.
Supply Chain
Enhances human physical performance, safety, and throughput across distribution logistics and manual material handling networks.
Sustainable Manufacturing
Promotes long-term workforce sustainability, occupational health, and safe working conditions alongside environmental goals.
Energy & Resource Efficiency
Aligns ergonomic human movement with energy-efficient manual and machine operational routines.
CIM
Integrates software interfaces and human control checkpoints smoothly into digital shopfloor control systems.
Additive Manufacturing
Addresses specialized ergonomic task demands, powder handling safety, and post-processing workstation design.
Advanced Materials
Navigates human interaction challenges associated with processing novel composites and advanced reactive materials.
Digital Twin
Simulates physical biomechanics and human-system interactions virtually to optimize safety before physical tooling setup.
Core Principles of Human Factors and Ergonomics
Worker-Centered Design
- Definition: Adapting tools, machines, and processes to fit human capabilities and limitations.
- Key Elements:
- Ensuring tasks match workers’ physical, cognitive, and sensory abilities.
- Designing systems to reduce error and enhance ease of use.
- Promoting inclusive design to accommodate diverse populations, including those with disabilities or varying levels of expertise.
- Incorporating feedback from users during iterative design phases to continuously refine usability.
- Implementing safety features that align with natural human reflexes and responses.
Task Analysis
- Definition: Breaking down tasks into their individual components to identify potential risks or inefficiencies.
- Applications:
- Evaluating physical demands, cognitive load, and environmental factors.
- Designing processes to streamline tasks and reduce complexity.
- Creating training programs tailored to task-specific skills and risk areas.
- Developing standard operating procedures that align with real-world practices.
- Incorporating time-motion studies to optimize workflow and reduce idle time.
Physical Ergonomics
- Definition: Focuses on the physical interaction between workers and their environment, including posture, force, and movement.
- Key Considerations:
- Designing tools and workstations to prevent repetitive strain injuries (RSIs).
- Adjusting workstation heights and seating to reduce awkward postures.
- Ensuring lighting, temperature, and noise levels are within comfort and safety thresholds.
- Providing adjustable equipment and personal protective gear for individual needs.
- Conducting ergonomic risk assessments regularly to prevent musculoskeletal disorders.
Cognitive Ergonomics
- Definition: Focuses on mental processes such as perception, memory, and decision-making in work environments.
- Key Considerations:
- Reducing cognitive overload by simplifying machine interfaces.
- Designing displays and controls for intuitive use.
- Incorporating error-tolerant design to prevent critical mistakes.
- Using color coding, icons, and auditory signals to reinforce information recognition.
- Aligning information flow with human attention spans and multitasking limitations.
Organizational Ergonomics
- Definition: Examines how organizational structures and workflows influence human performance and well-being.
- Key Considerations:
- Improving communication and collaboration between workers.
- Designing shift schedules to reduce fatigue.
- Developing job roles and responsibilities that prevent burnout and overwork.
- Implementing ergonomic policies within human resource practices and corporate culture.
- Encouraging employee participation in decision-making to improve morale and ownership.
For deeper insights into workplace ergonomics research and standards, resources such as the Human Factors and Ergonomics Society (HFES) provide valuable guidance and publications for professionals and organizations alike.
Contemporary Biomechanical Modeling & Cognitive Computation Paradigms
Modern ergonomics has evolved from static observational checklists to dynamic, sensor-integrated biomechanical and cognitive computation. By fusing inverse dynamics, artificial intelligence, and real-time kinematic telemetry, manufacturing engineers quantify joint torques and cognitive friction with sub-second temporal resolution.
Dynamic Biomechanical Inversion & Musculoskeletal Neural Operators
Classical static equilibrium models fail to account for inertial accelerations (\(m\mathbf{a}\)) during rapid industrial picking. Contemporary ergonomic platforms integrate 3D segment kinematics to compute dynamic \(L_5/S_1\) joint moments through continuous inverse dynamics:
$$\mathbf{M}_{\text{joint}} = \sum_{i=1}^n \left( \mathbf{r}_i \times m_i (\mathbf{g} - \ddot{\mathbf{x}}_i) - \mathbf{I}_i \boldsymbol{\alpha}_i - \boldsymbol{\omega}_i \times (\mathbf{I}_i \boldsymbol{\omega}_i) \right) + \mathbf{r}_{\text{load}} \times \mathbf{F}_{\text{ext}}$$
Where \(\mathbf{I}_i\) is the segment inertia tensor, \(\boldsymbol{\omega}_i\) and \(\boldsymbol{\alpha}_i\) are angular velocity and acceleration vectors, and \(\mathbf{F}_{\text{ext}}\) is the external load vector. To bypass computationally expensive musculoskeletal simulations in real time, Fourier Neural Operators (FNOs) and DeepONets learn the mapping from sparse wearable IMU acceleration streams directly to individual muscle fascicle strain rates and spinal disc shear forces, allowing instantaneous posture correction feedback without tethered laboratory motion capture.
Human-Cobot Admittance Control & Adaptive Ergonomic Digital Twins
Collaborative robotics (cobots) optimize ergonomics by taking over physical loads while humans guide precision manipulation. Adaptive admittance controllers dynamically adjust robot compliance based on the operator's measured fatigue levels:
$$\mathbf{M}_d (\ddot{\mathbf{x}}_c - \ddot{\mathbf{x}}_d) + \mathbf{D}_d(t) (\dot{\mathbf{x}}_c - \dot{\mathbf{x}}_d) + \mathbf{K}_d (\mathbf{x}_c - \mathbf{x}_d) = \mathbf{F}_{\text{human}}$$
Here, the damping matrix \(\mathbf{D}_d(t)\) is modulated continuously via machine learning algorithms monitoring operator heart rate variability (HRV) and surface electromyography (sEMG) signals. When muscular fatigue thresholds are exceeded, the cobot autonomously stiffens and absorbs a higher fraction of gravitational and inertial torques, preserving human stamina and eliminating repetitive strain injuries.
Systems Engineering Trade-Off Matrix: Ergonomic Interventions in Manufacturing
Ergonomic workplace design requires managing multi-variable compromises among biomechanical relief, cycle time, capital expenditure, and cognitive complexity:
| Ergonomic Intervention | Primary Biomechanical Benefit | Operational / Ergonomic Risk | Engineering Mitigation |
|---|---|---|---|
| Passive Upper-Limb Exoskeletons | Transfers deltoid and rotator cuff loads during sustained overhead work (\(\gt 90^\circ\) arm elevation) to the pelvis. | Thermal discomfort, localized soft tissue contact pressure, altered trunk kinematics causing compensatory lumbar hyperextension. | Deploy breathable composite textiles; calibrate gas-spring assist profiles to match specific tool weights; enforce duty cycle limits. |
| Collaborative Robots (Cobots) in Assembly | Eliminates heavy lifting (\(\gt 15\,\text{kg}\)) and awkward reach maneuvers during engine block and chassis mating. | Increased cycle time due to safety-mandated speed limitations (\(v \le 250\,\text{mm/s}\)); potential operator boredom or complacency. | Implement speed-and-separation monitoring (SSM) radar zones allowing full robot velocity when human distance exceeds clearance thresholds. |
| Sit-Stand Workstations & Height Adjustability | Enables postural variation, mitigating venous pooling in lower extremities and static spinal disc creep. | Operators fail to utilize adjustment mechanisms (behavioral inertia); poor cable management poses trip hazards during transition. | Install automated memory presets linked to RFID operator badges; integrate enclosed articulated cable carriers. |
| Augmented Reality (AR) Smart Visors | Eliminates neck flexion by projecting pick-and-place instructions and wire schematics directly onto the line of sight. | Visual fatigue, vergence-accommodation conflict, device head-weight moment increasing cervical spine shear force. | Limit continuous AR utilization to 45-minute blocks; utilize ultra-lightweight waveguide optics with counterbalanced battery packs. |
Key Areas of Application of Human Factors and Ergonomics in Manufacturing
Workstation Design
- Principles:
- Arrange tools and materials within easy reach to minimize unnecessary movements.
- Adjust workstation height to accommodate various worker sizes.
- Incorporate modular setups to allow personalization for specific tasks.
- Ensure line of sight for visual tasks to minimize neck strain and eye fatigue.
- Account for left- and right-handed users when arranging tools and interfaces.
- Techniques:
- Use ergonomic chairs and adjustable desks.
- Implement anti-fatigue mats for standing workstations.
- Provide footrests and adjustable lighting to support various working positions.
- Introduce sit-stand desks to allow posture variation during long shifts.
- Benefits:
- Reduces musculoskeletal disorders (MSDs).
- Enhances comfort and efficiency.
- Promotes job satisfaction and reduces absenteeism due to physical discomfort.
Tool and Equipment Design
- Principles:
- Design tools with handles that fit the human grip to reduce strain.
- Minimize tool vibrations and weight to prevent fatigue.
- Ensure intuitive tool interfaces that align with user expectations.
- Incorporate safety locks and guards into tool designs.
- Applications:
- Power tools with anti-vibration features.
- Equipment with adjustable controls for different users.
- Tools with color-coded indicators to signal operational status.
- Ergonomic grips on frequently used hand tools to reduce repetitive strain injuries.
Process and Workflow Optimization
- Principles:
- Eliminate unnecessary steps to reduce physical and mental fatigue.
- Use automation to handle repetitive or hazardous tasks.
- Apply Lean principles to remove inefficiencies and standardize procedures.
- Balance workloads across teams to minimize bottlenecks and overloads.
- Applications:
- Assembly lines with rotating tasks to prevent repetitive strain.
- Streamlined workflows to reduce worker movement.
- Workflow simulations using digital manufacturing models to test ergonomic improvements.
- Integration of real-time feedback systems to monitor workflow efficiency and worker strain.
Safety Systems
- Principles:
- Design systems that prioritize worker safety through hazard prevention and control.
- Incorporate fail-safes and intuitive emergency response mechanisms.
- Use predictive analytics to identify potential safety risks before they occur.
- Applications:
- Guardrails and safety interlocks on machinery.
- Warning systems for potential hazards.
- Wearable technology that monitors posture and alerts workers of unsafe positions.
- Vision-based safety systems that detect proximity breaches near dangerous machinery.
- Benefits:
- Reduces workplace accidents and injuries.
- Enhances compliance with occupational safety standards.
Training and Education
- Principles:
- Train workers to use equipment safely and efficiently.
- Educate managers on the importance of ergonomics in improving productivity.
- Utilize feedback loops to tailor training to actual user experiences.
- Foster a culture of continuous improvement in ergonomic practices.
- Applications:
- Simulation-based training for new machinery.
- Workshops on proper lifting techniques.
- Gamified safety modules to increase engagement and knowledge retention.
- Refresher courses for long-term employees on updated ergonomic standards.
Environmental Design
- Principles:
- Optimize lighting, temperature, and noise levels to support worker comfort and focus.
- Promote biophilic elements to enhance mental well-being and reduce stress.
- Ensure proper ventilation and air quality to prevent fatigue and headaches.
- Applications:
- Installing LED lighting to reduce glare and shadows.
- Using noise-canceling barriers in noisy manufacturing environments.
- Dynamic temperature zoning to cater to different physical workspaces.
- Use of natural daylight and green interior design elements to reduce eyestrain and enhance mood.
Tools and Technologies for Human Factors and Ergonomics in Manufacturing
Motion Capture Systems
- Role: Analyze worker movements to identify inefficiencies or potential injury risks; track real-time biomechanical patterns to assess ergonomic posture compliance.
- Applications:
- Improving assembly line workflows by identifying awkward or repetitive movements.
- Designing tools and equipment layouts that reduce stress on joints and muscles.
- Supporting rehabilitation strategies for injured workers by visualizing movement deviations.
- Benchmarking best practices across different production environments using motion pattern databases.
Digital Human Modeling (DHM)
- Role: Simulate human interactions with systems and environments to optimize ergonomic design; visualize anthropometric diversity and posture variability across tasks.
- Applications:
- Testing workstation designs for ergonomics before implementation.
- Analyzing the impact of repetitive motions on worker health and long-term fatigue.
- Creating virtual prototypes for inclusive design, accommodating various worker body types.
- Conducting ergonomic assessments for global manufacturing sites using shared DHM models.
Wearable Technology
- Role: Monitor physical activity, posture, and fatigue in real time to prevent injuries; track vital signs to detect early signs of exhaustion or stress in workers.
- Applications:
- Wearable sensors tracking improper lifting techniques in warehouses and production areas.
- Smart clothing monitoring worker fatigue and stress levels to support scheduling decisions.
- Real-time feedback devices alerting workers when their posture deviates from ergonomic guidelines.
- Data-driven dashboards enabling supervisors to identify high-risk zones and plan interventions.
Exoskeletons
- Role: Provide physical support to workers performing heavy or repetitive tasks to reduce musculoskeletal strain; distribute mechanical load away from vulnerable muscle groups.
- Applications:
- Reducing strain during lifting and carrying tasks in logistics and construction environments.
- Assisting in precision tasks that require extended holding positions, such as welding or assembly.
- Supporting rehabilitation for workers returning from injury by limiting load-bearing on affected areas.
- Boosting worker stamina and reducing injury-related absenteeism across shift cycles.
Augmented Reality (AR)
- Role: Enhance worker training and assist in complex tasks with visual guidance overlays; improve cognitive ergonomics by reducing memory burden and instruction recall errors.
- Applications:
- AR overlays providing step-by-step instructions for machine maintenance and troubleshooting.
- Training workers on new assembly techniques without halting production lines.
- Real-time error prevention through AR prompts that highlight incorrect procedures.
- Remote collaboration for expert ergonomists to guide on-site improvements via AR interfaces. Emerging solutions like PTC Vuforia are accelerating AR's role in industrial ergonomics.
IoT and Smart Sensors
- Role: Collect data on environmental conditions and worker interactions to support proactive ergonomic improvements; enable predictive alerts based on historical strain or motion patterns.
- Applications:
- Monitoring noise levels to ensure compliance with safety standards and reduce auditory fatigue.
- Tracking machine vibrations to identify ergonomic risks associated with prolonged exposure.
- Gathering environmental metrics like temperature, lighting, and humidity to improve overall comfort.
- Interlinking ergonomic data with production KPIs to correlate performance with well-being indicators.
Applications of Ergonomics in Industrial Systems
About This Interactive Simulator:
This interactive ergonomics calculator models biomechanical spine compression forces under the NIOSH manual lifting framework. Adjust load weight, horizontal reach distance, and vertical lift distance to evaluate ergonomic risk thresholds in real time.
- Solid Cyan Line: Calculated \(L_5/S_1\) spinal compression force (\(\text{N}\)) across varying load weights.
- Dashed Rose Line: NIOSH recommended action limit (\(3{,}400\,\text{N}\)), above which spinal disc injury risk rises sharply.
- Interactive Sliders: Dynamically alter load weight (\(5\text{--}40\,\text{kg}\)), horizontal reach (\(25\text{--}60\,\text{cm}\)), and vertical travel (\(0\text{--}100\,\text{cm}\)).
Interactive Ergonomic Lifting Risk Calculator
Benefits of Human Factors and Ergonomics in Manufacturing
- Enhanced Worker Safety: Reduces injuries caused by repetitive motions, awkward postures, or hazardous environments through better workstation layouts and task designs. Minimizes exposure to physical and environmental risks by integrating ergonomic principles in machine interface and workflow planning, incorporating proactive monitoring tools to detect early signs of strain before chronic microtrauma occurs.
- Increased Productivity: Optimized workflows and ergonomic designs minimize fatigue and maximize efficiency by reducing unnecessary movement and simplifying task sequences. Improved physical comfort leads to sustained energy and focus, boosting overall task output per hour while enhanced cognitive ergonomics support better decision-making and reduce time lost due to interface confusion or errors.
- Improved Job Satisfaction: Comfortable work environments and user-friendly tools increase employee morale, leading to higher engagement and motivation. Empowered workers feel more in control and experience reduced stress, especially when they can customize their workspace to suit individual anthropometrics, fostering a positive corporate culture.
- Lower Absenteeism: Reduces workplace injuries and related absences by eliminating common causes such as poor lifting techniques, repetitive stress, and poor workstation design. Healthier work conditions contribute to improved mental and physical well-being, keeping employees consistently present and engaged.
- Cost Savings: Minimizes costs associated with injuries, downtime, and turnover by reducing medical expenses, compensation claims, and retraining efforts. Improved efficiency means less overtime and fewer production delays, leading to substantial ROI over time, as demonstrated by the National Institute for Occupational Safety and Health.
- Compliance with Regulations: Meets occupational safety and health standards, such as OSHA general duty clauses and ISO 6385 guidelines, thereby reducing legal liabilities and financial penalties while facilitating transparent reporting and auditing across global facilities.
Challenges & Biomechanical Constraints in Implementation
- High Initial Capital & Tooling Re-engineering: Substantial capital investment is required to procure industrial exoskeletons, automated scissor-lift tilters, and collaborative robotic workcells. Beyond hardware acquisition, retrofitting existing assembly lines often requires shutting down active cells, modifying structural overhead conveyors, and re-validating cycle times, creating severe financial friction for small-to-medium enterprises (SMEs).
- Behavioral Inertia, Muscle Memory & Cognitive Resistance: Experienced assembly technicians develop deeply ingrained motor programs and heuristic shortcuts over years of manual labor. Introducing new ergonomic fixtures or requiring the use of torque-reaction arms is often perceived as an impediment to piece-rate speed. Without participatory change management, workers frequently bypass safety interlocks or discard wearable supports.
- Anthropometric Diversity & Non-Linear Range Accommodations: Designing workstations to accommodate the 5th percentile female through the 95th percentile male requires wide adjustment ranges across multiple degrees of freedom (e.g., vertical travel \(\Delta z \ge 350\,\text{mm}\), reach envelope \(\Delta r \ge 250\,\text{mm}\)). In mass production environments with high station sharing, manual readjustment consumes valuable shift time, leading operators to work at non-optimal compromises.
- Wearable Sensor Artifacts & Real-Time Data Calibration: Capturing high-fidelity kinematic data on active shop floors is fraught with environmental noise. Ferromagnetic structural steel beams distort electromagnetic motion capture trackers, while wearable IMUs suffer from cumulative gyroscope integration drift (\(\int \epsilon \, dt\)). Furthermore, skin-electrode impedance shifts caused by worker perspiration introduce severe artifacts into surface electromyography (sEMG) fatigue models.
- Dynamic Load Amplification & Speed-Accuracy Trade-Offs: Under intense takt time constraints, workers naturally accelerate reach and lift motions. In accordance with Fitts' Law and Newton's Second Law (\(\mathbf{F} = m\mathbf{a}\)), dynamic peak inertial forces can exceed static loads by \(40\text{--}80\%\). Engineering interventions that limit movement speed to maintain safe joint torques risk bottlenecking production unless accompanied by collaborative automation.
Emerging Trends in Human Factors and Ergonomics for Manufacturing
- AI-Driven Computer Vision Ergonomic Screening: Markerless 3D computer vision algorithms running on edge cameras continuously track 2D/3D human skeletal joints across production cells. Machine learning frameworks automatically calculate real-time REBA and RULA risk scores without requiring intrusive wearable suits, instantly alerting plant supervisors to awkward neck or trunk flexion angles.
- Personalized Active Biomechanical Exosuits: Next-generation motorized soft exosuits utilize carbon-fiber series elastic actuators and electromyographic sensors to provide proportional torque assistance. These active systems anticipate worker lifting intent, dynamically injecting up to \(30\,\text{Nm}\) of assistive torque at the lumbar spine or shoulder complex during the precise instant of peak exertion.
- Virtual Reality (VR) Immersive Anthropometric Prototyping: Before physical tooling or factory layouts are commissioned, industrial engineers utilize immersive VR environments paired with digital human mannequins. Designers simulate reach envelopes, sightline clearances, and hand clearance spaces across global anthropometric databases, preventing costly physical workstation redesigns.
- Sustainable & Circular Ergonomics: Workstation architectures are increasingly engineered using modular, circular aluminum extrusions and non-toxic bio-composites. Ergonomic seating and anti-fatigue flooring are designed for rapid disassembly and material recovery, aligning human health with corporate environmental, social, and governance (ESG) targets.
- Cognitive Workload Monitoring & Neuroergonomics: Industrial neuroergonomics leverages lightweight functional near-infrared spectroscopy (fNIRS) and eye-tracking glasses to monitor cognitive workload and pupillary dilation. In safety-critical aerospace and semiconductor assembly, systems automatically modulate HMI information density when cognitive saturation thresholds are approached.
Future Directions in Human Factors and Ergonomics
- Integration with Industry 5.0 & Human-Centric Cyber-Physical Systems: Industry 5.0 shifts the focus from purely automated productivity back to human-centric, resilient systems. Cyber-physical manufacturing architectures will synthesize real-time physiological telemetry with production scheduling software, reallocating strenuous tasks from fatigued workers to automated machinery dynamically.
- Ergonomics for Aging & Neurodiverse Workforces: As industrial demographics shift toward an older workforce, workstation design is incorporating multi-modal sensory feedback—combining directional acoustic tones, tactile haptic vibrations, and high-contrast ambient lighting—to compensate for age-related sensory declines while accommodating neurodiverse cognitive processing styles.
- Global Harmonization of Ergonomic Standards: Multinational supply chains are establishing unified, auditable ergonomic KPIs adhering to frameworks like ISO 6385 (Ergonomic Principles in the Design of Work Systems). Standardized metrics ensure equitable, dignified working conditions across distributed manufacturing hubs globally.
- Predictive Longitudinal Musculoskeletal Digital Twins: Longitudinal digital human twins will track cumulative biomechanical micro-trauma across an individual worker’s entire multi-year career. Biomechanical algorithms will forecast early disc degeneration or tendinitis risks months in advance, prompting proactive job-rotation regimens before clinical pathology develops.
- Autonomous, Self-Adapting Workcells: Workstations equipped with motorized linear actuators and facial recognition will identify incoming operators and automatically adjust table elevations, bin tilt angles, lighting lux levels, and HMI display heights to match their personalized anthropometric profile within seconds of arrival.
Why Study Human Factors and Ergonomics in Manufacturing
Designing Workplaces That Fit People
Human factors and ergonomics focus on adapting work environments to human needs. Students learn how to design tools, workstations, and tasks that reduce strain and injury. This supports safety, comfort, and productivity.
Understanding Human Capabilities and Limitations
Students study anatomy, biomechanics, and cognitive psychology. They learn how people perceive, think, and move in industrial settings. This knowledge informs better equipment design and workflow organization.
Applications in Manufacturing and Automation
Ergonomics is essential in manual assembly, machine operation, and interface design. Students learn to assess risks and recommend improvements. This contributes to quality, efficiency, and worker satisfaction.
Data Collection and Usability Testing
Students gain skills in task analysis, observational studies, and usability testing. They learn to evaluate human performance and system interaction. These methods support evidence-based design decisions.
Enhancing Workplace Safety and Organizational Outcomes
Ergonomic design reduces injuries, boosts morale, and lowers healthcare costs. Students understand how human-centered design benefits both workers and companies. This creates healthier, more sustainable manufacturing environments.
Human Factors and Ergonomics: Conclusion
Human Factors and Ergonomics (HFE) is an essential aspect of modern manufacturing, ensuring the safety, well-being, and productivity of workers. It goes beyond simple adjustments to tools or environments—it encompasses a systemic approach to designing tasks, technologies, and organizational structures that align with human strengths and limitations. By optimizing the interaction between humans and machines, HFE reduces injuries, enhances operational efficiency, and supports long-term organizational success.
As manufacturing continues to embrace digitization and automation, the role of HFE will expand to address the cognitive and emotional dimensions of work in high-tech environments. Future developments will likely integrate real-time feedback systems, AI-powered ergonomic analysis, and immersive simulation tools to model worker-machine interactions under various conditions. These advancements will empower proactive interventions before discomfort, fatigue, or injury occur, transforming reactive ergonomics into predictive safety systems.
Furthermore, the growing emphasis on diversity, equity, and inclusion will encourage ergonomic designs that accommodate varied body types, ages, and abilities, ensuring that all employees can contribute effectively and comfortably. Platforms like the Human Factors and Ergonomics Society (HFES) are leading efforts to align research, standards, and industry practices.
Ultimately, the evolution of HFE will play a pivotal role in humanizing the future of manufacturing—where technology and people not only coexist but thrive together in environments designed for mutual growth and resilience.
Human Factors and Ergonomics in Manufacturing: Frequently Asked Questions
This FAQ gathers common questions about human factors and ergonomics in manufacturing and provides concise, structured answers for quick reference.
1. What are human factors and ergonomics, and why are they important in the manufacturing industry?
2. How can ergonomic workplace design reduce the risk of musculoskeletal disorders (MSDs) in manufacturing workers?
3. What are the key components of a successful ergonomics program in a manufacturing setting?
4. How can ergonomic assessments be conducted in a manufacturing environment, and what tools are commonly used?
5. What are the common ergonomic hazards in manufacturing, and how can they be mitigated?
6. How can the implementation of ergonomic tools and equipment improve productivity and reduce errors in manufacturing processes?
7. What role does employee training play in the effective implementation of ergonomics in manufacturing, and what key topics should be covered?
8. How can the integration of ergonomic principles into the design of manufacturing processes enhance overall operational efficiency?
9. How can the principles of ergonomics be applied to improve the design of manufacturing tools and equipment?
10. How can human factors engineering be used to design safer and more efficient manufacturing systems?
11. How can wearable ergonomic devices be utilized in manufacturing to monitor and improve worker health and performance?
12. How can participatory ergonomics enhance the effectiveness of ergonomic interventions in manufacturing?
13. How can ergonomics contribute to reducing workplace accidents and enhancing overall safety in manufacturing environments?
Human Factors & Ergonomics Practice Modules
Section 1: Interactive Knowledge Self-Assessment
1. What is the fundamental difference between human factors and physical ergonomics?
2. How do ergonomic interventions prevent Musculoskeletal Disorders (MSDs)?
3. What primary metrics are evaluated using the RULA and REBA assessment tools?
4. Why is task analysis vital prior to introducing industrial automation or cobots?
5. What role does cognitive ergonomics play in automated control room design?
6. How does digital human modeling (DHM) improve line planning?
7. What are the key elements of a participatory ergonomics program?
8. How do industrial exoskeletons impact biomechanical load distribution?
Section 2: Analytical & Scenario-Based Case Studies
1. Scenario: An electronics assembly plant notices a spike in wrist tendonitis among manual soldering technicians. How should engineering evaluate and resolve this?
2. Scenario: On an automotive packing line, operators experience lower back pain from retrieving parts out of 1-meter deep wire bins. What redesign is required?
3. Scenario: A CNC machine operator frequently enters incorrect tool offset values, leading to machine crashes. How can cognitive ergonomics fix this?
4. Scenario: Operators in a stamping plant report fatigue despite working within NIOSH lifting limits. What secondary factors should be investigated?
5. Scenario: A warehouse transitions to voice-guided picking, but errors spike during peak hours. What cognitive ergonomics breakdown occurred?
6. Scenario: An aerospace composite facility introduces active shoulder exoskeletons for overhead drilling, but workers refuse to wear them. Why?
7. Scenario: A food processing line suffers high turnover due to cold environment (≤4°C) and high-speed sorting. How can thermal/physical ergonomics solve this?
Section 3: Mathematical Biomechanics & Ergonomic Calculations
Work through these step-by-step mathematical calculations evaluating spinal compression forces, NIOSH lifting limits, lever mechanics, metabolic allowances, and task illuminance.
Problem 1: NIOSH Recommended Weight Limit (RWL) Derivation
Problem Statement: Calculate the Recommended Weight Limit (\(\text{RWL}\)) under the NIOSH manual lifting equation where Load Constant \(\text{LC} = 23\,\text{kg}\), Horizontal Multiplier \(\text{HM} = 0.80\), Vertical Multiplier \(\text{VM} = 0.90\), Distance Multiplier \(\text{DM} = 0.93\), Asymmetric Multiplier \(\text{AM} = 1.00\), Frequency Multiplier \(\text{FM} = 0.75\), and Coupling Multiplier \(\text{CM} = 0.90\).
Step 1: Multiplicative Equation Formulation
$$\text{RWL} = \text{LC} \times \text{HM} \times \text{VM} \times \text{DM} \times \text{AM} \times \text{FM} \times \text{CM}$$
Step 2: Sequential State Evaluation
$$\text{RWL} = 23 \times 0.80 \times 0.90 \times 0.93 \times 1.00 \times 0.75 \times 0.90$$
$$\text{RWL} = (23 \times 0.72) \times (0.93 \times 0.675) = 16.56 \times 0.62775 = \mathbf{10.395\,\text{kg}}$$
Engineering Interpretation: The baseline load capacity of \(23\,\text{kg}\) is degraded by \(54.8\%\) primarily due to horizontal extension (\(\text{HM} = 0.80\)) and lift frequency (\(\text{FM} = 0.75\)). The nominal design payload for this station should not exceed \(10.40\,\text{kg}\).
Problem 2: Lifting Index (LI) Evaluation & Risk Classification
Problem Statement: A worker lifts an actual load weight \(L = 18.0\,\text{kg}\) in an assembly task where the calculated \(\text{RWL}\) is \(12.0\,\text{kg}\). Compute the Lifting Index (\(\text{LI}\)) and categorize the occupational risk.
Step 1: Lifting Index Formulation
$$\text{LI} = \frac{L}{\text{RWL}}$$
Step 2: Numerical Calculation
$$\text{LI} = \frac{18.0\,\text{kg}}{12.0\,\text{kg}} = \mathbf{1.50}$$
Engineering Interpretation: An \(\text{LI} = 1.50\) exceeds the unity threshold (\(\text{LI} \gt 1.0\)), placing the operation in the moderate-to-high risk category. Redesign of horizontal reach or mechanical hoist integration is mandatory under OSHA ergonomics guidelines.
Problem 3: Horizontal Multiplier (HM) Calculation
Problem Statement: Determine the Horizontal Multiplier (\(\text{HM}\)) for a manual lift where the horizontal distance \(H\) from the midpoint between the ankles to the hands is measured at \(40.0\,\text{cm}\). The NIOSH relation is defined as \(\text{HM} = 25 / H\).
Step 1: Metric Substitution
$$\text{HM} = \frac{25\,\text{cm}}{H} = \frac{25}{40.0} = \mathbf{0.625}$$
Engineering Interpretation: Holding the load \(40\,\text{cm}\) away from the body penalizes allowable capacity by \(37.5\%\) due to the extended moment arm acting on the lumbosacral joint.
Problem 4: 2D Biomechanical Static Lumbar Spine (L5/S1) Compression Analysis
Problem Statement: Calculate lumbar spine compression force \(F_c\) using a 2D biomechanical static moment equilibrium model: \(F_c = W_{\text{upper}} + \left( \frac{W_{\text{load}} \cdot d_{\text{load}}}{d_{\text{muscle}}} \right)\), where upper body weight \(W_{\text{upper}} = 350\,\text{N}\), load weight \(W_{\text{load}} = 200\,\text{N}\), horizontal load distance \(d_{\text{load}} = 45.0\,\text{cm}\), and erector spinae moment arm \(d_{\text{muscle}} = 5.0\,\text{cm}\).
Step 1: Moment Equilibrium at L5/S1 Pivot
$$\sum M_{L_5/S_1} = 0 \Rightarrow F_{\text{muscle}} \cdot d_{\text{muscle}} = W_{\text{load}} \cdot d_{\text{load}}$$
$$F_{\text{muscle}} = \frac{200\,\text{N} \times 45.0\,\text{cm}}{5.0\,\text{cm}} = \frac{9{,}000\,\text{N}\cdot\text{cm}}{5.0\,\text{cm}} = 1{,}800\,\text{N}$$
Step 2: Total Spinal Compressive Force Resolution
$$F_c = W_{\text{upper}} + F_{\text{muscle}} = 350\,\text{N} + 1{,}800\,\text{N} = \mathbf{2{,}150\,\text{N}}$$
Engineering Interpretation: The resulting compressive load of \(2{,}150\,\text{N}\) is below the NIOSH action limit of \(3{,}400\,\text{N}\), indicating a safe static loading condition for a healthy industrial workforce.
Problem 5: Ergonomic Lever Torque & Hand Actuation Force Reduction
Problem Statement: An operator exerts an actuation force \(F_1 = 120.0\,\text{N}\) on a manual clamp lever located at \(d_1 = 0.35\,\text{m}\) from the fulcrum. If an ergonomic redesign extends the handle distance to \(d_2 = 0.50\,\text{m}\), determine the required actuation force \(F_2\) to produce the identical torque.
Step 1: Torque Conservation
$$\tau = F_1 \cdot d_1 = 120.0\,\text{N} \times 0.35\,\text{m} = 42.0\,\text{N}\cdot\text{m}$$
Step 2: New Operating Force Calculation
$$F_2 = \frac{\tau}{d_2} = \frac{42.0\,\text{N}\cdot\text{m}}{0.50\,\text{m}} = \mathbf{84.0\,\text{N}}$$
$$\Delta F_{\%} = \frac{120.0 - 84.0}{120.0} \times 100\% = \mathbf{30.0\%}$$
Engineering Interpretation: Increasing the mechanical advantage lowers muscular exertion by \(30.0\%\), bringing hand grip requirements well within sustainable continuous operational limits.
Problem 6: Metabolic Energy Expenditure & Spitzer Rest Allowance
Problem Statement: Calculate the rest allowance fraction \(R\) for an arduous manual foundry transfer task using Spitzer's equation: \(R = \frac{M - S}{M - 1.2}\), where actual metabolic energy expenditure \(M = 7.5\,\text{kcal/min}\), and standard sustainable physiological limit \(S = 5.0\,\text{kcal/min}\).
Step 1: Value Substitution into Spitzer's Relation
$$R = \frac{7.5 - 5.0}{7.5 - 1.2} = \frac{2.5}{6.3} \approx \mathbf{0.3968}$$
$$R_{\%} = 0.3968 \times 100\% = \mathbf{39.7\%}$$
Engineering Interpretation: A rest allowance of \(39.7\%\) (approximately \(23.8\,\text{minutes}\) per working hour) is required to prevent cumulative cardiovascular exhaustion and blood lactate buildup.
Problem 7: Workstation Photometric Illuminance Evaluation
Problem Statement: Compute the illuminance \(E\) in lux on a precision PCB inspection bench located \(d = 2.0\,\text{m}\) directly beneath a \(1{,}200\,\text{lumen}\) omnidirectional light fixture using the inverse-square law: \(E = I / d^2\), where luminous intensity \(I = \Phi / (4\pi)\).
Step 1: Point Source Luminous Intensity Conversion
$$I = \frac{1{,}200\,\text{lm}}{4\pi\,\text{sr}} \approx \frac{1{,}200}{12.5664} = 95.49\,\text{cd}$$
Step 2: Inverse-Square Illuminance Evaluation
$$E = \frac{I}{d^2} = \frac{95.49\,\text{cd}}{(2.0\,\text{m})^2} = \frac{95.49}{4.0} = \mathbf{23.87\,\text{lux}}$$
Engineering Interpretation: A benchtop illuminance of \(23.87\,\text{lux}\) is critically deficient for inspection tasks (which require \(500\text{--}750\,\text{lux}\) under IESNA standards). Specialized task lighting with localized articulated arms must be installed to prevent eyestrain.