
Advanced Materials and Manufacturing Technologies Education, as mapped here, is not simply about learning “new materials.” It is about learning how to move from possibility to proof. Students start with promising material ideas and real production data, then learn to interrogate them under demanding constraints—strength, durability, cost, safety, repeatability. Using the tools and platforms of modern manufacturing, they practise turning lab-scale insight into manufacturable reality: selecting materials, choosing processes, tuning parameters, and validating performance. The end result is a maker’s kind of literacy—an ability to design, build, measure, and improve—so that innovation becomes something you can produce reliably, not just admire in theory.
- Composite Micromechanics & Anisotropic Elasticity: Formulate the longitudinal Voigt isostrain (\(E_1 = V_f E_f + V_m E_m\)) and transverse Reuss isostress bounds, evaluate Halpin-Tsai corrections, and compute specific modulus metrics.
- High-Temperature Alloys & Creep Kinetics: Analyze single-crystal nickel-base superalloy \(\gamma/\gamma'\) precipitate hardening, thermal barrier coating (TBC) degradation, and Larson-Miller stress-rupture life estimation.
- Precision Deposition & Nanoscale Synthesis: Model Chemical Vapor Deposition (CVD) film growth kinetics, automated fiber placement (AFP) compaction kinematics, and carbon nanotube surface functionalization mechanisms.
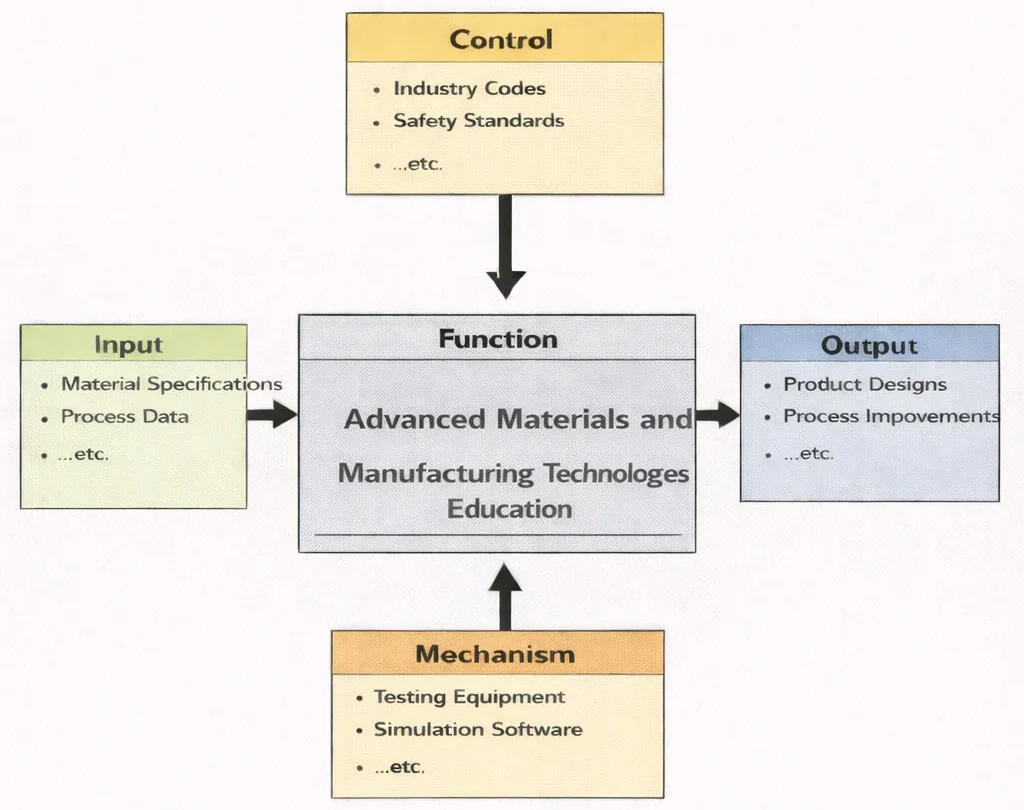
This IDEF0 diagram frames “Advanced Materials and Manufacturing Technologies Education” as a disciplined transformation. On the left, Inputs such as materials innovations and process data feed the learning process. From above, Controls—quality standards and safety regulations—set boundaries that prevent “clever” work from becoming unsafe or non-compliant. From below, Mechanisms (e.g., nanomaterials knowledge, precision machinery, and related lab capabilities) represent the practical means students use to test, fabricate, and validate. On the right, Outputs capture what the education is meant to produce: graduates who can translate advanced materials concepts into new products and measurable efficiency gains in manufacturing.
The rise of Advanced Materials and Manufacturing Technologies has dramatically reshaped the way industries innovate, produce, and deliver value. These technologies are foundational to modern Industrial and Manufacturing Technologies, supporting the transition from conventional processes to advanced, data-driven, and sustainable systems. As materials science continues to uncover novel composites, smart alloys, and nano-structured surfaces, engineers are increasingly able to meet performance demands that were once unattainable.
These materials find synergistic applications through cutting-edge processes like Additive Manufacturing (3D Printing), which allow for rapid prototyping and complex geometries. They are further integrated into Computer-Integrated Manufacturing (CIM) systems and real-time simulations enabled by Digital Twin Technology, driving manufacturing efficiency and precision.
Sustainability is at the forefront of modern production, and innovative materials support Energy and Resource Efficiency in Manufacturing. Their use reduces material wastage, enhances product lifespan, and minimizes environmental impact, thereby aligning well with Sustainable Manufacturing principles. The role of ergonomics and human-centered design is also critical, as seen in Human Factors and Ergonomics in Manufacturing, where the application of light, durable materials improves usability and safety.
Interactive System Dynamics: Composite Micromechanics & Specific Modulus Simulator
Simulate longitudinal composite tensile strength, density, and structural weight reduction versus AISI 4130 structural steel. Adjust fiber volume fraction (\(V_f\)), fiber tensile rating, and polymer matrix strength to evaluate micromechanical rule-of-mixtures behavior in real time.
Constituent Variables
Material Innovation: Advanced Properties and Next-Generation Manufacturing
Advanced Materials and Manufacturing Technologies represent the convergence of materials synthesis and precision fabrication. By engineering composites, smart alloys, and nanostructures, modern industry builds lighter, stronger, and more resilient systems capable of operating in extreme physical environments.
Industrial & Manufacturing Technologies – Overview
Connects material science advancements with industrial production capabilities, establishing the foundation for modern manufacturing systems.
Additive Manufacturing
Enables direct layer-by-layer fabrication of complex geometries using specialized metal powders, ceramics, and high-performance polymers.
Process Design
Develops specialized process parameters tailored to high-temperature alloys, fiber reinforcement layups, and nanoscale synthesis.
Quality Control
Utilizes advanced spectroscopy, electron microscopy, and non-destructive testing to verify internal material purity and structural integrity.
Smart Manufacturing
Integrates smart materials and adaptive sensors directly into automated IIoT production workflows for closed-loop optimization.
Digital Twin
Simulates microstructural deformation, thermal expansion, and mechanical fatigue under operational loads before physical prototyping.
Automation
Applies automated fiber placement (AFP) and robotic tooling to process delicate or hazardous advanced material feedstocks with high precision.
CIM
Unifies materials databases, CAD specifications, and shop-floor execution into a single digital software pipeline.
Supply Chain
Coordinates specialized chemical synthesis, rare earth sourcing, and temperature-sensitive storage logistics across global networks.
Sustainable Manufacturing
Focuses on bio-based polymers, closed-loop composite recycling, and low-carbon processing methods to minimize lifecycle environmental impact.
Energy Efficiency
Optimizes high-energy thermal curing, laser sintering, and plasma deposition processes to reduce factory energy consumption.
Human Factors
Designs safe workplace protocols and ergonomic interfaces for handling airborne nanomaterials, chemical resins, and automated machinery.
Core Concepts of Advanced Materials
Advanced Materials Overview
- Engineered Composites: Combining macroscopically distinct matrix and reinforcement phases to achieve targeted anisotropic properties. Carbon Fiber Reinforced Polymers (CFRP) provide high specific stiffness (\(E/\rho\)) and corrosion immunity in primary aerospace structures.
- High-Temperature Superalloys: Nickel-, iron-, and cobalt-base superalloys engineered with coherent \(\gamma'\) \(\text{Ni}_3(\text{Al, Ti})\) intermetallic precipitates retain yield strength and creep-rupture resistance past \(1,050^\circ\text{C}\).
- Nanomaterials & 2D Crystals: Engineered structures with nanoscale dimensions (\(1 - 100\text{ nm}\))—such as single-layer graphene, multi-walled carbon nanotubes (MWCNTs), and MXenes—where high surface-to-volume ratios and quantum confinement yield extreme electrical conductivity and mechanical modulus.
- Smart & Functional Materials: Shape Memory Alloys (e.g., Nitinol) exhibiting thermoelastic martensitic transformations, piezoelectric ceramics (PZT) translating mechanical strain to electric charge, and magnetostrictive actuators.
Advanced Manufacturing Technologies
- Automated Fiber Placement (AFP) & Resin Transfer Molding (RTM): Multi-axis robotic placement heads steer continuous pre-impregnated fiber tows along contoured paths, followed by high-pressure vacuum injection of thermoset resins.
- Vapor Phase Synthesis (CVD & PVD): Chemical Vapor Deposition (CVD) thermally decomposes gaseous precursors into ultra-hard wear coatings (TiN, TiAlN, diamond-like carbon), while Physical Vapor Deposition (PVD) sputters target atoms onto precision cutting tools.
- Superplastic Forming & Diffusion Bonding (SPF/DB): Utilizing fine-grained titanium alloys at elevated temperatures (\(\sim 900^\circ\text{C}\)) to form complex hollow aerodynamic structures in a single thermal cycle.
Problem Formulation: Voigt/Reuss Elastic Bounds, Halpin-Tsai Transverse Modulus & Specific Performance Ratios
An advanced structures engineer is designing an aerospace primary spar cap using a unidirectional Carbon Fiber Reinforced Polymer (CFRP) lamina. The constituent carbon fibers have longitudinal modulus \(E_{f1} = 240.0\text{ GPa}\), transverse modulus \(E_{f2} = 15.0\text{ GPa}\), tensile strength \(\sigma_f = 4,200.0\text{ MPa}\), Poisson's ratio \(\nu_f = 0.20\), and density \(\rho_f = 1.80\text{ g/cm}^3\). The toughened epoxy matrix exhibits isotropic modulus \(E_m = 3.60\text{ GPa}\), tensile strength \(\sigma_m = 75.0\text{ MPa}\), Poisson's ratio \(\nu_m = 0.35\), and density \(\rho_m = 1.20\text{ g/cm}^3\). For a fiber volume fraction \(V_f = 0.620\), calculate the longitudinal modulus (\(E_1\)) via the Voigt isostrain model, the transverse modulus (\(E_2\)) via the Reuss isostress model, the composite density (\(\rho_c\)), the longitudinal tensile strength (\(\sigma_1\)), and compare the Specific Strength (\(\sigma_1 / \rho_c\)) against high-strength Ti6Al4V alloy (\(\sigma = 950\text{ MPa}\), \(\rho = 4.43\text{ g/cm}^3\)).
- Fiber Volume Fraction: \(V_f = 0.620\); Matrix Volume Fraction: \(V_m = 1.0 - V_f = 0.380\)
- Fiber properties: \(E_{f1} = 240.0\text{ GPa}\), \(E_{f2} = 15.0\text{ GPa}\), \(\sigma_f = 4,200.0\text{ MPa}\), \(\rho_f = 1.80\text{ g/cm}^3\)
- Matrix properties: \(E_m = 3.60\text{ GPa}\), \(\sigma_m = 75.0\text{ MPa}\), \(\rho_m = 1.20\text{ g/cm}^3\)
- Benchmark Ti6Al4V: \(\sigma_{\text{Ti}} = 950.0\text{ MPa}\), \(\rho_{\text{Ti}} = 4.43\text{ g/cm}^3\)
Step 1: Longitudinal Elastic Modulus (\(E_1\)) via Voigt Isostrain Formulation
$$E_1 = E_{f1} \cdot V_f + E_m \cdot V_m = (240.0\text{ GPa} \times 0.620) + (3.60\text{ GPa} \times 0.380)$$ $$E_1 = 148.80\text{ GPa} + 1.368\text{ GPa} = \mathbf{150.168\text{ GPa}}$$Step 2: Transverse Elastic Modulus (\(E_2\)) via Reuss Isostress Formulation
$$\frac{1}{E_2} = \frac{V_f}{E_{f2}} + \frac{V_m}{E_m} = \frac{0.620}{15.0\text{ GPa}} + \frac{0.380}{3.60\text{ GPa}}$$ $$\frac{1}{E_2} = 0.041333 + 0.105556 = 0.146889\text{ GPa}^{-1}$$ $$E_2 = \frac{1}{0.146889} = \mathbf{6.808\text{ GPa}}$$(Notice the high anisotropy: \(E_1 / E_2 \approx 22.1\), illustrating the extreme directional stiffness of unidirectional composite laminae).
Step 3: Composite Density (\(\rho_c\)) and Longitudinal Tensile Strength (\(\sigma_1\))
$$\rho_c = \rho_f \cdot V_f + \rho_m \cdot V_m = (1.80\text{ g/cm}^3 \times 0.620) + (1.20\text{ g/cm}^3 \times 0.380) = 1.116 + 0.456 = \mathbf{1.572\text{ g/cm}^3}$$Apply the longitudinal rule of mixtures for ultimate tensile strength:
$$\sigma_1 = \sigma_f \cdot V_f + \sigma_m \cdot V_m = (4,200.0\text{ MPa} \times 0.620) + (75.0\text{ MPa} \times 0.380)$$ $$\sigma_1 = 2,604.0\text{ MPa} + 28.5\text{ MPa} = \mathbf{2,632.50\text{ MPa}}$$Step 4: Specific Strength Comparison with Aerospace Titanium
$$\text{Specific Strength}_{\text{CFRP}} = \frac{\sigma_1}{\rho_c} = \frac{2,632.50\text{ MPa}}{1.572\text{ g/cm}^3} = \mathbf{1,674.62\text{ MPa}\cdot\text{cm}^3\text{/g}}$$ $$\text{Specific Strength}_{\text{Ti}} = \frac{\sigma_{\text{Ti}}}{\rho_{\text{Ti}}} = \frac{950.0\text{ MPa}}{4.43\text{ g/cm}^3} = \mathbf{214.45\text{ MPa}\cdot\text{cm}^3\text{/g}}$$ $$\text{Performance Multiplier} = \frac{1,674.62}{214.45} = \mathbf{7.81\times}$$Systems Engineering Trade-Off Matrix: Advanced Material Classes
Selecting advanced engineering materials requires balancing specific mechanical modulus, operational temperature envelopes, manufacturing scalability, raw feedstock costs, and damage tolerance.
| Material Class | Primary Microstructural Phase | Operating Temp Range | Specific Modulus (\(E/\rho\)) | Failure Modes & Environmental Limits | Primary Manufacturing Route |
|---|---|---|---|---|---|
| Carbon Fiber Composites (CFRP) | Graphitic basal fibrils in crosslinked thermoset matrix | Cryogenic to \(180^\circ\text{C}\) (epoxy limit) | Exceptional (\(85 - 130\text{ GPa}\cdot\text{cm}^3\text{/g}\)) | Delamination, impact micro-cracking, moisture absorption | Autoclave prepreg, AFP, RTM injection molding |
| Single-Crystal Nickel Superalloys | Coherent \(\gamma'\) \(\text{Ni}_3(\text{Al,Ti})\) precipitates in FCC \(\gamma\) matrix | Up to \(1,150^\circ\text{C}\) | Moderate (\(15 - 20\text{ GPa}\cdot\text{cm}^3\text{/g}\)) | Creep cavity coalescence, high-temperature hot corrosion | Investment casting with helical grain selectors |
| Ceramic Matrix Composites (CMC) | Continuous SiC fibers in chemical-vapor-infiltrated SiC matrix | Up to \(1,400^\circ\text{C}\) | High (\(70 - 90\text{ GPa}\cdot\text{cm}^3\text{/g}\)) | Brittle matrix micro-cracking, high-temp steam oxidation | Chemical Vapor Infiltration (CVI), polymer infiltration |
| Titanium-Aluminides (\(\gamma\)-TiAl) | Ordered intermetallic lamellar \(\alpha_2-\text{Ti}_3\text{Al} + \gamma-\text{TiAl}\) | Up to \(750^\circ\text{C}\) | High (\(40 - 45\text{ GPa}\cdot\text{cm}^3\text{/g}\)) | Very low room-temperature ductility (\(\epsilon \lt 1.5\%\)) | Electron Beam Melting (E-PBF), vacuum induction casting |
| Carbon Nanotube (CNT) Nanocomposites | Multi-walled CNTs dispersed in engineering polymer | Cryogenic to \(250^\circ\text{C}\) | Moderate (\(20 - 35\text{ GPa}\cdot\text{cm}^3\text{/g}\)) | Nanoparticle bundling/agglomeration, interfacial slippage | High-shear sonication, twin-screw melt compounding |
Applications of Advanced Materials & Manufacturing
- Aerospace Primary Structures & Propulsion: Carbon-fiber wing skins and empennage assemblies cut airframe structural weight by 20%, while CMC shroud tiles enable commercial jet engines to operate without cooling bleed air at turbine inlet temperatures exceeding \(1,300^\circ\text{C}\).
- Electric Vehicle Battery Enclosures: Crash-resistant extruded aluminum alloys coupled with fire-retardant organosheet composites safeguard lithium-ion modules during vehicle collisions while minimizing parasitic vehicle curb weight.
- Orthopedic Biocompatible Implants: Porous electron-beam melted Ti6Al4V acetabular cups coated with plasma-sprayed hydroxyapatite stimulate natural bone remodeling and cellular osseointegration, preventing long-term implant loosening.
- Industrial Machining & Tooling Coatings: Multi-layer nanostructured TiAlN and diamond-like carbon (DLC) coatings deposited via magnetron sputtering reduce friction coefficients and maintain cutting edge hardness up to \(900^\circ\text{C}\).
Why Study Advanced Materials and Manufacturing Technologies
Anisotropic Solid Mechanics & Constitutive Modeling
Students master laminate theory, classical tensor stress transformations, and fracture mechanics governing composite and crystal structures.
Process Metallurgy and Phase Transformations
Engineers gain hands-on expertise with precipitation kinetics, time-temperature-transformation (TTT) diagrams, and directional solidification phenomena.
Advanced Analytical Characterization Mastery
Coursework covers Transmission Electron Microscopy (TEM), X-ray diffraction (XRD), and dynamic mechanical thermal analysis (DMTA) to diagnose atomic defects.
High-Value Precision Manufacturing Methods
Students design scalable automated production lines combining robotic AFP, Chemical Vapor Deposition, and Hot Isostatic Pressing.
Advanced Materials and Manufacturing Technologies: Conclusion
Advanced Materials and Manufacturing Technologies represent the fundamental bridge between microstructural science and industrial execution. By developing high-temperature superalloys, fiber composites, and functional nanostructures, engineers produce lighter, more resilient systems capable of operating in extreme physical environments. As computational material discovery, automated fiber placement, and digital twin simulation advance, this discipline provides the essential technical foundation for the next generation of aerospace, automotive, and biomedical innovation.
Frequently Asked Questions
What are the primary advantages of composite materials over structural alloys?
Composites deliver significantly higher specific strength (\(\sigma/\rho\)) and specific modulus (\(E/\rho\)) than structural steel or aluminum, while offering complete immunity to electrochemical corrosion and superior fatigue endurance under cyclic loading.
Why are single-crystal superalloys required for modern gas turbine blades?
At operational temperatures above \(1,000^\circ\text{C}\), conventional polycrystalline alloys fail via grain boundary sliding, creep cavitation, and oxidation. Single-crystal superalloys eliminate grain boundaries entirely along the primary stress axis, providing exceptional creep rupture life.
What prevents carbon nanotubes from achieving theoretical strength in bulk composites?
While individual carbon nanotubes possess tensile strengths exceeding 60 GPa, strong van der Waals forces cause them to agglomerate into tangled bundles. Overcoming this requires chemical surface functionalization and high-shear dispersion to prevent interfacial slippage under load.
End-of-Page Practice & Assessment Modules
Section 1: Interactive Foundational Concepts Review
Question 1: Material Structure Classification
Question 2: Nanoscale Mechanics
Question 3: High-Temperature Superalloys
Question 4: Smart Material Responsiveness
Section 2: Analytical & Scenario-Based Inquiry
Question 1: Aerospace Material Selection Criteria
Question 2: Nanocomposite Dispersion Optimization
Question 3: Thermal Barrier Coating (TBC) Spallation
Section 3: Applied Engineering Quantitative Calculations
Problem 1: Composite Rule of Mixtures Tensile Strength
Question: A unidirectional CFRP composite consists of a \(60.0\%\) carbon fiber volume fraction (\(V_f = 0.60\)) and \(40.0\%\) epoxy matrix (\(V_m = 0.40\)). The tensile strength of the fiber is \(4,000.0\text{ MPa}\), and the tensile strength of the epoxy matrix is \(80.0\text{ MPa}\). Calculate the longitudinal tensile strength of the composite (\(\sigma_c\)) using the Rule of Mixtures.
Solution:
1. Rule of Mixtures equation: \(\sigma_c = (\sigma_f \cdot V_f) + (\sigma_m \cdot V_m)\)
2. Fiber contribution: \(4,000.0\text{ MPa} \times 0.60 = 2,400.0\text{ MPa}\)
3. Matrix contribution: \(80.0\text{ MPa} \times 0.40 = 32.0\text{ MPa}\)
4. Total longitudinal tensile strength:
$$\sigma_c = 2,400.0\text{ MPa} + 32.0\text{ MPa} = \mathbf{2,432.0\text{ MPa}}$$Problem 2: Composite Elastic Modulus Calculation
Question: Calculate the longitudinal elastic modulus (\(E_c\)) of a glass-fiber composite with a \(45.0\%\) fiber volume fraction (\(V_f = 0.45\)). The elastic modulus of E-glass fiber is \(E_f = 72.0\text{ GPa}\), and the matrix modulus is \(E_m = 3.50\text{ GPa}\).
Solution:
1. Rule of Mixtures formula: \(E_c = (E_f \cdot V_f) + [E_m \cdot (1 - V_f)]\)
2. Fiber contribution: \(72.0\text{ GPa} \times 0.45 = 32.40\text{ GPa}\)
3. Matrix fraction: \(1.0 - 0.45 = 0.55\)
4. Matrix contribution: \(3.50\text{ GPa} \times 0.55 = 1.925\text{ GPa}\)
5. Composite longitudinal modulus:
$$E_c = 32.40 + 1.925 = \mathbf{34.325\text{ GPa}}$$Problem 3: Aerospace Mass Reduction & Density Comparison
Question: An aerospace bracket made of steel (\(\rho_{\text{steel}} = 7.85\text{ g/cm}^3\)) has a volume of \(400.0\text{ cm}^3\). Redesigning the component in carbon fiber composite gives a density of \(\rho_{\text{comp}} = 1.55\text{ g/cm}^3\) for the same volume. Calculate total mass saved in kilograms and percentage weight reduction.
Solution:
1. Baseline steel mass: \(400.0\text{ cm}^3 \times 7.85\text{ g/cm}^3 = 3,140.0\text{ g} = 3.140\text{ kg}\)
2. Composite redesign mass: \(400.0\text{ cm}^3 \times 1.55\text{ g/cm}^3 = 620.0\text{ g} = 0.620\text{ kg}\)
3. Total mass saved: \(3.140\text{ kg} - 0.620\text{ kg} = \mathbf{2.520\text{ kg saved}}\)
4. Percentage reduction: \(\left(\frac{2.520}{3.140}\right) \times 100\% = \mathbf{80.25\%}\)
Problem 4: Specific Strength Efficiency Ratio
Question: Titanium alloy (Ti6Al4V) has a tensile strength of \(900.0\text{ MPa}\) and density of \(4.43\text{ g/cm}^3\). A CFRP composite exhibits tensile strength of \(1,800.0\text{ MPa}\) and density of \(1.60\text{ g/cm}^3\). Determine the specific strength of both materials and calculate the efficiency multiplier.
Solution:
1. Specific strength of Titanium alloy: \(\frac{900.0\text{ MPa}}{4.43\text{ g/cm}^3} = \mathbf{203.16\text{ MPa}\cdot\text{cm}^3\text{/g}}\)
2. Specific strength of CFRP composite: \(\frac{1,800.0\text{ MPa}}{1.60\text{ g/cm}^3} = \mathbf{1,125.00\text{ MPa}\cdot\text{cm}^3\text{/g}}\)
3. Efficiency multiplier:
$$\text{Ratio} = \frac{1,125.00}{203.16} = \mathbf{5.54\times}$$Problem 5: Surface-Area-to-Volume Ratio of Nanoparticles
Question: A spherical microparticle has a radius \(R = 1.0\text{ mm}\) (\(1,000,000.0\text{ nm}\)). A spherical nanoparticle has a radius \(r = 10.0\text{ nm}\). Calculate the Surface-Area-to-Volume ratio (\(\text{SA}/V = 3/r\)) for both particles and find the multiplier increase for the nanoparticle.
Solution:
1. Microparticle ratio: \(\frac{3}{1,000,000.0\text{ nm}} = 3.0 \times 10^{-6}\text{ nm}^{-1}\)
2. Nanoparticle ratio: \(\frac{3}{10.0\text{ nm}} = 0.30\text{ nm}^{-1}\)
3. Multiplier increase:
$$\text{Multiplier} = \frac{0.30}{3.0 \times 10^{-6}} = \mathbf{100,000\times}$$Problem 6: Thin-Film CVD Deposition Time
Question: A chemical vapor deposition (CVD) process deposits a wear-resistant Titanium Nitride (TiN) coating onto cutting tools at a constant rate of \(1.50\text{ µm/hr}\). If the engineering drawing specifies a uniform coating thickness of \(7.50\text{ µm}\), calculate required deposition time in hours.
Solution:
1. Deposition time formula:
$$t_{\text{dep}} = \frac{\text{Required Thickness}}{\text{Deposition Rate}} = \frac{7.50\text{ µm}}{1.50\text{ µm/hr}} = \mathbf{5.00\text{ hours}}$$Problem 7: Composite Fiber & Matrix Raw Material Cost Split
Question: A composite part weighing \(10.0\text{ kg}\) has a fiber mass fraction of \(70.0\%\) carbon fiber and \(30.0\%\) epoxy resin matrix. Carbon fiber raw cost is \(\$40.00\text{/kg}\) and resin cost is \(\$10.00\text{/kg}\). Determine total raw material cost for the part.
Solution:
1. Fiber mass: \(10.0\text{ kg} \times 0.70 = 7.00\text{ kg}\)
2. Resin mass: \(10.0\text{ kg} \times 0.30 = 3.00\text{ kg}\)
3. Fiber cost: \(7.00\text{ kg} \times \$40.00\text{/kg} = \$280.00\)
4. Resin cost: \(3.00\text{ kg} \times \$10.00\text{/kg} = \$30.00\)
5. Total raw material cost: \(\$280.00 + \$30.00 = \mathbf{\$310.00}\)