
Sustainable manufacturing represents a transformative approach to production that prioritizes environmental stewardship, economic viability, and social responsibility. By integrating principles of resource efficiency and lifecycle thinking, it seeks to reduce the environmental footprint of manufacturing while enhancing long-term competitiveness. The field draws from foundational knowledge in industrial and manufacturing technologies, evolving in response to increasing global concerns about climate change, resource depletion, and industrial emissions.
Sustainable manufacturing is not a single technique; it is a change of conscience inside engineering. It asks a student to look beyond the immediate triumph of “it works” and to ask the longer question: What does it cost the world for it to work this way? The diagram captures how that habit is cultivated. The inputs—materials choices and energy practices—bring the subject down to earth, where every kilogram, every kilowatt-hour, and every discarded offcut matters. The controls—goals and assessment—keep sustainability from drifting into vague good intentions; they insist on defined targets, transparent reasoning, and accountable results. In the central function, learners practice translating values into design decisions: selecting materials with purpose, reducing waste by redesign rather than apology, and improving processes without shifting harm elsewhere. The mechanisms—lifecycle tools and clean technology—act as the student’s instruments of truth, revealing hidden trade-offs and making improvement measurable. The outputs, then, are more than “green awareness”: they are informed students who can defend their choices with evidence, and cleaner processes that reflect careful design, disciplined measurement, and a willingness to improve what industry has long taken for granted.
- Industrial Decarbonization & Life Cycle Assessment (LCA): Quantifying Scope 1, 2, and 3 carbon accounting, embodied carbon substitutions, and ISO 14040/14044 cradle-to-grave inventory modeling.
- Resource Recovery & Circular Economy Mechanics: Closed-loop solvent extraction, industrial water recycling (MBR/RO), affinity-law fan throttling (VFDs), and additive near-net-shape buy-to-fly reduction.
- Digital Sustainability & Clean Technologies: Deploying Physics-Informed Neural Networks (PINNs) for real-time heat-recovery modeling, microgrid dispatch optimization, and IoT-driven waste-heat boiler economics.
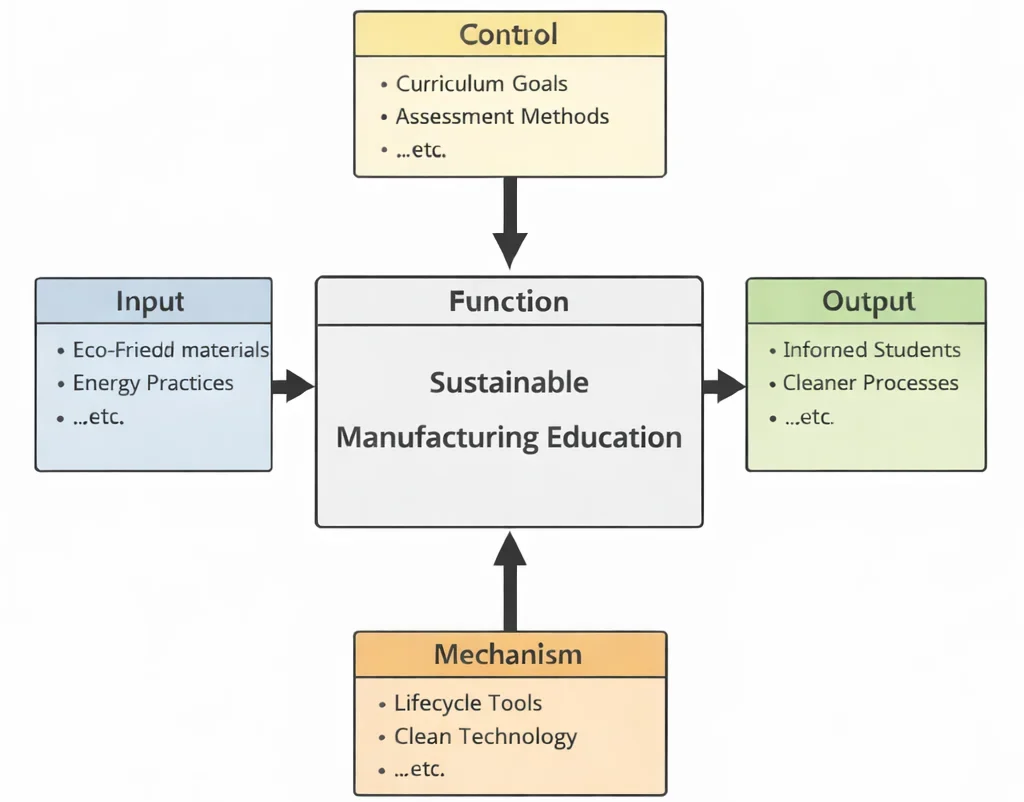
This IDEF0 (Input–Control–Output–Mechanism) diagram frames Sustainable Manufacturing Education as a structured system for building practical sustainability competence. Inputs on the left—eco-friendly materials and energy practices—represent the foundational knowledge and real-world approaches students must engage with. Controls at the top—curriculum goals and assessment methods—set direction and define how learning is evaluated, ensuring sustainability is taught with clarity and measurable standards. The central function, Sustainable Manufacturing Education, transforms inputs and controls into applied understanding through guided learning and practice. Outputs on the right—Informed Students and Cleaner Processes—represent the educational aim: learners who can make responsible decisions and contribute to lower-impact production. Mechanisms at the bottom—lifecycle tools and clean technology—provide the practical enablers that support analysis, design choices, and improvement work across materials, processes, and product life cycles.
Modern strategies for sustainability include the adoption of energy and resource efficiency in manufacturing, which emphasizes lean input use and minimal waste. This aligns with the goals of lean manufacturing, creating operational synergy between cost reduction and ecological impact minimization. Incorporating digital twin technology enables simulations of environmental performance, helping firms preemptively optimize product and process sustainability.
Innovations like Additive Manufacturing (3D Printing) contribute to sustainable practices by reducing material waste and supporting decentralized production. Similarly, advanced materials and manufacturing technologies introduce lightweight, recyclable, and energy-efficient alternatives to conventional components.
At the design level, computer-aided design (CAD) empowers engineers to create products with minimal environmental impact, integrating end-of-life considerations from the outset. Complementing these efforts, manufacturing process design and optimization focuses on streamlining workflows to conserve energy, time, and materials.
Sustainability also depends on human-centered engineering. Incorporating human factors and ergonomics helps create healthier and safer workplaces, which contributes to social sustainability. Simultaneously, quality control and assurance ensures products meet regulatory standards and minimize rework, reducing resource waste.
Automation and intelligent systems play a crucial role in sustainability. The rise of industrial automation and robotics helps optimize energy use and enhances precision, reducing unnecessary consumption. When embedded within computer-integrated manufacturing, these systems offer a framework for holistic sustainability monitoring across facilities.
Sustainable manufacturing must also embrace broader systemic shifts. The concept of Smart Manufacturing and Industry 4.0 introduces real-time data integration, predictive maintenance, and self-adaptive systems that reduce downtime and resource waste. Equally important is supply chain management, which ensures sustainable sourcing, transportation, and end-user delivery.
Beyond industrial systems, sustainable thinking influences cross-disciplinary domains. In automotive engineering, lightweight materials and fuel efficiency are emphasized. Biomechanical engineering explores eco-friendly prosthetics and health devices. Even fundamental areas like thermodynamics and heat transfer contribute to developing efficient heating and cooling systems within factories.
Supportive fields such as fluid mechanics and hydraulics enhance the design of low-energy transport and cooling systems, while solid mechanics underpins structural integrity and material conservation. Advances in nanotechnology further support the development of green coatings and energy-efficient surfaces.
Finally, the integration of robotics in mechanical engineering accelerates smart manufacturing, while the foundational knowledge offered in mechanical engineering remains indispensable for designing efficient systems. As global industries strive for decarbonization and resilience, sustainable manufacturing becomes a vital field that bridges innovation, efficiency, and ethics in engineering.

Sustainable Production: Environmental Responsibility and Lifecycle Thinking
Explore our comprehensive curriculum modules to see how core technologies integrate into cohesive, intelligent production workflows within the broader industrial engineering ecosystem:
Industrial & Manufacturing Technologies Overview
Frames sustainability as a core objective within industrial production systems across the overarching curriculum roadmap.
Sustainable Manufacturing (Current Topic)
Designs production systems that minimize environmental impact while maintaining economic viability and operational throughput.
Energy & Resource Efficiency
Optimizes material consumption and power loads to directly eliminate industrial waste streams and carbon emissions.
Lean Manufacturing
Eliminates non-value-added operational waste and supports environmentally responsible, streamlined factory workflows.
Process Design
Develops high-performance manufacturing sequences designed specifically to minimize ecological footprint and toxic byproducts.
Supply Chain Management
Promotes sustainable procurement, closed-loop reverse logistics, and carbon-neutral freight transport systems.
Smart Manufacturing
Leverages real-time IoT sensors and cloud intelligence to optimize energy distribution and monitor emissions levels.
Digital Twin
Simulates full product lifecycles and virtual plant conditions to optimize green manufacturing parameters before physical execution.
Additive Manufacturing
Dramatically reduces raw material scrap via near-net-shape 3D printing and localized, on-demand component fabrication.
Advanced Materials
Enables the synthesis of bio-based polymers, lightweight alloys, and fully recyclable composite matrix structures.
Automation
Improves energy efficiency and reduces material defects through precise, automated equipment motion controls.
CIM
Integrates carbon tracking and environmental compliance metrics directly into automated shop-floor management software.
Quality Control
Ensures manufactured products adhere strictly to green certifications and zero-defect environmental compliance standards.
Human Factors
Fosters occupational health, ergonomic safety, and workplace well-being as key components of social sustainability.
Core Principles of Sustainable Manufacturing
Resource Efficiency
Definition: Resource efficiency is the strategic engineering approach of extracting maximum functional value from raw materials, electrical energy, water, and auxiliary gases while eliminating waste, fugitive emissions, and operating costs across all life-cycle stages.
- Optimizing production sequences using Lean flow methodologies to cut idle running times and auxiliary heating power draw.
- Deploying industrial variable frequency drives (VFDs) and high-efficiency IE4 electric motors to regulate process fluid and air flow.
- Establishing internal closed loops to capture metallic chips and machining swarf for re-melting and additive atomization.
- Recovering low-grade industrial waste heat via economizers and heat exchangers to pre-heat boiler feedwater or heat wash tanks.
Waste & Emission Reduction
Definition: Systematically minimizing hazardous and non-hazardous solid, liquid, and airborne discharges through source reduction, process redesign, and chemical recovery.
- Eliminating single-use industrial cutting fluids by switching to Minimum Quantity Lubrication (MQL) and cryogenic CO2 cooling.
- Transitioning factory thermal equipment to on-site renewable power, green hydrogen, or industrial electric heat pumps.
- Adhering to authoritative carbon accounting protocols as guided by the EPA Center for Corporate Climate Leadership.
Sustainable Materials & Lifecycle Thinking
Definition: Replacing virgin, finite, or toxic materials with bio-based, non-toxic, and high-recycled-content alternatives, guided by comprehensive life cycle assessments (LCA) from cradle to grave.
- Specifying post-consumer recycled (PCR) aluminum and thermoplastics to cut upstream extraction emissions by up to 90%.
- Designing modular mechanical assemblies for non-destructive disassembly, remanufacturing, and component refurbishment.
- Conducting standardized LCA studies adhering to ISO 14040/14044 to verify environmental footprints across global supply chains.
Contemporary Computational Paradigms: Digital LCA & Physics-Informed Carbon Optimization
Modern sustainable manufacturing relies on computational modeling to evaluate environmental trade-offs before committing physical resources. By coupling discrete-event digital twins with real-time thermodynamic simulations and neural network estimators, green factories optimize their carbon intensity dynamically.
Thermodynamic Waste Heat Recovery & Fluid Affinity Formulations
The energy recovery potential (\(\dot{Q}_{\text{rec}}\)) from industrial furnace flue gases or high-temperature exhaust streams is governed by the mass flow rate (\(\dot{m}\)), specific heat capacity (\(c_p\)), temperature differential (\(\Delta T\)), and heat exchanger effectiveness (\(\varepsilon\)):
$$\dot{Q}_{\text{rec}} = \varepsilon \cdot \dot{m} c_p (T_{\text{exhaust}} - T_{\text{ambient}})$$
For auxiliary ventilation and fluid delivery systems, significant electricity savings are achieved by modulating motor speeds via Variable Frequency Drives (VFDs). In accordance with the Affinity Laws for Turbomachinery, the shaft power consumption (\(P\)) scales cubically with rotational speed (\(N\)):
$$\frac{P_2}{P_1} = \left( \frac{N_2}{N_1} \right)^3 = \left( \frac{Q_2}{Q_1} \right)^3$$
Throttling fan flow rate by just 20% (\(Q_2 / Q_1 = 0.80\)) drops instantaneous electrical power draw to \((0.80)^3 = 0.512\) (a 48.8% reduction), demonstrating the nonlinear energy advantages of electronic speed control over mechanical duct dampers.
Physics-Informed Neural Networks (PINNs) in Factory Carbon Optimization
Smart factories deploy Physics-Informed Neural Networks (PINNs) to solve transient heat transfer and multi-echelon carbon accounting equations simultaneously across variable production shifts. By penalizing deviations from physical conservation of energy and material mass balance:
$$\mathcal{L}_{\text{PINN}} = \|\mathbf{y}_{\text{sensor}} - \hat{\mathbf{y}}\|^2 + \lambda_{\text{energy}} \left\| \rho c_p \frac{\partial T}{\partial t} - \nabla \cdot (k \nabla T) - \dot{q}_{\text{process}} \right\|^2 + \lambda_{\text{mass}} \left\| \frac{\partial \rho_{\text{mat}}}{\partial t} + \nabla \cdot (\rho_{\text{mat}} \mathbf{v}) \right\|^2$$
These models predict thermal energy losses and material degradation in real time. Embedded within edge controllers, neural optimizers adjust machine tool acceleration curves and furnace heating cycles to match live renewable microgrid solar and wind generation windows.
Systems Engineering Trade-Off Matrix: Sustainable Manufacturing Interventions
Selecting clean manufacturing interventions requires evaluating critical multi-variable trade-offs between capital expenditure, carbon abatement efficiency, product performance, and operational complexity:
| Sustainability Strategy | Core Environmental Advantage | Engineering Bottlenecks & Risks | Design Mitigation Strategy |
|---|---|---|---|
| Near-Net-Shape Additive Manufacturing | Lowers buy-to-fly ratios from 8:1 down to 1.2:1; eliminates massive metallic scrap generated in subtractive milling. | High specific electrical energy per kilogram deposited; high raw powder purchasing expense. | Reserve 3D printing for complex, high-value alloys (Ti-6Al-4V, Inconel); deploy inert gas powder sieving for >90% re-use. |
| Post-Consumer Recycled (PCR) Materials | Cuts virgin material embodied carbon by up to 70–90%; reduces landfill accumulation. | Batch-to-batch chemical impurity variations; degraded fatigue life and impact toughness. | Implement strict spectral XRF incoming inspection; blend virgin and PCR feedstock in verified ratios. |
| Industrial Waste Heat Recovery Boilers (WHRB) | Captures high-temperature exhaust gas to generate facility steam; displaces fossil natural gas combustion. | Corrosive acid condensation if flue gas drops below dew point; thermal fatigue cracking on boiler tubes. | Utilize corrosion-resistant stainless-steel alloy exchangers; install automated flue bypass dampers. |
| Closed-Loop Membrane Water Recycling (RO/MBR) | Recovers up to 85–95% of industrial rinse water; eliminates trade effluent discharge surcharges. | Membrane fouling from surfactants and organic dyes; high chemical cleaning downtime. | Install automated multi-stage sand/carbon pre-filters; implement automated cross-flow backwash cycles. |
Applications of Sustainable Manufacturing Systems
About This Interactive Simulator:
This dynamic simulator models industrial lifecycle carbon footprint and energy trade-offs during factory operations. By adjusting key operational levers, observe how clean energy integration and material recycling directly lower total carbon intensity and improve ESG performance.
- Renewable Energy Mix (%) [Solid Green Line]: Controls the percentage of factory power derived from on-site solar, wind, or green PPAs, reducing operational Scope 2 carbon emissions.
- Recycled Material Content (%) [Control Slider]: Sets the ratio of reclaimed or bio-based feedstock used in production, lowering embodied Scope 3 material footprint.
- Heat Recovery Factor [Dashed Blue Line]: Simulates the impact of industrial waste heat recovery and affinity-law fan throttling, highlighting net energy savings across time.
Interactive Factory Lifecycle Carbon & Energy Simulator
Adjust control sliders below to visualize real-time impacts on Scope 1, 2, and 3 emissions, energy intensity, and net sustainability rating.
Automotive Industry
Automotive assembly utilizes lightweighting strategies—substituting high-strength virgin steel with recycled aluminum sheets and bio-based polymer matrices—to directly cut vehicular curb weight and operational exhaust emissions. Closed-loop stamping programs collect clean aluminum skeleton offcuts directly beneath stamping presses, shipping them directly back to secondary smelters to preserve 95% of embodied alloying energy.
Electronics Manufacturing
High-tech electronics OEMs enforce design-for-demanufacturing, eliminating irreversible structural potting resins in favor of serviceable snap-fits. Laser-etched QR digital product passports log rare earth magnet formulations and battery chemistries, enabling automated robotic disassembly lines to recover critical cobalt, nickel, and neodymium with zero landfill leakage.
Textile, Food & Chemical Industries
Process industries eliminate hazardous effluent streams via on-site closed loops. Textile wet-processing lines deploy membrane bioreactors and reverse osmosis systems that recover over 85% of washing water. Chemical and pharmaceutical facilities integrate continuous solvent distillation columns, recovering volatile organic solvents for immediate re-use in active pharmaceutical synthesis.
Benefits of Sustainable Manufacturing
- Environmental Protection: Minimizes greenhouse gas emissions, eliminates hazardous effluent discharge, and protects natural ecosystems through responsible resource stewardship.
- Substantial Operating Cost Savings: Lower utility bills from decreased electricity and water usage, reduced virgin material consumption through recycling, and avoided landfill fees create long-term financial resilience.
- Regulatory Compliance: Proactively meets tightening environmental legislation (e.g., EU Corporate Sustainability Due Diligence, US EPA rules) and earns international ISO 14001 and ISO 5001 certifications.
- Enhanced Brand Equity & ESG Rating: Demonstrating verified environmental performance attracts sustainability-minded institutional investors, enhances CDP climate scores, and secures preferred vendor status with global enterprises.
- Long-Term Supply Chain Resilience: Decoupling production volume from finite virgin mineral inputs insulates manufacturers from global geopolitical commodity price shocks and raw material shortages.
Challenges & Systemic Constraints in Implementation
- High Initial Capital Expenditure: Deploying waste heat recovery boilers, membrane bioreactors, and on-site solar/wind microgrids involves significant capital outlay with payback periods spanning 2 to 5 years.
- Multi-Tier Supply Chain Complexity: Tracking Scope 3 emissions and verifying ethical mineral extraction across overseas Tier-2 and Tier-3 suppliers demands extensive data auditing and traceability infrastructure.
- Material Purity and Performance Variability: Recycled feedstocks and bio-based polymers frequently exhibit variability in melt flow index, tensile yield, and thermal stability compared to standardized virgin petroleum inputs.
- Technical Integration with Legacy Facilities: Retrofitting existing steam boilers, mechanical presses, and legacy pneumatic infrastructure with digital energy-monitoring transducers requires custom engineering and plant downtime.
Emerging Trends & Future Directions in Sustainable Manufacturing
- Net-Zero & Carbon-Negative Production Facilities: Integrating on-site renewable microgrids with electrified thermal processes to eliminate Scope 1 and 2 fossil fuel emissions completely.
- Molecular-Scale Advanced Recycling: Deploying chemical pyrolysis, enzymatic breakdown, and hydrometallurgical leaching to break complex multi-material composites and batteries down to virgin-grade chemical monomers.
- Digital Product Passports (DPP): Molding cryptographic NFC chips or QR codes into physical goods to log material provenance, carbon footprint, and disassembly instructions for automated recycling sorters.
- Bio-Manufacturing & Mycelium Composites: Utilizing biological cell cultures, fungal mycelium, and agricultural cellulose waste to grow structural packaging, replacing expanded polystyrene foam.
Why Study Sustainable Manufacturing
Balancing Production with Environmental Responsibility
Sustainable manufacturing focuses on minimizing the environmental impact of production processes. Students learn how to reduce waste, energy consumption, and emissions. This supports long-term ecological balance and regulatory compliance.
Green Technologies and Materials
Students study renewable energy systems, biodegradable materials, and eco-friendly processes. They explore how to design products and systems with sustainability in mind. This fosters innovation that aligns with environmental goals.
Life Cycle Assessment and Resource Efficiency
The course introduces tools for analyzing the environmental impact of products over their lifespan. Students learn to optimize resource use from raw materials to disposal. This enables more sustainable decision-making in engineering and design.
Compliance with Regulations and Standards
Students explore environmental laws, certifications, and sustainability reporting. They learn how to align operations with global frameworks like ISO 14001. This ensures ethical and responsible business practices.
Innovation for a Circular Economy
Sustainable manufacturing supports reuse, remanufacturing, and recycling. Students study how to design closed-loop systems that reduce environmental impact. This prepares them to lead in circular economy transitions.
Sustainable Manufacturing: Conclusion
Sustainable manufacturing represents a transformative paradigm shift in how goods are produced, emphasizing not only economic productivity but also environmental stewardship and social responsibility. As industrialization continues to expand globally, traditional manufacturing approaches are increasingly recognized as unsustainable due to their reliance on finite resources, high energy consumption, and substantial waste generation. In contrast, sustainable manufacturing aims to balance profitability with the urgent need to preserve ecological systems, reduce carbon footprints, and foster ethical labor practices.
One of the cornerstones of sustainable manufacturing is the integration of eco-friendly technologies that minimize environmental impact across every stage of the production lifecycle. These technologies range from renewable energy systems and clean process innovations to closed-loop recycling mechanisms and digital monitoring tools. When deployed effectively, such innovations not only reduce the strain on natural resources but also enhance operational efficiency, enabling businesses to achieve greater output with fewer inputs.
Waste minimization plays a critical role in this transformation. By adopting lean manufacturing, additive manufacturing, and circular economy models, companies can significantly lower material usage and extend the lifespan of components and products. Furthermore, by reusing by-products or remanufacturing used goods, industries move toward a more regenerative model of production that aligns with nature’s cyclical patterns rather than linear consumption models.
Energy use is another domain where sustainable manufacturing has a profound impact. The shift from fossil fuels to solar, wind, biomass, and geothermal energy helps manufacturers decouple growth from carbon emissions. Additionally, technologies like smart grids, advanced energy storage, and AI-powered predictive analytics optimize energy flows in real time, reducing operational costs while meeting sustainability targets.
Social responsibility is also deeply intertwined with sustainable manufacturing. Ethical sourcing, fair labor practices, and community engagement are key elements that ensure the well-being of workers and local populations. This holistic approach acknowledges that long-term industrial success depends on more than profitability—it requires trust, transparency, and equitable treatment of stakeholders throughout the supply chain.
As global priorities shift toward climate resilience, regulatory compliance, and sustainable development, companies that embrace sustainable manufacturing are better positioned to navigate emerging challenges and seize new market opportunities. Consumers are increasingly favoring environmentally responsible brands, and investors are prioritizing companies with robust environmental, social, and governance (ESG) strategies. As a result, sustainable practices are becoming both a moral imperative and a competitive advantage.
Looking forward, the continuous evolution of enabling technologies—such as blockchain for supply chain transparency, IoT for resource tracking, and AI for decision-making—will further enhance the effectiveness of sustainable manufacturing. Moreover, collaboration among governments, industries, and academic institutions will be essential for scaling these practices globally and ensuring their accessibility to small and medium enterprises.
In conclusion, sustainable manufacturing is not a temporary trend but a foundational principle for future industrial development. By embedding sustainability into design, production, logistics, and corporate governance, manufacturers contribute to a circular, inclusive, and low-carbon economy. These efforts not only benefit the planet but also create value for shareholders, employees, and society at large—ensuring long-term resilience in an increasingly resource-constrained world.
Frequently Asked Questions
1. What is sustainable manufacturing?
2. How does sustainable manufacturing differ from traditional manufacturing?
3. What are the main pillars or dimensions of sustainable manufacturing?
4. Which key strategies can factories use to make their operations more sustainable?
5. How do Industry 4.0 and digital technologies support sustainable manufacturing?
6. What is the role of life-cycle thinking and eco-design in sustainable manufacturing?
7. How can companies measure sustainability performance in manufacturing?
8. Does sustainable manufacturing always increase costs?
Sustainable Manufacturing: Comprehensive Student Exercises
Core Concept Review Modules
1. What is sustainable manufacturing, and why is it crucial for modern industries?
2. How can energy efficiency be achieved in manufacturing operations?
3. What role does waste reduction play in sustainable production systems?
4. How can renewable energy sources be integrated into industrial facilities?
5. What are the key principles of Green Supply Chain Management (GSCM)?
6. What are the core benefits of a Circular Economy model in manufacturing?
7. What main challenges arise when adopting sustainable manufacturing practices?
8. How does Life Cycle Assessment (LCA) support eco-friendly engineering?
Analytical & Strategic Thought Scenarios
1. Scenario: Bio-Based Polymers vs. Recyclable Engineering Plastics
2. Scenario: Decarbonizing High-Temperature Industrial Thermal Processes
3. Scenario: Closed-Loop Solvent Recovery in Pharmaceutical Synthesis
4. Scenario: Zero-Water-Discharge (ZWD) Systems in Electronics Manufacturing
5. Scenario: Extended Producer Responsibility (EPR) in Lithium-Ion Battery Manufacturing
6. Scenario: Microgrid Architecture for Net-Zero Industrial Parks
7. Scenario: Additive Manufacturing vs. Subtractive Machining Life Cycle Footprint
8. Scenario: AI-Driven Energy Peak Shaving in Heavy Stamping Facilities
9. Scenario: Scope 1, 2, and 3 Carbon Accounting in Global Supply Networks
Quantitative & Mathematical Calculations
Work through these step-by-step mathematical problems to master quantitative environmental engineering in sustainable manufacturing, carbon footprint modeling, waste heat thermodynamics, solar array sizing, water recycling economics, and affinity-law fan energy throttling.
Problem 1: Life Cycle Carbon Footprint Reduction via Material Substitution
Problem Statement: An automotive stamping plant produces \(100{,}000\,\text{structural brackets}\) annually.
• Option A (Conventional Steel): Weight = \(4.5\,\text{kg/part}\). Embodied carbon of virgin steel = \(2.1\,\text{kg CO}_2\text{e/kg}\). Manufacturing energy = \(3.0\,\text{kWh/part}\) (grid emission factor = \(0.50\,\text{kg CO}_2\text{e/kWh}\)).
• Option B (Recycled Aluminum): Weight = \(2.8\,\text{kg/part}\). Embodied carbon of recycled aluminum = \(1.6\,\text{kg CO}_2\text{e/kg}\). Manufacturing energy = \(4.2\,\text{kWh/part}\) (grid emission factor = \(0.50\,\text{kg CO}_2\text{e/kWh}\)).
Calculate total annual carbon emissions for both options and determine net annual carbon savings in metric tons.
Step 1: Calculate Emissions for Option A (Steel)
$$\text{Embodied Carbon}_A = 4.5\,\text{kg} \times 2.1\,\frac{\text{kg CO}_2\text{e}}{\text{kg}} = 9.45\,\text{kg CO}_2\text{e/part}$$
$$\text{Energy Carbon}_A = 3.0\,\text{kWh} \times 0.50\,\frac{\text{kg CO}_2\text{e}}{\text{kWh}} = 1.50\,\text{kg CO}_2\text{e/part}$$
$$\text{Total Carbon}_A = 9.45 + 1.50 = 10.95\,\text{kg CO}_2\text{e/part}$$
$$\text{Annual Carbon}_A = 100{,}000 \times 10.95 = 1{,}095{,}000\,\text{kg CO}_2\text{e} = \mathbf{1{,}095.00\,\text{Metric Tons CO}_2\text{e}}$$
Step 2: Calculate Emissions for Option B (Recycled Aluminum)
$$\text{Embodied Carbon}_B = 2.8\,\text{kg} \times 1.6\,\frac{\text{kg CO}_2\text{e}}{\text{kg}} = 4.48\,\text{kg CO}_2\text{e/part}$$
$$\text{Energy Carbon}_B = 4.2\,\text{kWh} \times 0.50\,\frac{\text{kg CO}_2\text{e}}{\text{kWh}} = 2.10\,\text{kg CO}_2\text{e/part}$$
$$\text{Total Carbon}_B = 4.48 + 2.10 = 6.58\,\text{kg CO}_2\text{e/part}$$
$$\text{Annual Carbon}_B = 100{,}000 \times 6.58 = 658{,}000\,\text{kg CO}_2\text{e} = \mathbf{658.00\,\text{Metric Tons CO}_2\text{e}}$$
Step 3: Calculate Annual Net Carbon Abatement
$$\Delta \text{CO}_2\text{e} = 1{,}095.00 - 658.00 = \mathbf{437.00\,\text{Metric Tons CO}_2\text{e/year}} \quad (39.91\%\text{ reduction})$$
Engineering Interpretation: Lightweighting coupled with secondary material recycling achieves an annual abatement of \(437.00\,\text{MT CO}_2\text{e}\), reducing Scope 3 supply chain footprints substantially.
Problem 2: Waste Heat Recovery Boiler (WHRB) Economics and Payback
Problem Statement: An industrial glass manufacturing furnace discharges exhaust gas at \(450^\circ\text{C}\). A Waste Heat Recovery Boiler (WHRB) captures flue gas thermal energy, displacing \(1{,}800{,}000\,\text{kWh/year}\) of natural gas heating fuel. Natural gas costs \(\$0.06/\text{kWh}\). Capital equipment and installation cost is \(\$216{,}000\), with annual maintenance costs of \(\$10{,}800\). Determine net annual fuel savings and the simple payback period in years.
Step 1: Calculate Gross Fuel Cost Savings
$$\text{Gross Savings} = 1{,}800{,}000\,\text{kWh} \times \$0.06/\text{kWh} = \$108{,}000.00/\text{year}$$
Step 2: Calculate Net Annual Operating Savings
$$\text{Net Savings} = \text{Gross Savings} - \text{Maintenance} = \$108{,}000 - \$10{,}800 = \mathbf{\$97{,}200.00/\text{year}}$$
Step 3: Calculate Simple Payback Period
$$\text{Payback} = \frac{\text{Capital Cost}}{\text{Net Annual Savings}} = \frac{\$216{,}000}{\$97{,}200} = \mathbf{2.22\,\text{years}} \quad (\approx 26.7\,\text{months})$$
Engineering Interpretation: A payback period of \(2.22\,\text{years}\) easily satisfies corporate hurdle rates (<3 years), providing ongoing annual operating cash savings of \(\$97{,}200\) while reducing thermal flue emissions.
Problem 3: Rooftop Solar Photovoltaic (PV) Generation & Carbon Offset
Problem Statement: A facility installs a \(500\,\text{kWp}\) rooftop solar PV array with specific yield of \(1{,}400\,\text{kWh/kWp per year}\). Grid electricity costs \(\$0.12/\text{kWh}\), with an average utility grid emission factor of \(0.62\,\text{kg CO}_2\text{e/kWh}\). Compute annual generation (\(\text{kWh}\)), annual utility bill reductions (\(\$\)), and avoided greenhouse gas emissions (\(\text{Metric Tons CO}_2\text{e}\)).
Step 1: Calculate Annual Clean Electricity Generation
$$E_{\text{solar}} = 500\,\text{kWp} \times 1{,}400\,\frac{\text{kWh}}{\text{kWp}\cdot\text{year}} = \mathbf{700{,}000.0\,\text{kWh/year}}$$
Step 2: Calculate Annual Utility Cost Savings
$$\text{Savings} = 700{,}000\,\text{kWh} \times \$0.12/\text{kWh} = \mathbf{\$84{,}000.00/\text{year}}$$
Step 3: Calculate Annual Carbon Offsets
$$\text{CO}_2\text{e}_{\text{avoided}} = 700{,}000\,\text{kWh} \times 0.62\,\frac{\text{kg CO}_2\text{e}}{\text{kWh}} = 434{,}000\,\text{kg CO}_2\text{e} = \mathbf{434.00\,\text{Metric Tons CO}_2\text{e/year}}$$
Engineering Interpretation: The system eliminates \(434\,\text{MT}\) of Scope 2 emissions annually while buffering the manufacturing plant against volatile wholesale electrical grid price spikes.
Problem 4: Closed-Loop Industrial Water Recycling Efficiency
Problem Statement: A textile wet-finishing plant consumes \(80{,}000\,\text{liters/hour}\) of freshwater over an \(18\text{-hour}\) daily operating shift. A membrane bioreactor (MBR) and reverse osmosis (RO) system recovers \(85\%\) of wastewater for reuse. Municipal intake water costs \(\$2.50/\text{m}^3\) and sewer discharge fees are \(\$1.80/\text{m}^3\) (\(1\,\text{m}^3 = 1{,}000\,\text{liters}\)). Compute daily and annual water management cost savings assuming \(300\,\text{operating days/year}\).
Step 1: Calculate Daily Baseline Consumption
$$V_{\text{daily}} = 80{,}000\,\frac{\text{L}}{\text{h}} \times 18\,\text{h} = 1{,}440{,}000\,\text{L/day} = 1{,}440.0\,\text{m}^3/\text{day}$$
Step 2: Calculate Recovered Water Volume (85%)
$$V_{\text{recovered}} = 1{,}440.0\,\text{m}^3 \times 0.85 = \mathbf{1{,}224.0\,\text{m}^3/\text{day}}$$
Step 3: Combined Unit Tariff (Intake + Discharge Avoidance)
$$\text{Tariff} = \$2.50 + \$1.80 = \$4.30/\text{m}^3$$
Step 4: Calculate Daily and Annual Financial Savings
$$\text{Savings}_{\text{daily}} = 1{,}224.0\,\text{m}^3 \times \$4.30/\text{m}^3 = \mathbf{\$5{,}263.20/\text{day}}$$
$$\text{Savings}_{\text{annual}} = \$5{,}263.20/\text{day} \times 300\,\text{days} = \mathbf{\$1{,}578{,}960.00/\text{year}}$$
Engineering Interpretation: Conserving \(1{,}224\,\text{m}^3\) daily generates \(\$1.58\,\text{million}\) in annual operating savings while protecting local watershed reserves from industrial drawdown.
Problem 5: Buy-to-Fly Ratio and Raw Material Scrap in Additive Manufacturing
Problem Statement: An aerospace facility manufactures \(250\,\text{structural titanium brackets}\) annually (final weight = \(2.2\,\text{kg/part}\)).
• Subtractive CNC Milling: Requires a solid billet of \(18.0\,\text{kg/part}\). Billet cost = \(\$45.00/\text{kg}\). Swarf recycling buyback credit = \(\$5.00/\text{kg}\).
• Additive Manufacturing (3D Printing): Consumes \(2.6\,\text{kg}\) of gas-atomized titanium powder per part at \(\$110.00/\text{kg}\). Unused powder recycling recovery efficiency is \(92\%\).
Calculate Buy-to-Fly ratios for both processes and total annual raw material savings using 3D printing.
Step 1: Calculate Buy-to-Fly Ratios
$$\text{BTF}_{\text{CNC}} = \frac{18.0\,\text{kg}}{2.2\,\text{kg}} = \mathbf{8.18 : 1}$$
$$\text{BTF}_{\text{3D}} = \frac{2.6\,\text{kg}}{2.2\,\text{kg}} = \mathbf{1.18 : 1}$$
Step 2: Net Material Cost for Subtractive CNC
$$\text{Billet Cost} = 18.0\,\text{kg} \times \$45.00 = \$810.00$$
$$\text{Scrap Credit} = (18.0 - 2.2)\,\text{kg} \times \$5.00 = 15.8\,\text{kg} \times \$5.00 = \$79.00$$
$$\text{Net Cost}_{\text{CNC}} = \$810.00 - \$79.00 = \$731.00/\text{part}$$
Step 3: Net Material Cost for Additive Manufacturing
$$\text{Initial Powder Input} = 2.6\,\text{kg} \times \$110.00 = \$286.00$$
$$\text{Recovered Powder Value} = (2.6 - 2.2)\,\text{kg} \times 0.92 \times \$110.00 = 0.368\,\text{kg} \times \$110.00 = \$40.48$$
$$\text{Net Cost}_{\text{3D}} = \$286.00 - \$40.48 = \$245.52/\text{part}$$
Step 4: Annual Raw Material Financial Savings (250 Parts)
$$\Delta \text{Cost} = \$731.00 - \$245.52 = \$485.48/\text{part}$$
$$\text{Savings}_{\text{annual}} = 250 \times \$485.48 = \mathbf{\$121{,}370.00/\text{year}}$$
Engineering Interpretation: Additive near-net-shape deposition eliminates over \(3.9\,\text{metric tons}\) of raw titanium billet extraction and machining swarf annually, yielding \(\$121{,}370\) in direct material savings.
Problem 6: Variable Frequency Drive (VFD) Fan Throttling via Affinity Laws
Problem Statement: A factory cleanroom ventilation system runs a \(75.0\,\text{kW}\) centrifugal fan motor \(8{,}000\,\text{hours/year}\). A Variable Frequency Drive (VFD) is installed, allowing fan speed to be reduced to \(80\%\) of full flow during unpopulated off-peak shifts (\(4{,}000\,\text{hours/year}\)). According to Turbomachinery Affinity Laws, power scales with the cube of speed: \(P_2 = P_1 (N_2 / N_1)^3\). Electricity costs \(\$0.10/\text{kWh}\). Calculate annual energy savings in \(\text{kWh}\) and annual utility cost savings.
Step 1: Power Consumption at 80% Rotational Speed
$$P_{80\%} = 75.0\,\text{kW} \times (0.80)^3 = 75.0 \times 0.512 = \mathbf{38.40\,\text{kW}}$$
Step 2: Instantaneous Power Reduction During Throttled Hours
$$\Delta P = 75.0\,\text{kW} - 38.40\,\text{kW} = \mathbf{36.60\,\text{kW}}$$
Step 3: Annual Energy Savings Integration (4,000 Hours)
$$E_{\text{saved}} = 36.60\,\text{kW} \times 4{,}000\,\text{h} = \mathbf{146{,}400.0\,\text{kWh/year}}$$
Step 4: Annual Financial Savings Resolution
$$\text{Savings} = 146{,}400\,\text{kWh} \times \$0.10/\text{kWh} = \mathbf{\$14{,}640.00/\text{year}}$$
Engineering Interpretation: Due to cubic affinity scaling, reducing fan speed by just \(20\%\) slashes electrical power draw by \(48.8\%\), saving \(\$14{,}640\) annually on a single motor drive.