
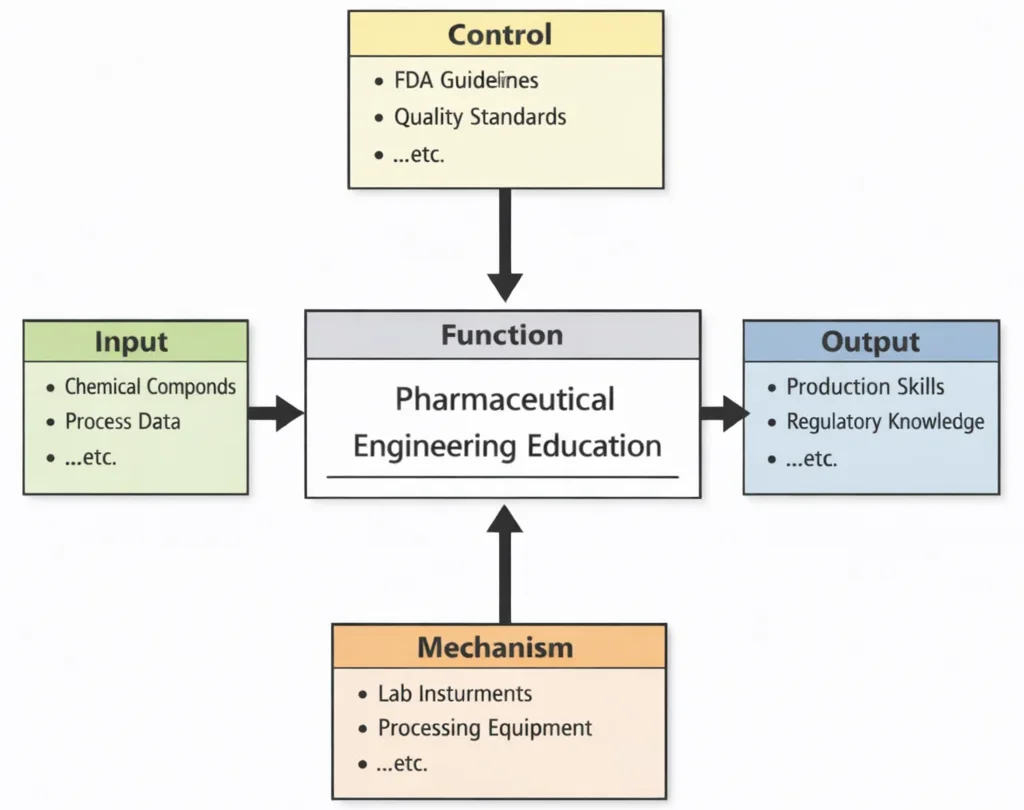
IDEF0 functional decomposition of pharmaceutical engineering education: raw chemical/biologic inputs governed by GMP and regulatory guidelines, operationalized through process analytical technology and unit operation pilot equipment to generate validated manufacturing competencies.
Pharmaceutical Engineering Education, as shown in this IDEF0 diagram, functions as a disciplined “conversion process” that turns scientific and industrial Inputs into real-world engineering competence. Students begin with Inputs such as chemical compounds and process data—what a drug is made from, and how it behaves during mixing, reaction, separation, drying, granulation, or filling. Their learning is guided by Controls like FDA guidelines and quality standards, which act as firm guardrails: they define what counts as safe, reproducible, traceable, and acceptable for patients and regulators. The transformation is enabled by Mechanisms—lab instruments and processing equipment—through which students learn to measure, validate, and scale up processes rather than merely describe them. The Outputs are the capabilities that matter in practice: production skills and regulatory knowledge, meaning graduates can design or operate manufacturing steps, identify sources of variability, implement quality-by-design thinking, and defend decisions with evidence and compliance awareness—so medicines can be produced consistently, safely, and at scale.
Pharmaceutical Engineering bridges chemical engineering principles with biomedical science to design, optimize, and scale up processes for producing therapeutic drugs and delivery systems. It complements the broader field of Biomedical Engineering by focusing on the molecular and process-level aspects of pharmaceutical production. With growing interest in personalized medicine, integration with Bioinformatics allows pharmaceutical engineers to tailor drug formulations based on genomic and proteomic data.
A key concern in drug development is biocompatibility, which draws from expertise in Biomaterials to ensure safe interaction with human tissues. Understanding mechanical interactions, such as drug-eluting stents or inhalers, relies on concepts from Biomechanics. Signal transduction in targeted delivery systems often incorporates methods from Biomedical Signal Processing to guide precision therapy.
Innovations in Cardiovascular Engineering have informed pharmaceutical research in anticoagulants and lipid-lowering agents, while Clinical Engineering ensures that pharmaceutical delivery devices operate reliably in hospital settings. Diagnosis-driven pharmacology also relies on tools developed in Medical Imaging, enabling targeted treatment for cancer, infections, and metabolic disorders.
Recent advancements in Neural Engineering contribute to the development of neuropharmaceuticals, such as mood stabilizers and anti-epileptics. Recovery and functional rehabilitation are supported by synergy with Rehabilitation Engineering, especially for drug-assisted therapy. Tissue regeneration techniques, as studied in Tissue Engineering and Regenerative Medicine, are frequently combined with controlled drug release systems.
Pharmaceutical processes rely on a solid foundation in Chemical Engineering, particularly in understanding thermodynamics, transport phenomena, and reactor design. Biochemical Engineering plays a crucial role in synthesizing bioactive compounds and scaling up fermentation processes for antibiotics, hormones, and vaccines. Meanwhile, reaction optimization is guided by Chemical Catalysis and Reaction Engineering.
Energy consumption in manufacturing is optimized through Chemical Energy Systems Engineering, while material stability and packaging rely on Chemical Materials Engineering. Large-scale production lines are designed and managed using techniques from Chemical Process Engineering. Modeling pharmacokinetics and molecular dynamics benefits from Computational Chemical Engineering.
The increasing convergence of food and medicine—nutraceuticals and drug delivery via food matrices—draws parallels with Food and Beverage Engineering. Emerging therapies based on nano-encapsulation and smart drug carriers are driven by progress in Nanotechnology in Chemical Engineering. Additionally, innovations in Polymer and Plastics Engineering enable the development of bioresorbable capsules and advanced drug containers.
Beyond lab design, Civil Engineering contributes to the infrastructure for pharmaceutical cleanrooms and production facilities. The logistics and development of pharmaceutical campuses involve close coordination with Construction Management. Finally, ensuring continuous production and access to critical medicines during crises involves strategies from Earthquake and Disaster Engineering, particularly for emergency stockpiling and resilient supply chains.
Automated continuous pharmaceutical manufacturing suite featuring inline spectroscopic Process Analytical Technology (PAT), robotic filling modules, and computational molecular optimization.
This image portrays pharmaceutical engineering as a meeting point between laboratory research and industrial-scale drug production. In the foreground, engineers and scientists review data on a large digital tablet beside capsules and lab glassware, suggesting formulation work, quality testing, and process control. The mid-ground shows stainless-steel vessels, pipelines, and controlled production areas typical of modern pharmaceutical plants, while robotic systems and automated modules hint at high-throughput manufacturing and sterile operations. Above a central platform, a glowing DNA helix and molecular graphics represent the scientific foundations behind drug design and biomolecular therapies. The surrounding overlays—chemical structures, charts, and hexagonal “molecule” motifs—reinforce themes of precision, regulation, and data-driven optimization. Overall, the scene communicates how pharmaceutical engineers design and manage processes that ensure medicines are consistent, effective, and produced safely at scale.
Biomedical Engineering – Knowledge Map
Pharmaceutical Engineering (Current Page)
Centres on formulating, scaling up, and delivering therapeutic agents with precise control over dosage, release timing, and biological safety.
Bioinformatics
Identifies molecular drug targets and models pharmacokinetic interactions through large-scale analysis of genomic and proteomic databases.
Biomaterials
Enables engineered polymer matrices, hydrogels, and liposomal carriers that regulate drug release kinetics and biological tissue compatibility.
Cardiovascular Engineering
Represents key therapeutic targets where drug formulations directly regulate blood pressure, clotting cascades, and vascular tone.
Neural Engineering
Involves targeted neuropharmaceutical delivery across the blood-brain barrier to modulate synaptic signaling pathways and treat central nervous system disorders.
Medical Imaging
Tracks spatial biodistribution, nanocarrier accumulation, and localized drug clearance rates in vivo using contrast-enhanced PET, MRI, and CT imaging.
Biomedical Signal Processing
Interprets real-time physiological response signals (ECG, EEG, continuous glucose) to evaluate drug efficacy and calibrate automated infusion pumps.
Rehabilitation Engineering
Combines pharmacotherapeutic anti-spasticity or pain-management regimes with physical assistive devices to optimize post-trauma recovery.
Clinical Engineering
Manages pharmaceutical delivery equipment, sterile compounding isolators, and infusion hardware within hospital networks.
Tissue Engineering & Regenerative Medicine
Integrates growth-factor drug delivery into cellular scaffolds to stimulate organized tissue regeneration and organ repair.
Biomechanics
Analyzes how physiological fluid flow and tissue shear stress govern drug distribution, dissolution, and transport across biological membranes.
Biomedical Engineering – Overview
Serves as the overarching umbrella discipline uniting molecular therapeutics, medical devices, and physiological modeling to transform healthcare.
Core Areas of Pharmaceutical Engineering
Drug Development and Formulation
- Definition: The comprehensive process of turning active pharmaceutical ingredients (APIs) into safe, stable, and effective drug products for patient use.
- Key Processes:
- Preformulation Studies: Includes intrinsic solubility evaluation, solid-state polymorphism characterization (via pXRD and DSC), and excipient compatibility testing to avoid chemical degradation.
- Formulation Development: Crafting optimal mixtures of APIs and functional excipients (binders, superdisintegrants, glidants, film coatings) to maximize oral bioavailability, physical stability, and mechanical manufacturability.
- Dosage Forms: Encompasses immediate-release tablets, multi-particulate capsules, sterile parenterals, lyophilized cakes, transdermal patches, and long-acting depot suspensions.
Drug Delivery Systems
- Definition: Advanced technologies engineered to deliver medications precisely to target tissues, improving efficacy and reducing systemic toxicity.
- Types:
- Oral Delivery: Immediate-release tablets, enteric-coated matrices resisting gastric acidity (\(\text{pH } 1.2\)), and osmotic pump systems providing continuous zero-order delivery.
- Injectable Systems: Intravenous solutions, intramuscular depot microspheres, and subcutaneous autoinjectors delivering concentrated biologics.
- Transdermal Patches: Matrix-diffusion and reservoir-membrane systems delivering lipophilic compounds across the stratum corneum at constant flux.
- Nanoparticle Carriers: Ionizable lipid nanoparticles (LNPs), PEGylated liposomes, and polymeric micelles designed for target cell endocytosis and EPR tumor microvasculature permeation.
- Controlled Release Systems: Bioerodible PLGA matrices and hydrogel swelling systems maintaining therapeutic plasma levels across weeks or months.
Process Development and Scale-Up
- Definition: Engineering protocols to transition drug manufacturing from laboratory to industrial scale while maintaining quality and efficiency.
- Key Elements:
- Chemical Synthesis: Developing scalable, stereoselective reaction routes with minimized solvent footprints and high atom economy.
- Process Optimization: Leveraging Design of Experiments (DoE) and response surface methodology to maximize reaction yield and crystallizer purity.
- Pilot Plant Operations: Intermediate-scale validation to quantify impeller shear rates, drying kinetics, and flowability before commercial batch execution.
Manufacturing Technologies
- Definition: Adoption of state-of-the-art production methodologies geared toward efficient, quality-controlled pharmaceutical manufacturing.
- Techniques:
- Batch Manufacturing: Traditional multi-stage production characterized by step-wise hold periods, manual sampling, and discrete lot traceability.
- Continuous Manufacturing: Integrated processing where raw materials continuously enter loss-in-weight feeders, twin-screw granulators, and rotary presses under steady-state control.
- Bioprocessing: Cultivating recombinant mammalian cells (CHO lines) in fed-batch or perfusion bioreactors, followed by Protein A affinity chromatography and nanofiltration viral clearance.
Quality Control and Assurance
- Definition: Systematic strategies to ensure pharmaceutical products consistently meet regulatory and safety standards.
- Processes:
- Good Manufacturing Practices (GMP): International operational standards governing HVAC particulate counts, water for injection (WFI) loop sterility, and data integrity.
- Process Analytical Technology (PAT): In-line, on-line, and at-line spectroscopic sensors (NIR, Raman, FBRM) measuring moisture, API blend uniformity, and crystal chord size distribution in real time.
- Validation and Verification: Installation, Operational, and Performance Qualification (IQ/OQ/PQ) proving deterministic control across critical process parameters (CPPs).
Regulatory Compliance
- Definition: Ensuring adherence to legal, ethical, and international standards throughout the drug life cycle.
- Regulatory Bodies:
- Food and Drug Administration (FDA): U.S. federal oversight governing IND, NDA, and BLA approval frameworks.
- European Medicines Agency (EMA): Centralized scientific evaluation and marketing authorization across the European Union.
- World Health Organization (WHO): Establishes global pharmacopeial standards and international prequalification programs.
- Compliance Aspects:
- 21 CFR Part 11 compliant audit trails, electronic signatures, and batch production records.
- ICH Q8 (Pharmaceutical Development), Q9 (Quality Risk Management), and Q10 (Pharmaceutical Quality System) implementation.
Emerging Trends and Innovations
- Personalized Medicine: Utilizing pharmacogenomic testing and point-of-care micro-compounding to tailor drug regimens to specific CYP450 metabolic genotypes.
- 3D Printed Pharmaceuticals: Drop-on-powder and fused-filament printing of patient-specific polypills combining multiple active compounds into programmed dissolution geometries.
- Smart Drug Delivery: Closed-loop microfluidic pumps modulated by continuous biosensors (e.g., automated artificial pancreas systems).
Industry Impact and Collaboration
- Pharmaceutical engineers accelerate global availability of vaccines, low-cost generics, and biosimilars through modular, scalable continuous synthesis.
- Academic-industrial partnerships bridge fundamental molecular discoveries with automated, sterile fill-finish operations.
Applications of Pharmaceutical Engineering
Advanced Drug Formulations
- Controlled-Release Systems:
- Engineered to release active ingredients gradually over hours, days, or weeks, maintaining plasma concentrations within the therapeutic window.
- Common mechanisms include elementary osmotic pumps, hydrophilic HPMC matrix tablets, and PLGA subcutaneous depots.
- Mathematical kinetic modeling balances polymer hydrolysis, diffusion coefficients, and tablet erosion dynamics.
- Targeted Drug Delivery:
- Directing toxic therapeutic agents specifically to diseased tissues using functionalized ligands, avoiding healthy cellular damage.
- Technologies include antibody-drug conjugates (ADCs) with cleavable linkers, magnetic nanoparticles, and pH-sensitive liposomes.
- Drastically expands the therapeutic index of high-potency oncolytic chemotherapeutics.
- Combination Therapies:
- Fixed-dose combinations co-formulating multiple synergistic APIs inside multi-layer tablets or coated pellets.
- Overcomes physical drug-drug chemical incompatibilities through barrier coats and differential release profiles.
Biopharmaceuticals and Biologics
- Definition: Complex, high-molecular-weight therapeutics derived from living biological systems, including monoclonal antibodies, fusion proteins, and mRNA vaccines.
- Manufacturing:
- Upstream fed-batch or perfusion cultivation in single-use bioreactors with automated dissolved oxygen and pH feedback.
- Downstream purification utilizing multi-column continuous chromatography (MCC) and tangential flow filtration (TFF).
- Formulation stabilization using polysorbate surfactants, trehalose cryoprotectants, and histidine buffer matrices to prevent protein aggregation.
- Examples: Monoclonal IgG antibodies treating autoimmune disorders, and lipid-nanoparticle-encapsulated mRNA platforms.
Vaccine Production
- Applications: High-throughput, sterile biomanufacturing of viral vector, recombinant subunit, and mRNA vaccines.
- Formulation Technologies: Adjuvant emulsion synthesis (e.g., squalene-based MF59) and sub-zero lyophilization to maintain shelf life across global cold-chains.
Personalized Medicine
- Definition: Designing custom therapeutic interventions matched to patient-specific genomic, proteomic, and metabolic biomarkers.
- Technologies: Automated dispensing systems, digital drop-on-demand printing, and point-of-care sterile compounding isolators.
Nanomedicine
- Applications: Nanoscale colloidal systems (\(50\text{--}200\,\text{nm}\)) overcoming systemic clearance by the reticuloendothelial system (RES).
- Benefits: Solubilizes poorly water-soluble BCS Class II/IV APIs, enables passive tumor targeting via the EPR effect, and permits multi-modal theranostic imaging.
Cell and Gene Therapy
- Definition: Ex vivo and in vivo genetic interventions that permanently repair defective genetic alleles or reprogram autologous immune cells.
- Applications: CAR-T cell manufacturing using closed automated cell-processing systems (e.g., Prodigy/Cocoon), and recombinant adeno-associated viral (rAAV) vector synthesis.
Contemporary 2026 AI-Era Computational Paradigms in Pharmaceutical Engineering
Modern pharmaceutical process engineering integrates transport phenomena with deep learning to optimize unit operations and eliminate trial-and-error experimental cycles:
- Physics-Informed Neural Networks (PINNs) for Hot-Melt Extrusion & Fluid Bed Drying: PINNs solve coupled non-Newtonian Navier-Stokes equations and Fickian heat/mass transfer models directly across complex extruder geometries: $$\mathcal{L}_{\text{PINN}} = \left\| \rho \left( \frac{\partial \mathbf{u}}{\partial t} + (\mathbf{u}\cdot\nabla)\mathbf{u} \right) + \nabla p - \nabla \cdot \left( \eta(\dot{\gamma}, T) \left[ \nabla \mathbf{u} + (\nabla \mathbf{u})^T \right] \right) \right\|^2 + \lambda \left\| \rho C_p \left( \frac{\partial T}{\partial t} + \mathbf{u}\cdot\nabla T \right) - k_{\text{th}}\nabla^2 T - \dot{q}_{\text{visc}} \right\|^2$$ where \(\eta(\dot{\gamma}, T)\) is the temperature- and shear-rate-dependent Carreau-Yasuda viscosity model. This enables real-time optimization of polymer-API melt temperature profiles without mesh-dependent CFD grid generation.
- DeepONets & Neural Operators for Bioreactor Kinetics: Deep Operator Networks learn the non-linear functional mapping from dynamic nutrient feed schedules directly to continuous protein glycosylation profiles, solving multi-variable metabolic differential equations up to 5,000 times faster than Runge-Kutta numerical solvers.
- Edge Machine Learning for Inline PAT Quality-by-Design (QbD): High-throughput convolutional autoencoders process live Raman and NIR hyperspectral imaging directly on FPGA hardware at the die-feed face, predicting tablet API content uniformity and crushing hardness within \(5\,\text{ms}\), automatically diverting out-of-spec compacts via high-speed pneumatic reject gates.
Worked Engineering Calculation: Multi-Scale Impeller Agitation & Bioreactor Power Scaling
Analytical Engineering Derivation: Geometric & Dynamic Scale-Up of an API Crystallizer
Problem Formulation: A pilot-scale pharmaceutical crystallizer (Tank 1) with liquid volume \(V_1 = 0.10\,\text{m}^3\) and impeller diameter \(D_1 = 0.25\,\text{m}\) operates at an agitation speed of \(N_1 = 300\,\text{rpm}\). The pharmaceutical slurry has a dynamic viscosity of \(\mu = 0.0025\,\text{Pa}\cdot\text{s}\) and a fluid density of \(\rho = 1050\,\text{kg/m}^3\). The impeller is a standard pitched-blade turbine with an empirical turbulent Power Number of \(N_p = 1.27\).
- Calculate the impeller Reynolds number (\(\text{Re}_1\)) and power consumption (\(P_1\)) of the pilot vessel in Watts.
- Scale up the crystallizer to an industrial production vessel (Tank 2) with volume \(V_2 = 12.5\,\text{m}^3\) assuming geometric similarity (where linear scale factor \(\lambda = (V_2 / V_1)^{1/3}\)).
- Determine the required industrial impeller diameter (\(D_2\)), operational speed (\(N_2\)), and motor power (\(P_2\)) assuming the scale-up criterion maintains constant volumetric power dissipation (\(P / V = \text{constant}\)), which preserves identical secondary crystal nucleation rates.
Step 1: Pilot Vessel Reynolds Number & Power Evaluation
Convert impeller rotational speed to revolutions per second:
$$N_1 = \frac{300\,\text{rpm}}{60\,\text{s/min}} = 5.0\,\text{s}^{-1}$$
$$\text{Re}_1 = \frac{\rho N_1 D_1^2}{\mu} = \frac{(1050\,\text{kg/m}^3) \times (5.0\,\text{s}^{-1}) \times (0.25\,\text{m})^2}{0.0025\,\text{Pa}\cdot\text{s}} = \frac{328.125}{0.0025} = \mathbf{1.3125 \times 10^5}$$
Because \(\text{Re}_1 \gt 10{,}000\), the mixing regime is fully turbulent, and \(N_p\) remains constant at \(1.27\).The power drawn is governed by:
$$\begin{aligned}
P_1 &= N_p \, \rho \, N_1^3 \, D_1^5 \\
&= 1.27 \times (1050\,\text{kg/m}^3) \times (5.0\,\text{s}^{-1})^3 \times (0.25\,\text{m})^5 \\
&= 1.27 \times 1050 \times 125 \times 0.00097656 = \mathbf{162.74\,\text{Watts}}
\end{aligned}$$
Volumetric power density:
$$\left(\frac{P}{V}\right)_1 = \frac{162.74\,\text{W}}{0.10\,\text{m}^3} = \mathbf{1627.4\,\text{W/m}^3}$$
Step 2: Calculate Geometric Scale Factor and Large Vessel Diameter
$$\lambda = \left(\frac{V_2}{V_1}\right)^{1/3} = \left(\frac{12.5\,\text{m}^3}{0.10\,\text{m}^3}\right)^{1/3} = (125)^{1/3} = 5.0$$
$$D_2 = \lambda \times D_1 = 5.0 \times 0.25\,\text{m} = \mathbf{1.25\,\text{m}}$$
Step 3: Calculate Scaled Impeller Speed and Total Motor Power
Under constant power per unit volume (\(P / V = \text{constant}\)):
$$\frac{P_2}{V_2} = \frac{P_1}{V_1} \quad \Rightarrow \quad P_2 = P_1 \left(\frac{V_2}{V_1}\right) = 162.74\,\text{W} \times 125 = \mathbf{20{,}342.5\,\text{W}} \approx \mathbf{20.34\,\text{kW}}$$To determine the required rotational speed \(N_2\):
$$\frac{P_2}{P_1} = \left(\frac{N_2}{N_1}\right)^3 \left(\frac{D_2}{D_1}\right)^5 \quad \Rightarrow \quad 125 = \left(\frac{N_2}{N_1}\right)^3 (5.0)^5 = \left(\frac{N_2}{N_1}\right)^3 \times 3125$$
$$\left(\frac{N_2}{N_1}\right)^3 = \frac{125}{3125} = \frac{1}{25} = 0.040$$
$$\frac{N_2}{N_1} = (0.040)^{1/3} \approx 0.341995$$
$$N_2 = 5.0\,\text{s}^{-1} \times 0.341995 = 1.710\,\text{s}^{-1} \quad \Rightarrow \quad N_2 = 1.710 \times 60 \approx \mathbf{102.6\,\text{rpm}}$$
Physical Interpretation & Design Implication:
While maintaining constant \(P/V\) guarantees identical macro-mixing energy dissipation, the impeller tip speed increases from \(v_{\text{tip},1} = \pi N_1 D_1 = 3.93\,\text{m/s}\) to \(v_{\text{tip},2} = \pi N_2 D_2 = 6.72\,\text{m/s}\). This \(71\%\) elevation in maximum tip speed significantly increases local shear stress (\(\tau_{\max} \propto N D\)), which could cause crystal attrition or protein denaturation. In shear-sensitive biopharmaceutical crystallization, engineers must adjust scale-up rules toward constant tip speed or maximum shear stress rather than constant volumetric power.
Systems Engineering Trade-Off Analysis in Pharmaceutical Processing
Designing robust pharmaceutical manufacturing pipelines requires balancing physical transport phenomena, formulation stability, economic throughput, and regulatory validation:
| Unit Operation / Domain | Parameter Dimension A | Parameter Dimension B | Critical Multi-Variable Compromise |
|---|---|---|---|
| Solid Dosage Compaction | High Compression Force (\(F_{\text{comp}} \gt 25\,\text{kN}\)) | Disintegration Kinetics & Pore Network Permeability | Ensuring high tablet mechanical crushing strength (\(\sigma_t \gt 1.5\,\text{MPa}\)) to prevent friability during packaging versus preserving internal porosity for rapid water wicking and target disintegration time (\(\lt 15\,\text{min}\)). |
| Continuous Fluid Bed Drying | High Drying Air Temperature (\(T_{\text{inlet}} \gt 75^\circ\text{C}\)) | Thermolabile API Chemical Degradation & Case Hardening | Accelerating convective moisture removal and throughput versus inducing thermal degradation, ester hydrolysis, or rapid surface crusting that traps residual internal solvent. |
| LNP Microfluidic Formulation | Total Flow Rate (TFR) & High Reynolds Mixing | Channel Hydraulic Backpressure & Pump Cavitation Limits | Achieving ultra-fast chaotic advection mixing (\(\tau_{\text{mix}} \lt 2\,\text{ms}\)) for monodisperse small nanoparticles (\(\text{PDI} \lt 0.1\)) versus operating within microfluidic chip pressure thresholds (\(\Delta P \lt 15\,\text{bar}\)). |
| Biopharmaceutical Lyophilization | Aggressive Primary Drying Shelf Temperature (\(T_{\text{shelf}} \gt -10^\circ\text{C}\)) | Formulation Collapse Temperature (\(T_c / T_g'\)) | Shortening commercial freeze-drying cycle duration (reducing multi-day processing costs) versus avoiding product cake micro-collapse, loss of elegant cake structure, and protein bioactivity loss. |
Interactive Controlled-Release Drug Dissolution Simulator
Adjust polymer matrix erosion rate, drug solubility, and tablet coating thickness to simulate real-time dissolution profile kinetics (Higuchi vs. Zero-Order release) in a USP Dissolution Apparatus.
Mathematical model: Cumulative mass release \(M(t) = 100 \left(1 - e^{-k (t - t_{\text{lag}}) (\text{pH} / 5.0)}\right)\). Online interactive module: https://prep4uni.online/stem/physical-technologies/biomedical-engineering/pharmaceutical-engineering/
Why Study Pharmaceutical Engineering
Designing Drug Manufacturing Processes
Chemical and Biological Formulations
Regulatory and Quality Standards
Process Optimization and Automation
Contribution to Public Health
Pharmaceutical Engineering: Conclusion
Pharmaceutical Engineering is a vital and dynamic field that drives innovation in drug development, manufacturing, and delivery systems. By integrating engineering principles with pharmaceutical sciences, it ensures the safe, efficient, and cost-effective production of high-quality medicines. The field continues to evolve with emerging technologies like continuous manufacturing, nanotechnology, and personalized medicine, shaping the future of global healthcare. Pharmaceutical engineers are at the forefront of addressing challenges in drug production and ensuring access to safe and effective therapies for patients worldwide.
Frequently Asked Questions on Pharmaceutical Engineering
Is pharmaceutical engineering the same as pharmacy?
No. Pharmacy concentrates on the safe use of medicines in clinical practice, including dispensing and patient counselling. Pharmaceutical engineering focuses on how medicines are formulated, manufactured and scaled up, ensuring that each tablet, capsule, injection or biologic product is produced reliably and meets strict quality standards.
Do pharmaceutical engineers work only in big drug companies?
Many do work in large pharmaceutical firms, but there are also roles in biotech start-ups, contract manufacturing organisations, regulatory agencies, consulting firms and equipment or technology suppliers. Their skills are relevant anywhere large-scale production of medicines or related products is needed.
Why is scale-up from lab to factory so difficult?
Conditions that work perfectly in a small beaker may behave very differently in a large reactor or mixer. Heat transfer, mixing patterns and residence times all change with scale, which can alter particle size, purity or crystallisation behaviour. Pharmaceutical engineers must understand these effects and design processes that remain robust at industrial volumes.
How is “quality by design” different from just testing the final product?
Quality by design emphasises understanding how raw materials and process parameters influence the final product, and building quality into the process from the start. Instead of relying mainly on end-point testing, engineers design controlled processes, define acceptable design spaces and use real-time monitoring so that each batch is inherently more consistent.
Are biologic drugs engineered in the same way as traditional tablets?
Not exactly. Biologics such as antibodies are produced in living cells and are much more sensitive to temperature, pH and processing conditions than small-molecule drugs. Pharmaceutical engineering for biologics involves bioreactor design, sterile processing, complex purification steps and careful control of storage and transport conditions.
How does pharmaceutical engineering relate to sustainability and green chemistry?
Pharmaceutical engineers increasingly design processes that use safer solvents, fewer hazardous reagents and more energy-efficient equipment. They also develop continuous manufacturing lines that reduce waste and enable tighter control. These choices help lower the environmental footprint of medicine production while keeping quality and safety as top priorities.
End-of-Page Practice & Assessment Module
Section 1: Foundational Review Questions
Testing core principles, scale-up protocols, and regulatory frameworks. Toggle each box to reveal the answer.- What is pharmaceutical engineering, and what are its primary objectives?
Click to Toggle Answer
Answer: Pharmaceutical engineering is a branch of biomedical and chemical engineering that applies engineering principles to the development and manufacture of pharmaceutical products. Its primary objectives are to design efficient and scalable processes for drug production, ensure consistent product quality and safety, and develop innovative dosage forms and drug delivery systems that meet clinical and patient needs.
- How do pharmaceutical engineers contribute to drug formulation and delivery?
Click to Toggle Answer
Answer: Pharmaceutical engineers optimize drug formulations to improve stability, solubility, efficacy, and patient compliance. They design delivery systems such as controlled-release tablets, injectable suspensions, inhalable powders, transdermal patches, and nanoparticle-based carriers to ensure active ingredients reach target sites at controlled release rates.
- What role does process optimization play in pharmaceutical manufacturing?
Click to Toggle Answer
Answer: Process optimization refines unit operations to increase yield, minimize variability, and lower production costs while maintaining strict quality standards. Engineers utilize Process Analytical Technology (PAT), Quality by Design (QbD), and statistical Design of Experiments (DoE) to establish robust design spaces.
- How is quality control maintained in pharmaceutical manufacturing?
Click to Toggle Answer
Answer: Quality control is enforced through rigorous testing of raw materials, intermediates, and final dosage forms. Standard Operating Procedures (SOPs), validated analytical methods, and real-time PAT sensors ensure every batch complies with established monograph specifications prior to release.
- What are the challenges associated with scaling up pharmaceutical processes from lab to factory?
Click to Toggle Answer
Answer: Scale-up introduces non-linear shifts in fluid mixing dynamics, heat transfer, shear forces, and residence time distributions. These changes can alter API crystallization behavior, particle size distribution, and polymorph stability, requiring careful geometric and kinematic scaling strategies.
- How do regulatory agencies influence pharmaceutical engineering practices?
Click to Toggle Answer
Answer: Regulatory bodies (FDA, EMA, WHO) set mandatory Good Manufacturing Practice (GMP) regulations, documentation rules, and validation guidelines. Engineers design facility cleanrooms, unit operations, and automated controls to satisfy regulatory audits and ensure drug safety.
- What advancements have been made in sustainable pharmaceutical manufacturing?
Click to Toggle Answer
Answer: Integration of green chemistry principles, substitution of toxic organic solvents with aqueous or supercritical systems, solvent recovery, biocatalytic synthesis, and energy-efficient continuous manufacturing lines that decrease waste generation.
- How does computational modeling assist in pharmaceutical process development?
Click to Toggle Answer
Answer: Computational Fluid Dynamics (CFD) and Discrete Element Method (DEM) simulations model fluid mixing, tablet compaction, and drying dynamics in silico, reducing physical trial runs, shortening time-to-market, and optimizing scale-up design.
Section 2: Thought-Provoking & Scenario-Based Questions
Evaluating Quality by Design (QbD), bioprocess trade-offs, and advanced continuous manufacturing architectures. Toggle each box to reveal the answer.- How does the Quality by Design (QbD) framework fundamentally alter traditional end-product testing?
Click to Toggle Answer
Answer: QbD builds quality directly into the manufacturing process by establishing a clear Design Space linking Critical Material Attributes (CMAs) and Critical Process Parameters (CPPs) to Critical Quality Attributes (CQAs), ensuring process stability rather than relying on end-batch destructive testing.
- What operational trade-offs exist when transitioning from batch bioprocessing to continuous perfusion bioreactors for monoclonal antibodies?
Click to Toggle Answer
Answer: Continuous perfusion yields higher volumetric productivity and reduces bioreactor footprint, but requires complex automated cell-retention filters, extended sterile feed operations, higher media consumption, and sophisticated real-time PAT monitoring.
- How do lipid nanoparticles (LNPs) protect mRNA therapeutics from enzymatic degradation in vivo?
Click to Toggle Answer
Answer: LNPs encapsulate vulnerable single-stranded mRNA inside a protective hydrophobic lipid core composed of ionizable lipids, helper phospholipids, cholesterol, and PEGylated lipids, shielding it from extracellular ribonuclease (RNase) cleavage and facilitating endosomal escape.
- Why is continuous hot-melt extrusion (HME) effective for formulating poorly water-soluble BCS Class II drugs?
Click to Toggle Answer
Answer: HME molecularly disperses crystalline drug substances into a molten polymeric carrier matrix under heat and intense twin-screw shear mixing, converting the API into a stable amorphous solid dispersion with significantly enhanced dissolution rates.
- What engineering challenges arise when establishing automated 3D printing of personalized polypills?
Click to Toggle Answer
Answer: Preventing thermal degradation of heat-sensitive APIs during nozzle extrusion, maintaining precise inter-layer bonding without chemical cross-talk between compartmentalized active ingredients, and ensuring rapid non-destructive mass/dose verification post-printing.
- How does continuous crystallization reduce polymorphic impurity formation compared to batch crystallization?
Click to Toggle Answer
Answer: Continuous crystallizers (such as mixed-suspension mixed-product removal systems) maintain uniform supersaturation levels and tight residence time distributions, favoring the kinetic growth of the desired stable polymorph while suppressing metastable phase nucleation.
- What role does process analytical technology (PAT) play in feedback-controlled tablet compression?
Click to Toggle Answer
Answer: Near-Infrared (NIR) or Raman probes measure inline active concentration and granule moisture content prior to compression, while strain gauges monitor compression force in real time, automatically adjusting punch die fill depth to prevent weight and hardness variations.
Section 3: Numerical Problems & Step-by-Step Solutions
Quantitative analysis of drug dissolution kinetics, scale-up power consumption, bioreactor dilution rates, and pill compaction forces. Toggle each box to reveal the full calculation.- Problem 1: Noyes-Whitney Drug Dissolution Rate Calculation
Calculate the initial dissolution rate (\(\mathrm{d}C/\mathrm{d}t\)) in \(\text{mg/(L}\cdot\text{s)}\) of an active drug particle array with total surface area \(A = 2.5\,\text{m}^2\) dissolving in a \(V = 0.90\,\text{L}\) USP dissolution vessel. The drug diffusion coefficient \(D = 6.8 \times 10^{-10}\,\text{m}^2/\text{s}\), diffusion layer thickness \(h = 25\,\mu\text{m}\), saturation solubility \(C_s = 4.0\,\text{mg/mL}\), and current bulk drug concentration \(C = 0.5\,\text{mg/mL}\).Click to Toggle Step-by-Step Solution
Step 1: State the Noyes-Whitney Equation
$$\frac{\mathrm{d}C}{\mathrm{d}t} = \left(\frac{D A}{V h}\right) (C_s - C)$$ Step 2: Convert all parameters to consistent SI base units
$$A = 2.5\,\text{m}^2$$ $$V = 0.90\,\text{L} = 0.00090\,\text{m}^3$$ $$h = 25\,\mu\text{m} = 25 \times 10^{-6}\,\text{m}$$ $$C_s - C = (4.0 - 0.5)\,\text{mg/mL} = 3.5\,\text{mg/mL} = 3500\,\text{mg/L}$$ Step 3: Calculate the lead mass transfer coefficient
$$\frac{D A}{V h} = \frac{(6.8 \times 10^{-10}\,\text{m}^2/\text{s}) \times 2.5\,\text{m}^2}{0.00090\,\text{m}^3 \times 25 \times 10^{-6}\,\text{m}} = \frac{1.70 \times 10^{-9}}{2.25 \times 10^{-8}} = 0.075556\,\text{s}^{-1}$$ Step 4: Compute final concentration rate of change
$$\frac{\mathrm{d}C}{\mathrm{d}t} = 0.075556\,\text{s}^{-1} \times 3500\,\text{mg/L} = \mathbf{264.4\,\text{mg/(L}\cdot\text{s)}}$$ - Problem 2: Bioreactor Dilution Rate & Steady-State Cell Productivity
A continuous pharmaceutical fermenter operates at steady state producing therapeutic insulin. The feed flow rate \(F = 45\,\text{L/h}\), culture volume \(V = 300\,\text{L}\), cell concentration \(X = 12.5\,\text{g/L}\), and substrate concentration \(S = 2.0\,\text{g/L}\). Calculate the dilution rate \(D\) in \(\text{h}^{-1}\), residence time \(\tau\) in hours, and volumetric cell productivity \(P_x\) in \(\text{g/(L}\cdot\text{h)}\).Click to Toggle Step-by-Step Solution
Step 1: Calculate Dilution Rate (\(D\))
$$D = \frac{F}{V} = \frac{45\,\text{L/h}}{300\,\text{L}} = \mathbf{0.15\,\text{h}^{-1}}$$ Step 2: Calculate Mean Residence Time (\(\tau\))
$$\tau = \frac{1}{D} = \frac{1}{0.15\,\text{h}^{-1}} = \mathbf{6.67\,\text{Hours}}$$ Step 3: Calculate Volumetric Cell Productivity (\(P_x\))
$$P_x = D \times X = 0.15\,\text{h}^{-1} \times 12.5\,\text{g/L} = \mathbf{1.875\,\text{g/(L}\cdot\text{h)}}$$ - Problem 3: Power Consumption Scale-Up in Mixing Tanks
A laboratory mixing vessel (diameter \(D_1 = 0.20\,\text{m}\)) operated at speed \(N_1 = 500\,\text{rpm}\) draws power \(P_1 = 15\,\text{Watts}\) in a turbulent fluid regime (constant Power number \(N_p = 5.0\)). Calculate the power required (\(P_2\)) for a geometrically similar industrial vessel scaled up \(5\) times in diameter (\(D_2 = 1.0\,\text{m}\)) if the mixing process is scaled up based on constant tip speed (\(N_1 D_1 = N_2 D_2\)).Click to Toggle Step-by-Step Solution
Step 1: Determine Scaled Impeller Speed \(N_2\)
$$N_2 = N_1 \left(\frac{D_1}{D_2}\right) = 500\,\text{rpm} \times \left(\frac{0.20\,\text{m}}{1.0\,\text{m}}\right) = 100\,\text{rpm}$$ Step 2: Apply the Power Number equation ratio in turbulent regime
$$\text{Power formula: } P = N_p \rho N^3 D^5$$ $$\frac{P_2}{P_1} = \left(\frac{N_2}{N_1}\right)^3 \left(\frac{D_2}{D_1}\right)^5$$ Step 3: Calculate dimensionless scaling ratios
$$\left(\frac{N_2}{N_1}\right)^3 = \left(\frac{100}{500}\right)^3 = (0.2)^3 = 0.008$$ $$\left(\frac{D_2}{D_1}\right)^5 = \left(\frac{1.0}{0.20}\right)^5 = (5)^5 = 3125$$ Step 4: Compute final scaled power \(P_2\)
$$\frac{P_2}{P_1} = 0.008 \times 3125 = 25$$ $$P_2 = 25 \times 15\,\text{W} = \mathbf{375\,\text{Watts}}$$ - Problem 4: Tablet Compaction Tensile Strength
A cylindrical pharmaceutical tablet with diameter \(d = 10.0\,\text{mm}\) and thickness \(t = 4.0\,\text{mm}\) breaks under a radial crushing force \(F = 85\,\text{Newtons}\) in a hardness tester. Calculate the tensile strength \(\sigma_t\) of the tablet in Megapascals (\(\text{MPa}\)).Click to Toggle Step-by-Step Solution
Step 1: Formula for Diametral Tablet Tensile Strength
$$\sigma_t = \frac{2 F}{\pi d t}$$ Step 2: Convert dimensions to standard metric units
$$F = 85\,\text{N}, \quad d = 0.010\,\text{m}, \quad t = 0.004\,\text{m}$$ Step 3: Compute denominator and tensile strength
$$\text{Denominator} = \pi \times 0.010\,\text{m} \times 0.004\,\text{m} = 0.00012566\,\text{m}^2$$ $$\sigma_t = \frac{2 \times 85\,\text{N}}{0.00012566\,\text{m}^2} = \frac{170}{0.00012566} = 1{,}352{,}817\,\text{Pa} = \mathbf{1.35\,\text{MPa}}$$ - Problem 5: Zero-Order vs. First-Order Drug Release Half-Life
An extended-release formulation containing initial drug payload \(Q_0 = 500\,\text{mg}\) releases active ingredient via zero-order kinetics at rate \(k_0 = 25\,\text{mg/h}\). Calculate the zero-order half-life (\(t_{1/2}\)) in hours. If a secondary immediate-release formulation follows first-order kinetics with elimination rate constant \(k_1 = 0.15\,\text{h}^{-1}\), calculate its first-order half-life.Click to Toggle Step-by-Step Solution
Step 1: Zero-Order Half-Life Calculation
$$t_{1/2, \text{zero}} = \frac{Q_0}{2 k_0} = \frac{500\,\text{mg}}{2 \times 25\,\text{mg/h}} = \frac{500}{50} = \mathbf{10.0\,\text{Hours}}$$ Step 2: First-Order Half-Life Calculation
$$t_{1/2, \text{first}} = \frac{\ln(2)}{k_1} = \frac{0.69315}{0.15\,\text{h}^{-1}} = \mathbf{4.62\,\text{Hours}}$$ - Problem 6: Freeze-Drying (Lyophilization) Sublimation Energy Requirement
A batch of \(5{,}000\) vials containing monoclonal antibody solution requires sublimating \(2.0\,\text{mL}\) (\(2.0\,\text{grams}\)) of frozen ice water per vial during primary drying. If the latent heat of sublimation for ice is \(L_{\text{sub}} = 2830\,\text{J/g}\), calculate the total thermal energy in Megajoules (\(\text{MJ}\)) that must be supplied by the lyophilizer heating shelves.Click to Toggle Step-by-Step Solution
Step 1: Calculate total mass of ice to sublimate
$$\text{Total Mass} = 5000\,\text{vials} \times 2.0\,\text{g/vial} = 10{,}000\,\text{g} = 10.0\,\text{kg}$$ Step 2: Calculate Total Energy (\(Q\))
$$Q = m L_{\text{sub}} = 10{,}000\,\text{g} \times 2830\,\text{J/g} = 28{,}300{,}000\,\text{Joules}$$ Step 3: Convert to Megajoules
$$Q = \frac{28{,}300{,}000\,\text{J}}{1{,}000{,}000} = \mathbf{28.3\,\text{MJ}}$$ - Problem 7: First-Pass Sterilization Thermal Death Time (D-Value Calculation)
An autoclave cycle at \(121^\circ\text{C}\) reduces a bacterial endospore population (Geobacillus stearothermophilus) from an initial bioburden \(N_0 = 1.0 \times 10^6\,\text{spores}\) down to \(N = 1\,\text{spore}\) in \(12.0\,\text{minutes}\). Calculate the D-value (decimal reduction time) at \(121^\circ\text{C}\) in minutes.Click to Toggle Step-by-Step Solution
Step 1: State the Formula for D-value
$$D = \frac{t}{\log_{10}(N_0) - \log_{10}(N)}$$ Step 2: Calculate logarithmic microbial reduction
$$\log_{10}(N_0) = \log_{10}(10^6) = 6$$ $$\log_{10}(N) = \log_{10}(1) = 0$$ $$\text{Log Reductions} = 6 - 0 = 6\,\text{decades}$$ Step 3: Compute D-value
$$D_{121} = \frac{12.0\,\text{min}}{6} = \mathbf{2.0\,\text{Minutes}}$$